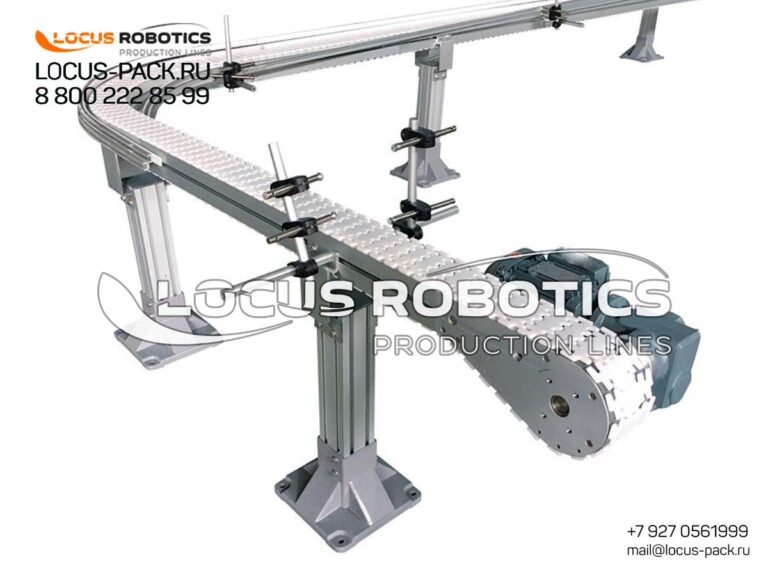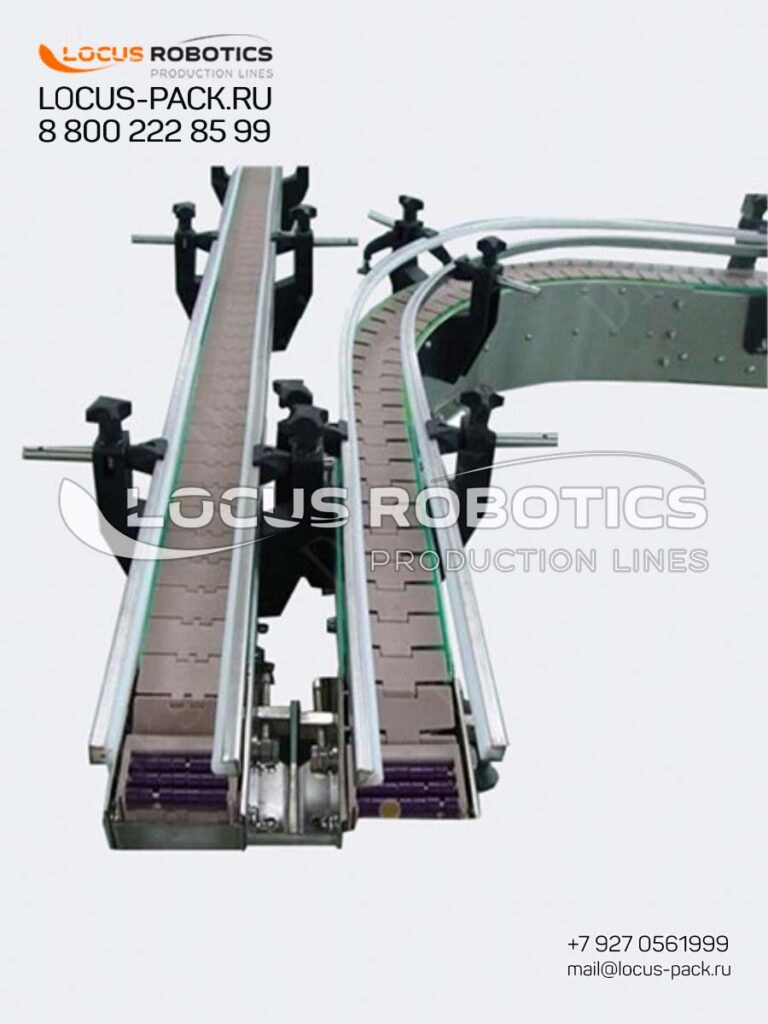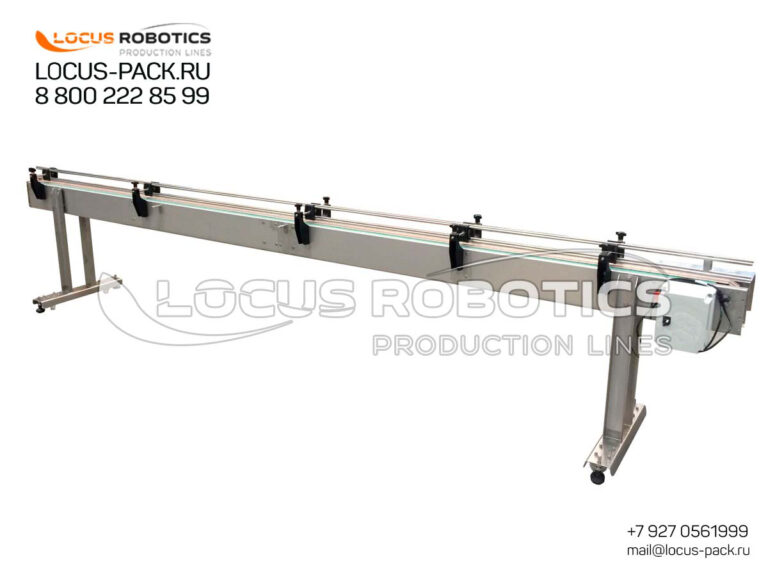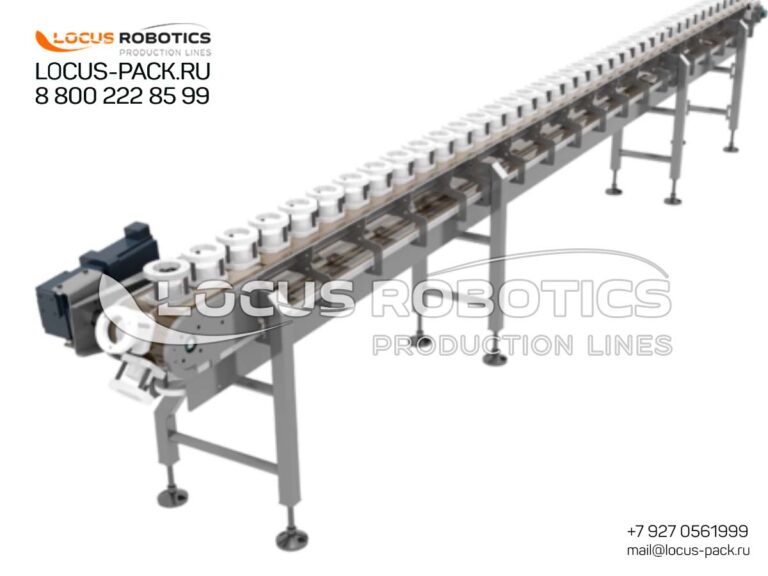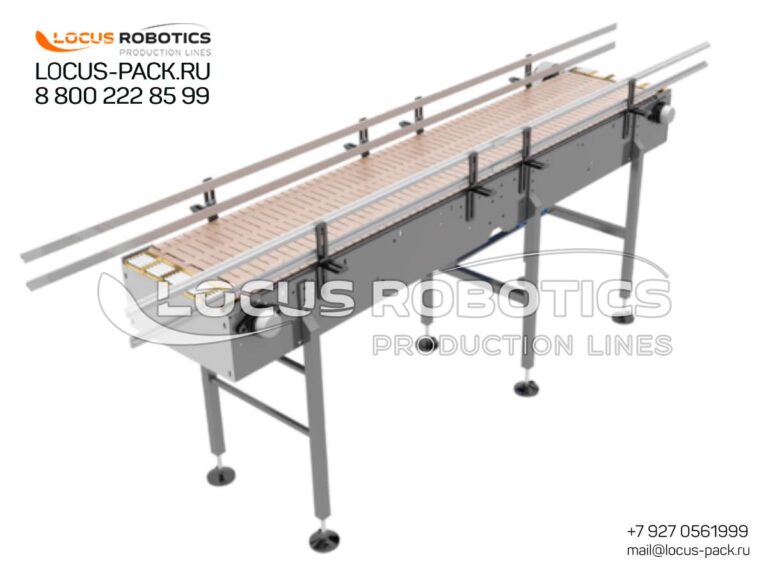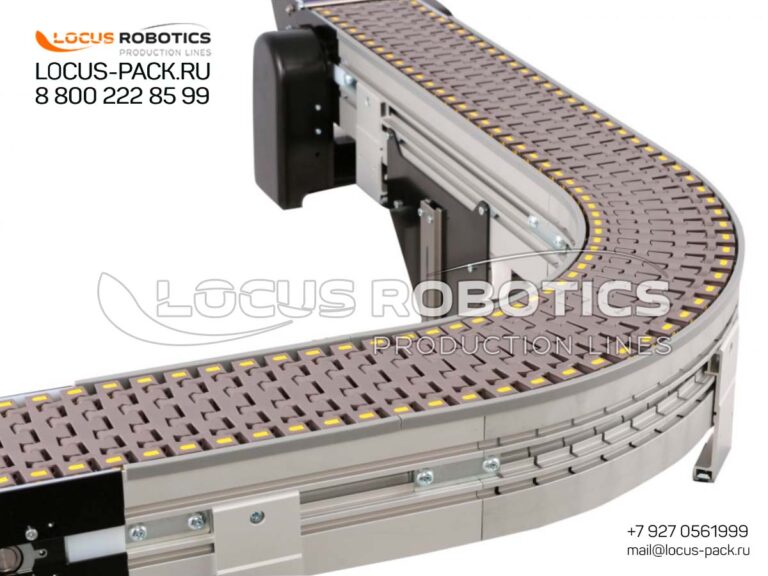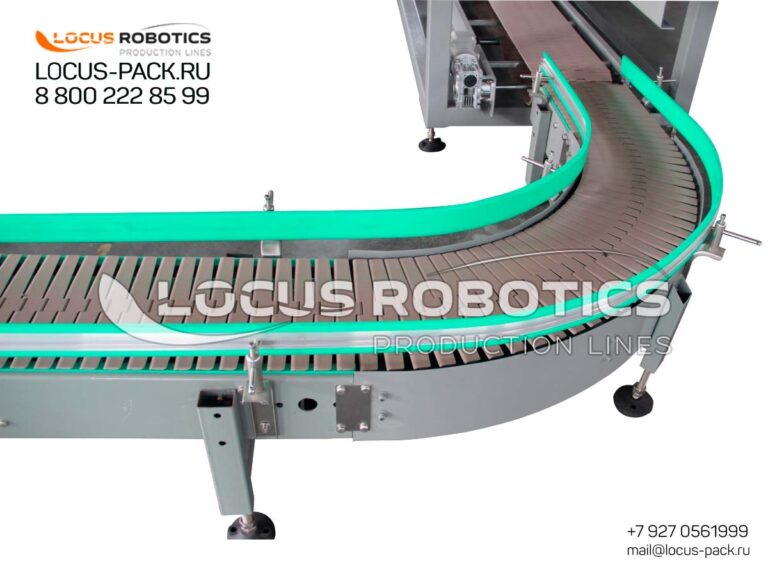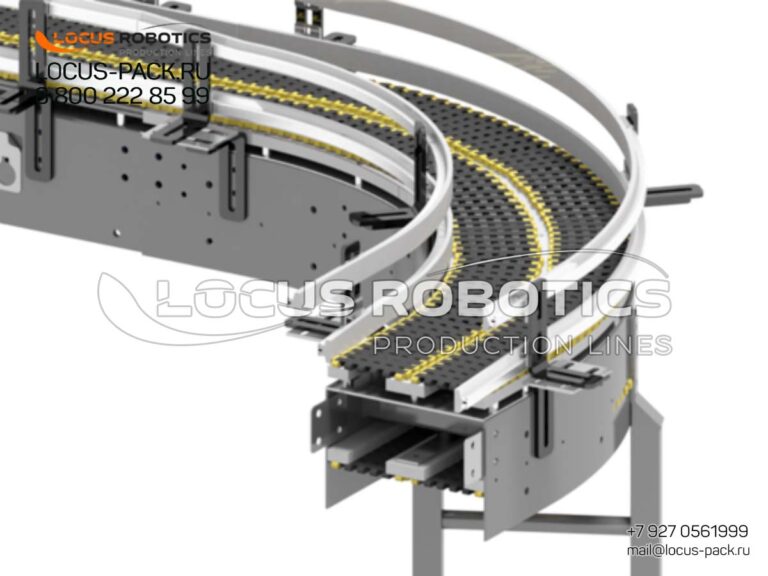
Industrial Modular Belt Conveyor Systems from plastic & SS chain
Chemical-Resistant Solutions • Pharma-Grade Designs.
Industry-leading plastic modular conveyors engineered for:
✅ Filling Monoblocks — Bottling lines, viscous product dosing
✅ Tri-block Systems — Rinse-fill-cap integration
✅ Packaging Automation — Vertical/horizontal form-fill-seal, inspection machines
✅ Harsh Environments — Chemical, pharmaceutical, and food processing
Industry-leading plastic chain conveyors featuring:
✅ Interlocking Modules — Polypropylene, POM acetal, or polyethylene belts
✅ Sanitary Design — No crevices, FDA/EC1935-compliant materials
✅ High-Temp Resistance — Up to 140°C (284°F) for CIP/SIP processes
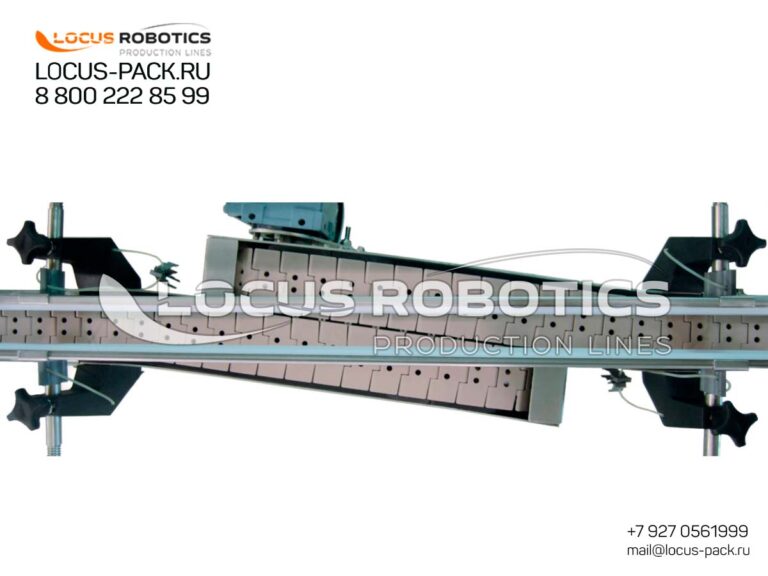
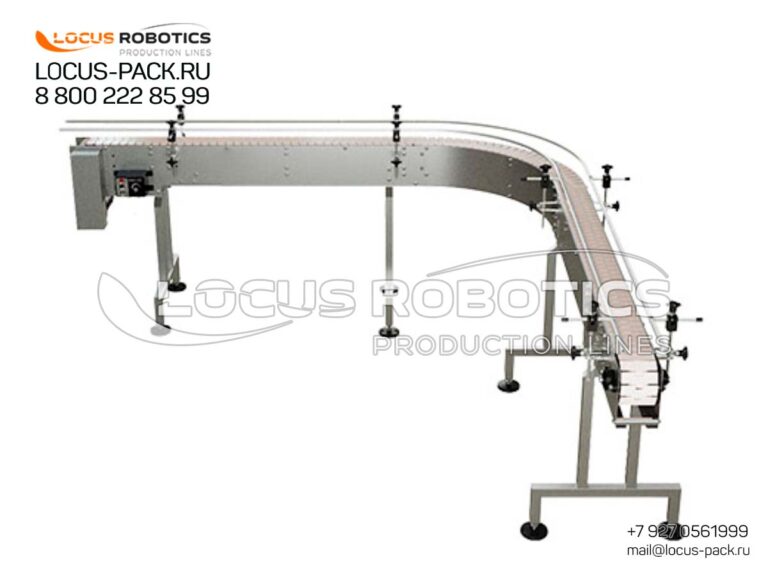
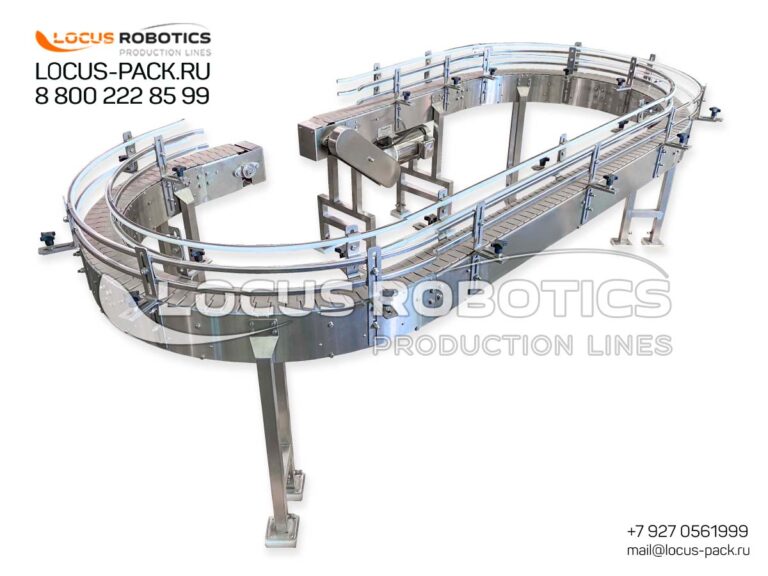
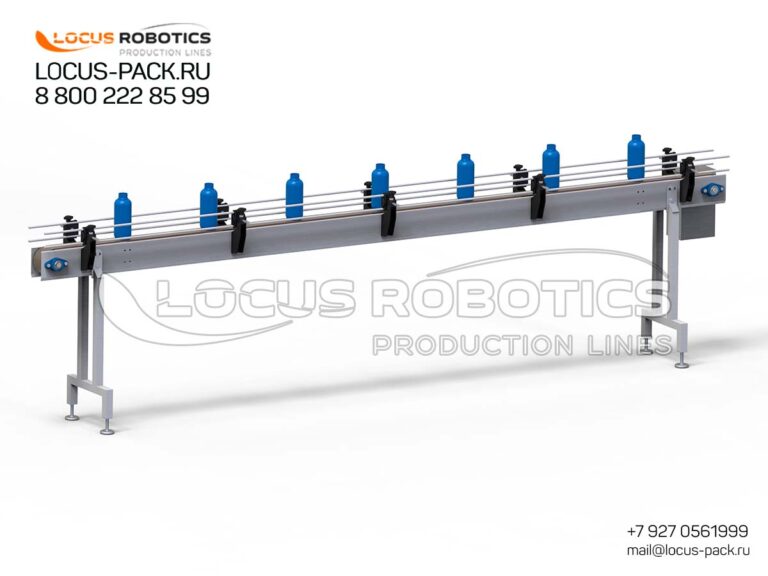
✅ Custom Configurations — Straight, curved, inclined (0-25°), multi-level
| Parameter | Options | Industry-Specific Features |
|---|---|---|
| Belt Material | 316L SS • POM Acetal • PEEK • Polypropylene | Acid-resistant coatings for chemicals • FDA-grade polymers for food |
| Belt Width | 56-220mm (customizable) | Narrow: vials/cosmetics • Wide: IBC totes |
| Frame Construction | Stainless steel • Reinforced polymer | Explosion-proof (ATEX/IECEx) options |
| Configuration | Straight • Curved • Serpentine • Multi-lane • Loop | Tension-compensating sections • Zoned drive systems |
Technical Specifications & Industry Applications.
| Parameter | Standard | Chemical Grade | Pharma Grade |
|---|---|---|---|
| Belt Material | PP | PBT + PTFE | PEEK |
| Chain Pitch | 38.1mm | 50.8mm | 25.4mm |
| Load Capacity | 80 kg/m | 120 kg/m | 60 kg/m |
| Temperature Range | -10°C to 90°C | -20°C to 140°C | -40°C to 180°C |
| Certifications | FDA | ATEX Zone 2 | GMP Annex 1 |
Flammable Liquids Line
ATEX-certified motors • Static-dissipative belts • Nitrogen purging ports
High-Pigment Products
Integrated CIP spray bars • Quick-release belt systems • Anti-stick surfaces
Pharma/GMP Applications
Cleanroom-compatible (ISO 14644) • Validation documentation • Particle-free operation
Food Processing
Jam/paste lines: Anti-stick surface treatments
Sauce fillers: Drainage channels for spill management
Frozen goods: Low-temp flexibility additives
Chemical Manufacturing
Acid-resistant chains (PBT + PTFE coating)
Explosion-proof drives (ATEX-certified)
Secondary containment trays
Pharmaceuticals
Validation documentation packages
Cleanroom-compatible (ISO Class 5-7)
Particle-free operation
| Sector | Use Cases | Critical Features |
|---|---|---|
| Chemicals | Paint • Solvents • Automotive fluids | Explosion safety • Polymer-compatible materials |
| Food & Beverage | Sauces • Jams • Toppings | USDA-compliant design • Drainage channels |
| Pharmaceuticals | Vials • Syringes • Medical devices | GMP validation • Change-part documentation |
✓ Seamless CIP — Fully submersible with in-place cleaning
✓ Zero Contamination — Electropolished stainless steel frames
✓ Quick-Change — Tool-free belt replacement <20 min
✓ Smart Monitoring — IoT-ready wear sensors (optional)
✓ Zero product carryover — Seamless belt modules
✓ Rapid changeovers — Tool-free belt replacement (<15 min)
✓ Smart monitoring — IoT-ready wear sensors (OEE tracking)
✓ Global compliance — CE, ATEX, FDA, EHEDG, GMP
Filling monoblocks
Rinse-Fill-Cap tri-blocks
Linear fillers • Capping machines
Labelers • Inspection systems
Vertical/horizontal packaging machines
Doypack® pouching equipment
Proven in Harsh Environments
Salt brine lines (pickle production)
Bleach filling stations
Sticky topping applications
Custom Engineering
Zoned heating/cooling modules
Magnetic bead chains for metal detection
Vacuum hold-down systems
GMP-Compliant Material Handling for Food, Chemical & Pharma Applications.
Precision Material Handling Solutions for Filling, Capping & Packaging Lines.
Need conveyors for explosive atmospheres or high-purity applications?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
Free line configuration for your products, throughput validation testing!
Contact Specialists for Packaging Equipment:
Compliance Roadmap: