Your Chemical Formulation Demands More Than a Standard Machine. It Demands Engineered Safety and Precision.
Chemical manufacturing—from everyday household cleaners and premium automotive polishes to industrial solvents, agricultural pesticides, and construction materials—presents a unique set of challenges that standard packaging equipment cannot solve. Safety is non-negotiable. Product integrity is paramount. The risks associated with aggressive pH levels, flammability (LFL), foaming, or high viscosity require a partner who understands materials science, explosion-proof (EX) design, and specialized handling protocols.
LOCUS Robotics is that partner. We provide true turnkey engineering and integration services for chemical production facilities. We do not sell generic «business-in-a-box» franchises; we deliver a professional, performance-guaranteed partnership. Our mission is twofold: first, to equip your facility with the optimal selection of specialized technology, and second, to ensure its flawless commissioning and ramp-up to your target production volumes.
With extensive experience serving everything from agile startups to leading national producers across Russia, we understand the spectrum of needs. We engineer solutions that are fundamentally safe, reliable, and tailored to the specific behavior of your product. Whether you are filling foaming car shampoos, corrosive acids, viscous sealants, or flammable solvents, we integrate the precise material compatibility, safety features, and process controls you need to operate with confidence and efficiency. Let’s build a production line that respects the science of your chemistry.
The Three Pillars of Chemical Line Engineering: Safety, Compatibility, and Precision
While chemical production may have different aesthetic requirements than cosmetics or food, its technical demands are often more rigorous. We engineer systems around three non-negotiable pillars.
Ultimate Safety for Personnel and Facility Handling flammable liquids (LFLs), solvents, or volatile compounds requires an engineering-first approach to hazard prevention.
Explosion-Proof (EX) Design: We design and integrate equipment with ATEX/EX-rated components—including motors, sensors, control panels, and lighting—for use in potentially explosive atmospheres. This includes pressurized enclosures (purge systems) and intrinsic safety barriers.
Vapor Containment & Ventilation: Systems can be integrated with local exhaust ventilation (LEV) and vapor recovery units to capture harmful fumes at the filling point.
Process Safety Controls: Interlocks, emergency stop circuits, and leak detection systems are standard to mitigate operational risks.
Advanced Material Compatibility for Product Integrity Aggressive chemicals demand specialized wetted materials to prevent contamination and equipment failure.
Corrosion-Resistant Materials: For acids, alkalis, and oxidizers, we construct product contact parts from high-performance polymers (PTFE, PVDF), specialty alloys (Hastelloy), or ceramic-coated stainless steel. This ensures long-term equipment life and prevents metallic contamination.
Inert Material Selection: We specify seals and gaskets (e.g., EPDM, FKM/Viton) that are chemically inert to your specific formulation, preventing swelling, degradation, and product adulteration.
Precision Handling for Difficult Product Behaviors Chemical products are not uniform. We apply targeted technologies to manage their physical characteristics.
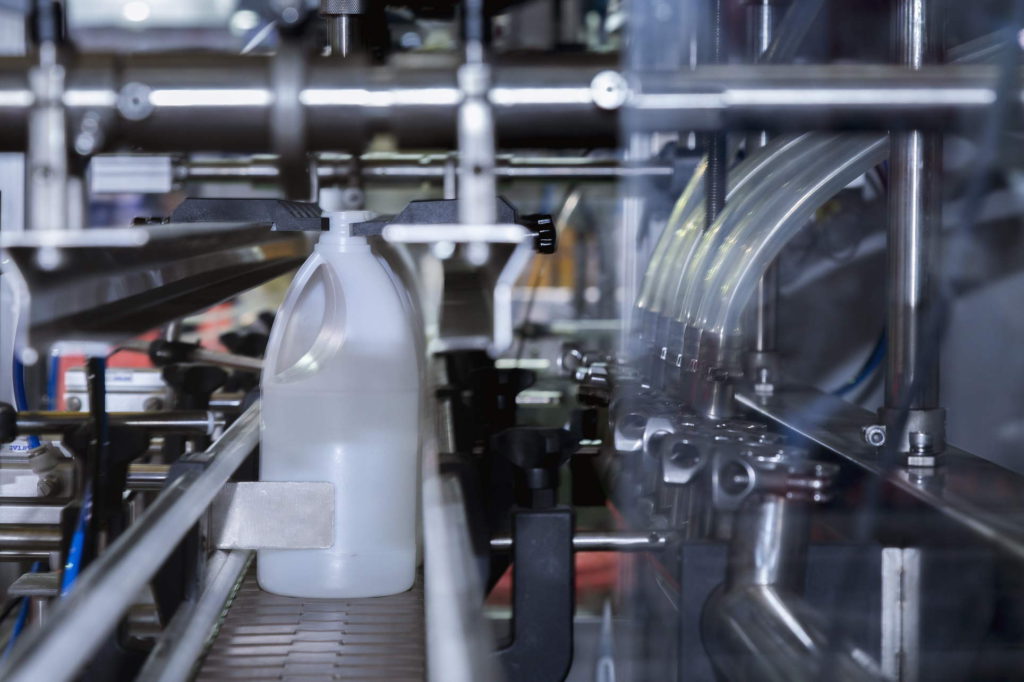
Foam Management: For shampoos, detergents, and foam cleaners, we implement bottom-up fill systems, «no-drip» snuff-back valves, and intelligent filling programs that minimize shear and air entrapment.
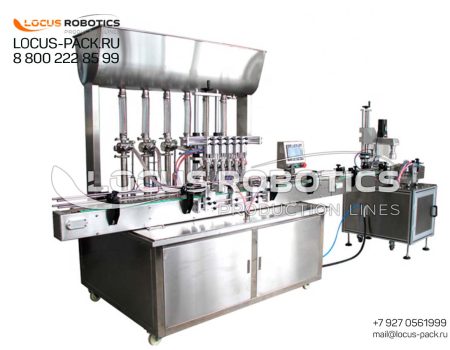
High-Viscosity Dosing: For sealants, pastes, and thick adhesives, we use piston fillers with scraped-surface hoppers and positive displacement pumps that handle viscous products without separation or cavitation.
Abrasive Slurry Handling: For products with suspended solids, we select wear-resistant components and valves designed to minimize abrasion and clogging.
Scalable Solutions Aligned with Your Production Strategy
We match technology to your output goals and operational flexibility needs.
Small-Batch & Pilot Production (< 8,000 units/shift) Ideal for R&D, limited editions, gift sets, or multi-SKU contract manufacturers.
Scenario: You need to produce small runs of various products (e.g., a new car wax, a pilot batch of industrial cleaner) or use different container types for specialty lines.
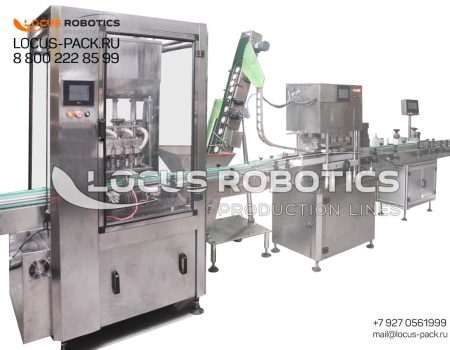
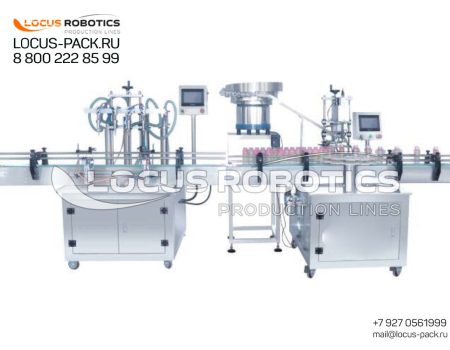
Our Solution:Modular Semi-Automatic Workstations. These include table-top or floor-standing fillers, cappers, and labelers. They offer maximum flexibility for frequent product changeovers, require lower initial investment, and are perfect for handling aggressive chemicals in a controlled, small-scale environment.
Key Benefit: Unmatched agility for product development and niche production with minimal downtime between runs.
High-Volume Serial Production (8,000+ units/shift) Designed for established brands with core products requiring reliable, efficient output.
Scenario: You have a bestselling product (e.g., a 1L glass cleaner) that requires consistent, high-volume packaging across multiple shifts.
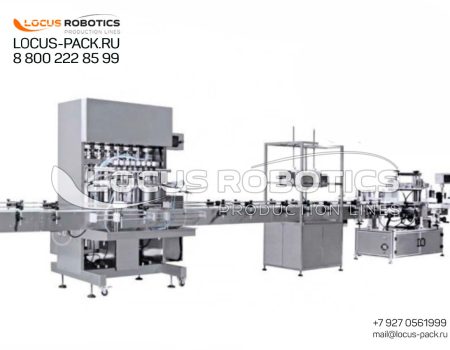
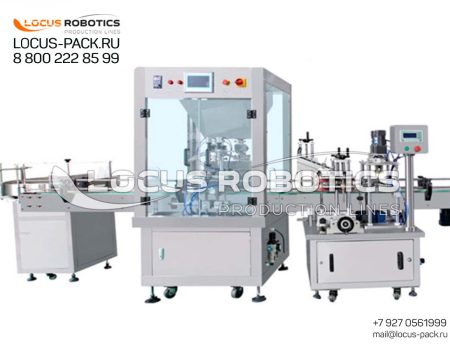
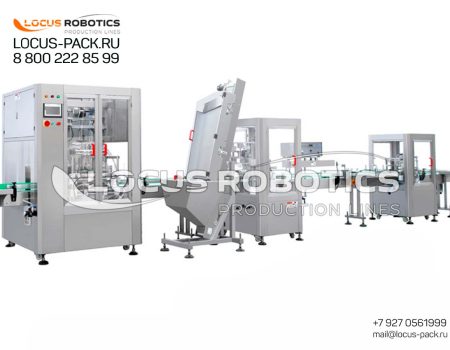
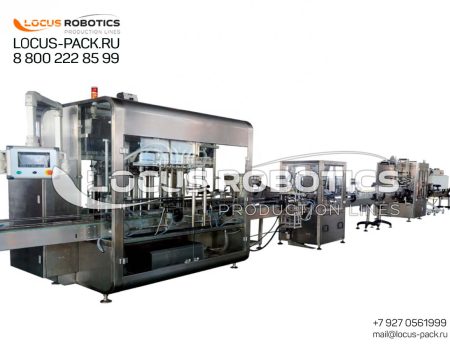
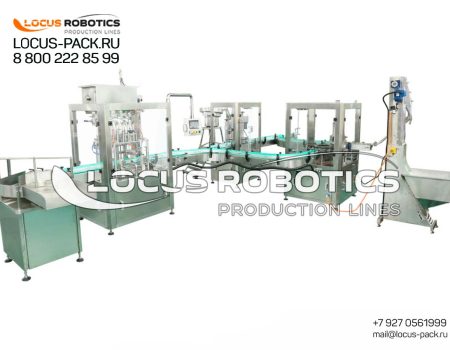
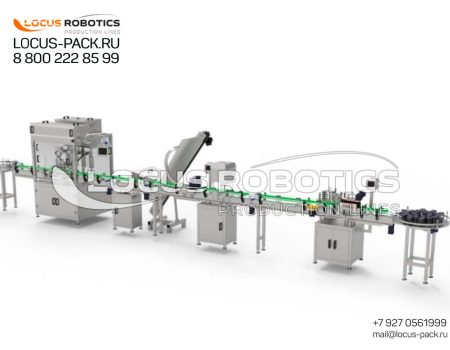
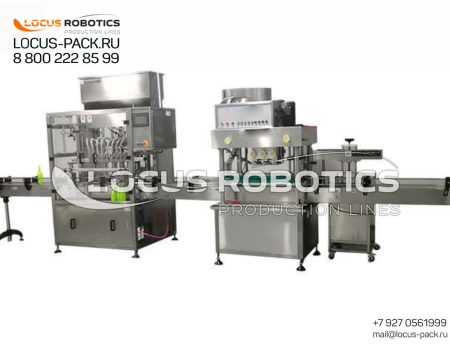
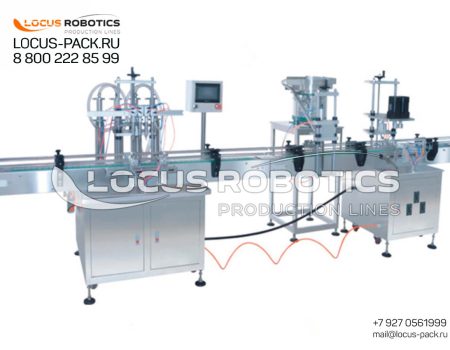
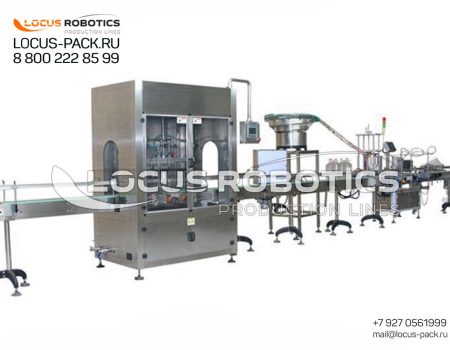
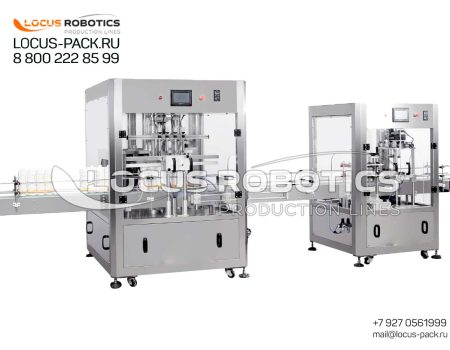
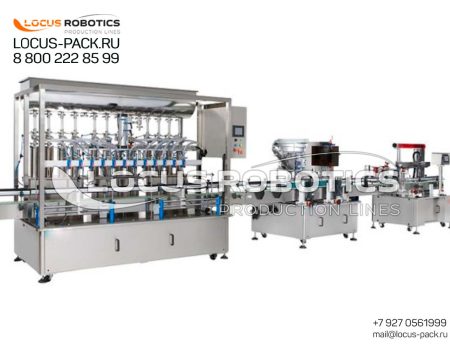
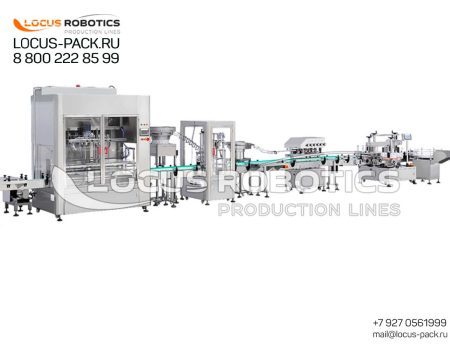
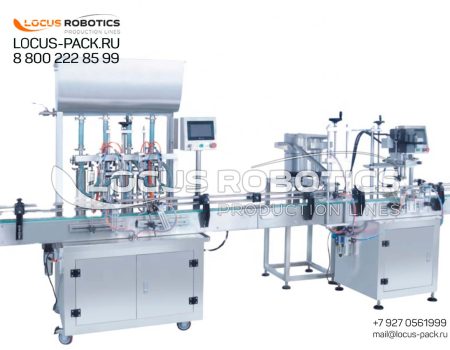
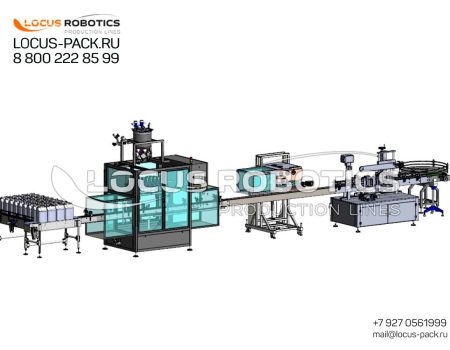
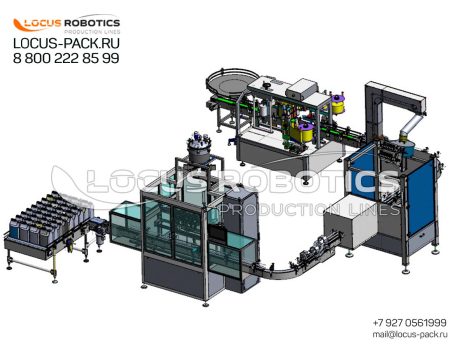
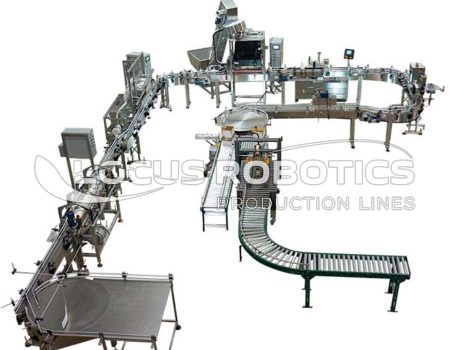
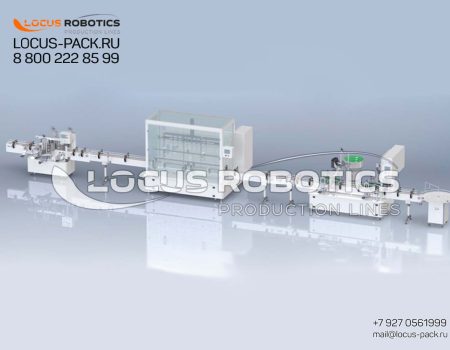
Our Solution:Automated Linear (Inline) Lines or Rotary Monoblocks. These synchronized systems provide continuous flow filling, capping, and labeling. They are engineered with the necessary safety and material specifications (EX, polymers) for your product and are built for high throughput with robust reliability.
Key Benefit: Optimized labor efficiency, consistent output quality, and the lowest cost-per-unit for high-volume SKUs, all within a safety-engineered framework.
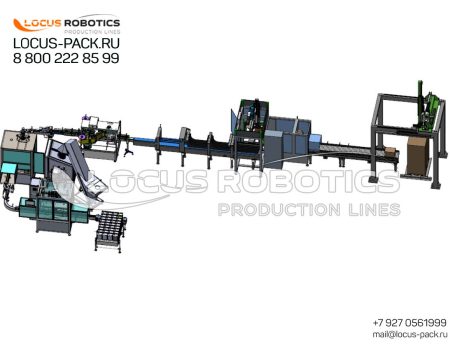
A Complete Supply Chain from Mixing to Palletizing
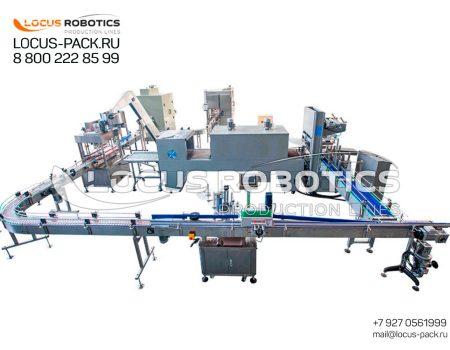
We provide and integrate the entire production line tailored for chemical manufacturing:
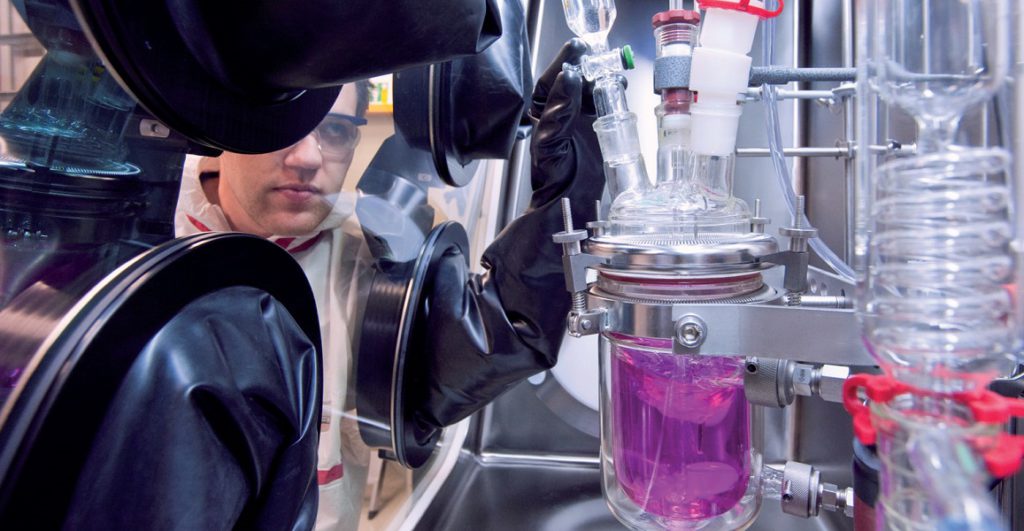
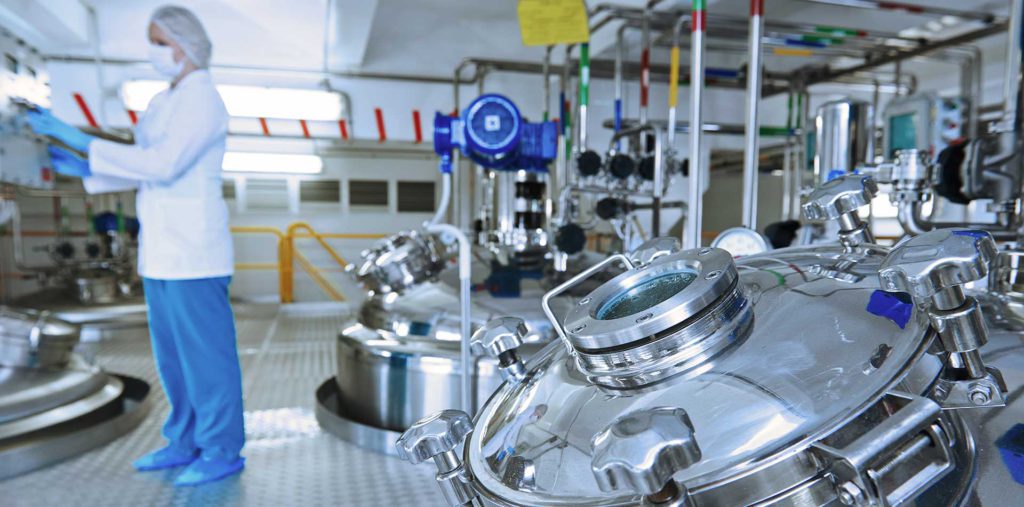
Preparation & Synthesis:Reactors, mixing tanks, dissolvers, turbo-emulsifiers, and preparation vessels for compounding raw materials.
Bulk Storage & Transfer:Eurocubes with specialized process skids and product transfer systems.
Specialized Primary Packaging:
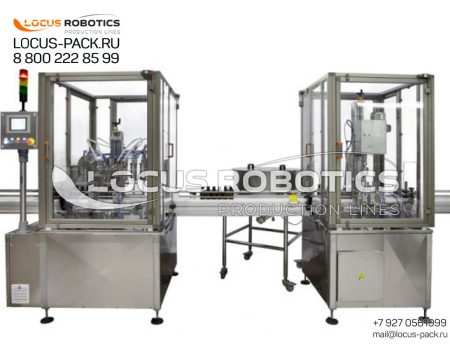
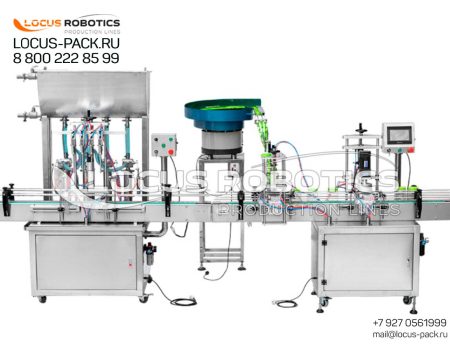
Liquid Fillers: From semi-automatic dosers to automatic linear and rotary fillers, configured for your product’s behavior.
Cappers: Semi-automatic and automatic capping machines for a wide range of closures (screw caps, flip-tops, plugs).
Sealers:Induction sealers for tamper-evidence on plastic containers, thermal sealers for flexible pouches.
Labeling & Coding:Semi-automatic and automatic labelers for precise application on various container shapes.
Secondary & Tertiary Packaging:Vertical/horizontal cartoners, multi-packing machines, and palletizing solutions.
Why Partner with a Specialist, Not a Franchise Seller?
Our model is built on engineering integrity and shared success, not just equipment sales.
Performance Guarantee Focus: We are contractually committed to your line’s output and efficiency targets, not just its delivery.
Deep Chemical Sector Expertise: Our team understands the regulatory, safety, and technical nuances of household, automotive, agro-, and industrial chemical production.
No «Black Box» Solutions: We provide full transparency in design, material selection, and costing. You own the process and the knowledge.
Ready to Engineer a Safer, More Efficient Chemical Packaging Line? Begin a technical discussion with our chemical industry specialists today.