Preserving Freshness, Taste, and Nutrition from Farm to Consumer

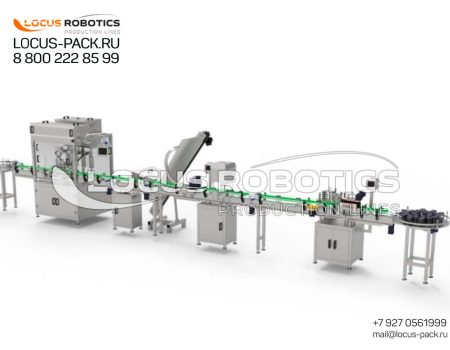
The dairy industry is defined by its commitment to delivering safe, nutritious, and sensorially perfect products with ever-shorter shelf life expectations. At LocusPack, we provide the integrated processing and precision packaging technology essential for success in this demanding sector. Our expertise covers the entire value chain—from the receiving and standardization of raw milk to the gentle, hygienic packaging of the most sensitive UHT creams, probiotic yogurts, cultured cheeses, and nutritional dairy powders. We engineer solutions that master the critical challenges of dairy: preventing post-pasteurization contamination, managing products of varying viscosity and fat content, and ensuring rapid, clean changeovers between different product types and packaging formats. For producers in growth markets across Asia, Africa, and the Americas, our robust, efficient lines are the key to scaling production, ensuring compliance with HACCP and local dairy standards, and building a brand synonymous with consistent quality and safety.

I. Aseptic & ESL (Extended Shelf Life) Liquid Packaging

For low-acid, nutrient-rich dairy products, microbial control is non-negotiable. Our technologies ensure sterility or exceptional hygiene to achieve ambient or extended chilled shelf life.

  • High-Speed Aseptic Brick Carton Packaging: The global standard for UHT milk, cream, and dairy drinks. We integrate form-fill-seal (FFS) machines that sterilize the packaging material (using hydrogen peroxide bath and heat), form it into a tube under sterile conditions, fill it with the UHT-treated product, and seal it. These systems achieve outputs over 9,000 cartons per hour and are the most efficient solution for large-volume, ambient-stable liquid dairy. Capabilities include adding straws, screw caps, or reclosable fitments for enhanced convenience.

  • Aseptic & ESL Bottle Filling for Premium Dairy: For products like UHT flavored milk, lactose-free milk, and cream liqueurs in PET or HDPE bottles. Our aseptic bottle fillers sterilize pre-formed bottles and caps (via H₂O₂ spray/vapor, PAA, or UV-C light), then fill in a sterile, positive-pressure chamber. For high-quality fresh milk targeting 30-60 day chilled shelf life, ESL (Extended Shelf Life) fillers use ultra-clean technology—micro-filtered air over the critical zone, CIP/SIP filler bowls, and sterile air flushing—to drastically reduce recontamination, outperforming standard clean-fill systems.

  • Hot-Fill Technology for Dairy-Based Desserts & Drinks: For products with higher acidity or sugar content, like drinking yogurts, dairy smoothies, and puddings, hot-fill is highly effective. Products are filled at 85-92°C into heat-resistant PET or glass. The hot product sanitizes the container interior, and the subsequent cooling creates a vacuum, ensuring stability. Our systems are designed to handle the viscosity and particulates in these products without clogging.
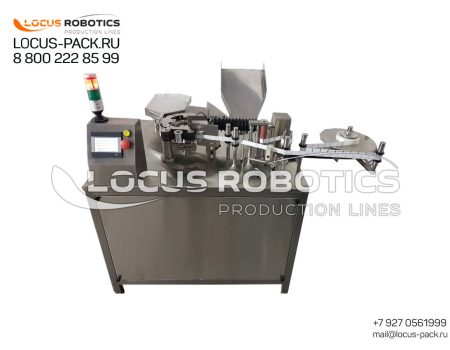
Dairy Industry Packaging & Processing Solutions

II. Processing & Packaging for Viscous & Cultured Products

Yogurt, sour cream, dairy desserts, and cream cheese present unique challenges due to their viscosity, delicate textures, and live cultures.

Dairy Industry Packaging & Processing Solutions
  • Precision Filling for Set & Stirred Yogurt: We offer distinct solutions for both types. For set yogurt, our piston fillers deposit a precise volume of inoculated mix directly into the final cup, which is then lidded and sent to incubation tanks. For stirred yogurt, gentle rotary piston fillers are used to transfer the coagulated product from a fermentation tank to cups or tubs. Key features include wide-diameter cylinders, low-shear valves, and fruit inclusion systems that can inject jam or fruit puree either in the center or swirl it through the product.

  • Cream Cheese, Quark & Dairy Spread Packaging: These high-viscosity, often sticky products require robust positive-displacement technology. Our piston fillers and specialized lobe pump systems accurately portion product into plastic tubs, foil containers, or even laminated tubes. They are paired with level-smoothing devices to create a perfectly flat product surface before lidding, which is crucial for brand presentation. For whipped products, we can integrate continuous aeration (mondomix) systems.

  • Integrated Fermentation & Processing Skids: We can supply complete fermentation tanks with integrated plate heat exchangers for cooling, and buffer tanks with gentle agitators. This allows for a seamless, closed process from inoculation and incubation through to cooling, fruit mixing, and final packaging, maximizing hygiene and process control.

III. Cheese & Powder Packaging Systems

From hard cheese blocks to dairy powders, dry and semi-dry products need robust, often gas-flushed packaging to prevent spoilage.

  • Modified Atmosphere Packaging (MAP) for Cheese: To extend shelf life and prevent mold, cheese requires oxygen-free packaging. Our horizontal flow-wrapper and chamber vacuum machines are ideal for block, sliced, and shredded cheese. They evacuate air from the package and back-flush with a protective gas mix (typically CO₂ and N₂) before sealing. For premium shredded cheese, we integrate weigh-price-labeling systems that fill by weight into pre-made pouches and apply a retail-ready label in one step.

  • Aging & Brining Systems for Cheese Production: For the production of semi-hard and hard cheeses, we provide cheese vats for curd processing, molding presses, and automated brining systems. These systems ensure consistent cheese geometry, controlled salt uptake, and efficient handling of heavy blocks, forming a complete solution for artisanal and industrial cheese makers.

  • Powder Filling for Milk & Whey Powder: The packaging of hygroscopic and dusty dairy powders demands precision and excellent containment. Our solutions include auger fillers with anti-bridging hoppers and deaeration systems for light powders, and gravimetric weigh-fillers for high-accuracy bagging. These are integrated with dust extraction hoods and can feed valve sacks, lined boxes, or composite cans. For infant formula, we can provide nitrogen gas flushing before sealing to prevent oxidation.
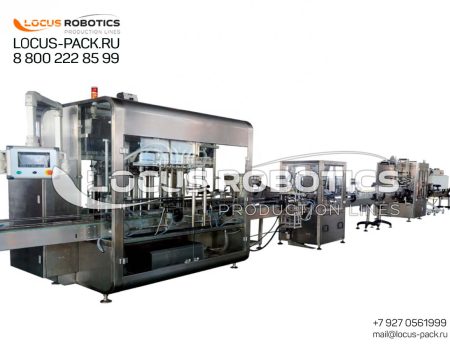
Dairy Industry Packaging & Processing Solutions

IV. Critical Support Systems: Homogenization, CIP & Process Control

The supporting technology is what transforms a filling line into a reliable, hygienic dairy plant.

Dairy Industry Packaging & Processing Solutions
  • High-Pressure Homogenization & Emulsification: Essential for stabilizing milk fat globules, preventing cream-line separation, and creating stable emulsions for cream and dessert products. We supply high-pressure homogenizers (up to 250 bar) that can be configured in single or two-stage setups. Integration with UHT plants is standard, ensuring a continuous, sterile process from treatment to packaging.
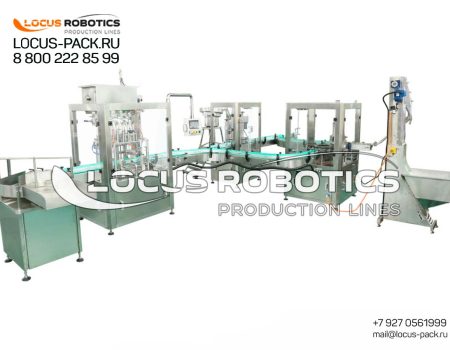
  • Sophisticated Clean-In-Place (CIP) Systems: The lifeblood of any dairy plant. We design and install multi-circuit, fully automated CIP systems. These systems control the circulation of water, caustic, acid, and sanitizer through all product contact piping, tanks, and filler bowls. Our designs feature turbulent flow for cleaning, recovery of chemicals and final rinse water, and data logging to provide validation records for every cleaning cycle.
  • Process Automation & Data Management: Modern dairy plants run on data. We integrate SCADA systems that provide a central overview of the entire process—from raw milk intake temperatures and pasteurization parameters to filler speeds and CIP cycle status. This enables real-time monitoring, recipe management, and comprehensive traceability reporting for quality assurance and regulatory compliance.

V. The LocusPack Total Solution for Dairy

We partner with dairy producers to build operational excellence, from greenfield projects to line expansions.

  1. Hygienic Engineering by Default: All our equipment is designed to EHEDG and 3-A Sanitary Standards. This means fully polished welds, self-draining slopes, cleanable frames, and hygienic fittings. This design drastically reduces bacterial harborage points, simplifies cleaning, and is fundamental to producing safe dairy products.

  2. Product & Format Flexibility: We engineer lines to handle a wide product portfolio. A single line can often be configured to run UHT whole milk, ESL skimmed milk, and flavored drinking yogurt by changing recipes and utilizing quick-change parts for fill volumes and container types (e.g., switching between 1L gable-top cartons and 500ml bottles).

  3. Lifecycle Efficiency & Sustainability: Our focus extends to reducing your total cost of ownership. We specify energy-efficient homogenizers and pumps, CIP systems that minimize water and chemical use, and high-yield fillers that reduce product giveaway. This improves both your profitability and environmental footprint.

  4. Comprehensive Project Execution: We manage the entire project: process design, equipment selection, factory testing, installation, commissioning, and validation support (IQ/OQ). We ensure your team is fully trained on operation, maintenance, and sanitation procedures, providing a smooth transition to full production.

Dairy Industry Packaging & Processing Solutions

Ready to build or upgrade a world-class dairy processing and packaging facility?

Contact the LocusPack dairy specialists today. Let’s discuss how our integrated technology and engineering expertise can help you produce safer, higher-quality dairy products with greater efficiency and flexibility.

Contact Our Team

Dairy Industry Packaging & Processing Solutions