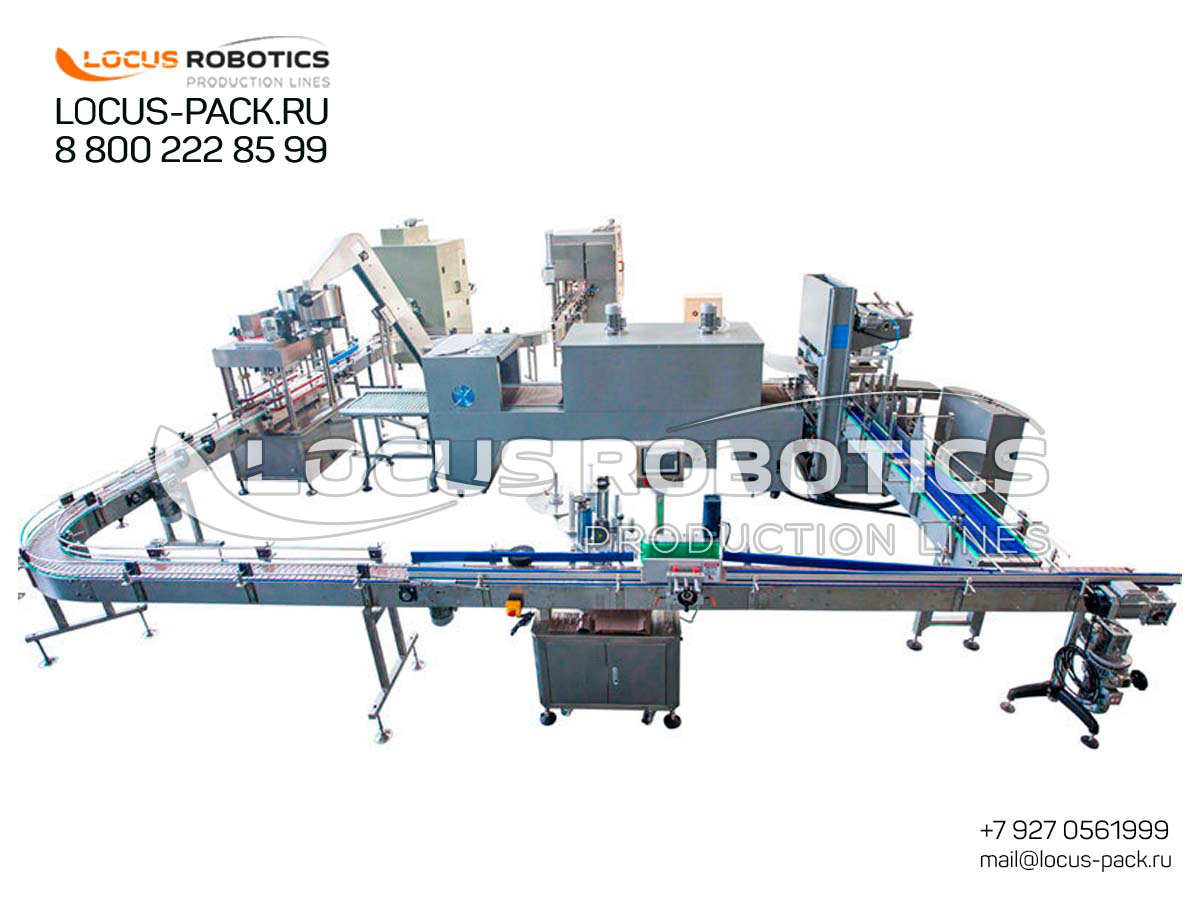
Description
High-Flexibility, Dual-Stream System for Diverse Chemical and Industrial Product Lines
Independent Dual Filling Blocks for Simultaneous or Separate Product Runs.
Automated Group Packaging Unit for Multipacks, Trays, and Bundles.
Centralized Control System with Multi-Language HMI.
The R-400 represents a paradigm shift in versatile production line design. It solves a critical bottleneck for modern manufacturers: the need to package diverse product portfolios with different chemical properties without costly line changeovers or dedicated machinery. This system is conceived as a «factory within a factory,» featuring two fully independent, parallel filling circuits. This architecture allows one side of the line to be dedicated to corrosive or solvent-based products constructed with specialized, chemically resistant valves and piping, while the other side handles water-based or food-grade products. A centralized intelligent conveyor system manages the flow of different container types to their respective fillers and then merges them for downstream group packaging. This dual-stream capability is a game-changer for operational efficiency, enabling producers in Southeast Asia, Africa, and the MENA region to serve varied market segments—from automotive chemicals and industrial solvents to household cleaners and food oils—with unparalleled agility and minimized downtime.
System Architecture: Dual Filling Capability and Automated Secondary Packaging
1. Independent Dual Filling Blocks for Simultaneous or Separate Product Runs: The core innovation lies in the two autonomous filling monoblocks. Each block can be configured with different filling technologies—such as piston fillers for viscous pastes, pump fillers for solvents, or gravity fillers for free-flowing liquids—suited to the product’s specific viscosity, foaming tendency, and aggressiveness. They operate from separate product supply tanks and CIP circuits, ensuring absolute cross-contamination prevention. This allows a plant to run a batch of windshield washer fluid on one line and a batch of engine degreaser on the other simultaneously, doubling effective output.
2. Automated Group Packaging Unit for Multipacks, Trays, and Bundles: After capping, bottles from both streams are intelligently conveyed to a high-speed group packaging station. This unit can assemble bottles into predefined patterns (2×3, 3×4), place them into cardboard trays or partitions, and apply a full or partial shrink wrap bundle. This automated secondary packaging is essential for creating retail-ready multipacks, improving warehouse palletization, and reducing manual handling damage—a critical value-add for products destined for supermarket shelves across the Global South.
3. Centralized Control System with Multi-Language HMI: A master Programmable Logic Controller (PLC) oversees the entire complex operation. The multi-language Human-Machine Interface (HMI) provides operators with separate control panels for each filling block and the packer, allowing for individual recipe management, speed adjustment, and fault diagnosis. The system can store hundreds of recipes for different container sizes, fill volumes, and pack patterns, enabling swift changeovers at the touch of a button.
Technical Specifications, Compliance, and Material Compatibility
-
Machine Type: Fully Automatic, Dual-Stream Integrated Packaging Line with Secondary Group Packager.
-
Primary Applications: Automotive Chemicals (Oils, Additives, Cleaners), Industrial Solvents & Lubricants, Household & Institutional Cleaners, Agrochemicals, Food-Grade Oils & Liquids, Paints & Coatings.
-
Filling Technology: Configurable per block. Options include Piston Filling, Peristaltic Pump Filling, Gravity Filling, and Overflow Filling. Each can be specified with product-compatible wetted parts (PTFE, 316L SS, PP).
-
Aggressive Product Handling: For corrosive chemicals, the line can be specified with ATEX-compliant components, explosion-proof motors, and specialized seal materials (Viton, EPDM, Kalrez) to ensure safety and durability.
-
Group Packaging Options: Automatic tray erector, partition inserter, shrink wrapping tunnel, or case packer. Configurable for various pack sizes and film types.
-
Output Capacity: High-speed design scalable to production needs. Output is effectively doubled due to parallel filling, with total line speeds possible from 4,000 to 15,000+ containers per hour depending on configuration.
-
Control System: Industrial-grade PLC network with integrated safety relays and SCADA capability for production data reporting.
-
Construction & Hygiene: GMP-ready design with all product contact surfaces in AISI 316L Stainless Steel. Features fully automated Clean-in-Place and Sterilize-in-Place (CIP/SIP) systems with separate circuits for each product line to prevent any cross-contamination risk.
-
Compliance Base: Designed to facilitate CE, EAC, and ISO 9001 certifications. GMP principles and HACCP support are integrated into the design. ATEX Zone 2 / Division 2 options are available for volatile solvents.
Target Applications and Unmatched Operational Advantages
This line is the ultimate strategic asset for:
-
Multi-Product Chemical Manufacturers: Companies producing a range from mild detergents to strong acids or alkalis under one roof.
-
Large-Scale Contract Packaging (Co-Packing) Facilities: Plants that need to offer clients dedicated, contamination-free filling lines for different product categories within a single footprint.
-
Global FMCG Brands with Regional Production: Companies requiring local plants to package both household chemical and food-grade lines with maximum flexibility.
The operational advantages are transformative. Maximum Plant Utilization is achieved by eliminating changeover downtime between product types. Unmatched Flexibility allows rapid response to market demand for different products. Enhanced Safety and Quality are ensured by dedicated, product-specific filling circuits with full traceability. Logistics Optimization is achieved through in-line multipacking, reducing downstream labor and packaging costs.
Global Support, Validation, and Strategic Implementation Framework
We engineer success by pairing advanced machinery with unparalleled support. The R-400 comes with a 24-month comprehensive performance guarantee. Our global infrastructure ensures on-site commissioning in under 72 hours from hubs in Dubai (MENA), Hanoi (SEA), and Lagos (Africa), with region-specific spare parts kits available in under 24 hours. We provide complete validation support (IQ/OQ/PQ documentation) to meet FDA, EU, and local regulatory expectations. Our service includes 24/7 remote monitoring, multi-language technical support (EN/RU/AR/ES), and free line configuration engineering for your specific products. With voltage customization (110V-480V) and a free efficiency audit boasting a 15% output improvement guarantee, the R-400 is not just an equipment purchase—it is a strategic partnership for achieving manufacturing excellence, supply chain resilience, and market dominance in the complex landscape of chemical and industrial product packaging.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.