The global imperative for hygiene has permanently transformed the landscape for antiseptic and sanitizer production. Meeting this sustained demand requires more than makeshift solutions; it demands industrial-grade, reliable, and scalable automation. Locus Robotics delivers precisely that: engineered complete turnkey filling lines designed explicitly for the rigorous production of alcohol-based gels, liquid sanitizers, disinfectant sprays, and related chemical formulations. Our integrated systems are built to handle the unique challenges of these products—from high-viscosity gels and volatile alcohols to stringent regulatory standards—while delivering unparalleled output, accuracy, and operational safety. Designed for resilience in the demanding environments of Southeast Asia, Africa, the Middle East, Latin America, and Eastern Europe, this line is your strategic asset to secure market share, ensure consistent quality, and achieve rapid Return on Investment (ROI) in the essential hygiene sector.
Navigating the New Normal of Hygiene Manufacturing:
The post-pandemic era is not a spike but a plateau of elevated demand. Manufacturers face a triad of critical challenges: the need for drastically increased throughput to fulfill large-scale contracts, the necessity of flawless product consistency to protect brand reputation in a competitive market, and adherence to evolving global and regional regulatory standards for disinfectants and antiseptics. Manual or semi-automatic processes are a bottleneck, introducing risks of contamination, fill-volume inconsistency leading to costly giveaways or regulatory non-compliance, and an inability to scale profitably.
The Locus Robotics Answer:
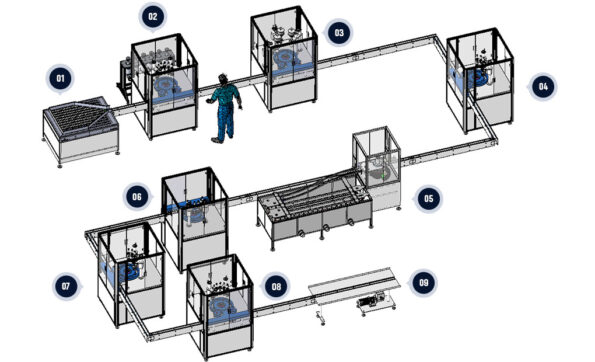
We provide a singular, integrated solution that eradicates these bottlenecks. Our turnkey line is not a collection of machines but a synchronized production ecosystem. From the moment a raw container is introduced to the point a sealed, labeled, and batch-coded case is palletized, every process is optimized for the specific rheology and safety requirements of antiseptic products. We engineer for high-viscosity gel transfer without shear degradation, precise dosing of high-alcohol-content liquids, and safe handling of flammable components where required. This holistic approach transforms your production facility from a constraint into a core competitive advantage, enabling you to respond with agility to market opportunities and tender specifications worldwide.
The Precision Filling Module
The Heart of Accuracy and Yield Preservation:
For high-value chemical products like sanitizers, every milliliter counts. Inaccurate filling erodes profit through giveaway or risks regulatory rejection for under-filling. Our filling modules are engineered for volumetric perfection.
-
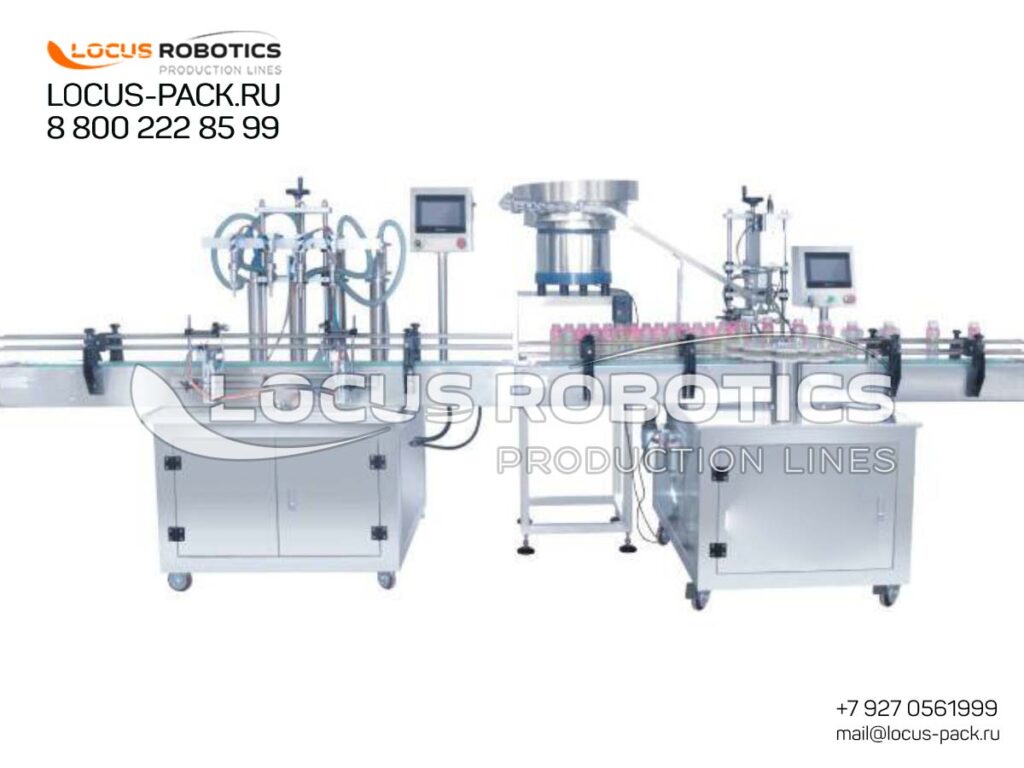
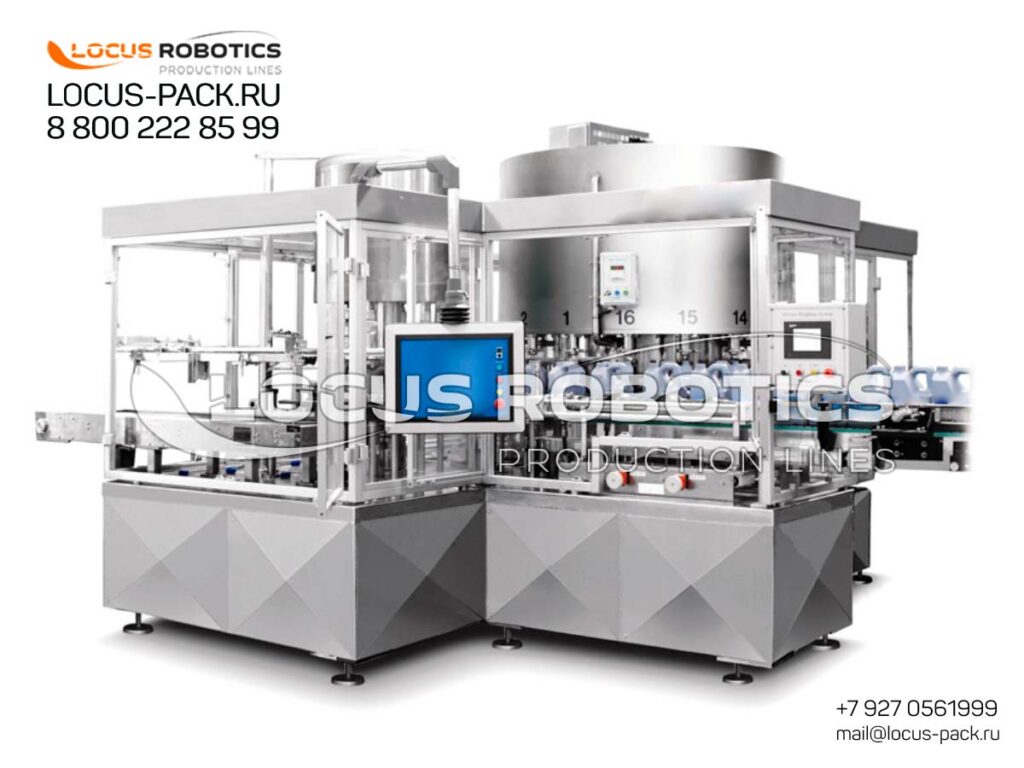
Technology Selection: For non-foaming gels and liquids, our servo-piston fillers provide unmatched accuracy, typically within ±0.5%, ensuring every bottle contains the exact advertised volume. For more volatile or foaming liquid sanitizers, gravity or overflow fillers offer high-speed, consistent performance. All product contact parts are crafted from AISI 316L stainless steel or PTFE-coated components for superior chemical resistance and easy cleaning, critical for maintaining product purity and meeting GMP-like hygienic standards even in non-sterile applications.
-
Handling Product Challenges: We integrate de-aeration systems for viscous gels to prevent air pockets and ensure precise volumetric control. Fillers are equipped with drip-free nozzles and quick-change tooling to switch between different bottle neck sizes and product types (e.g., from gel to liquid) in minutes, maximizing line flexibility for contract manufacturers or brands with diverse SKUs.
-
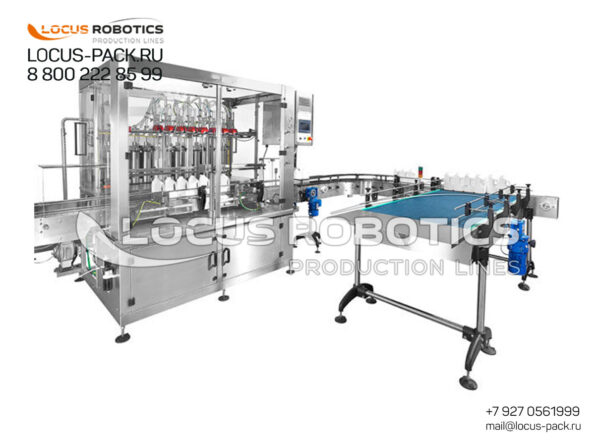
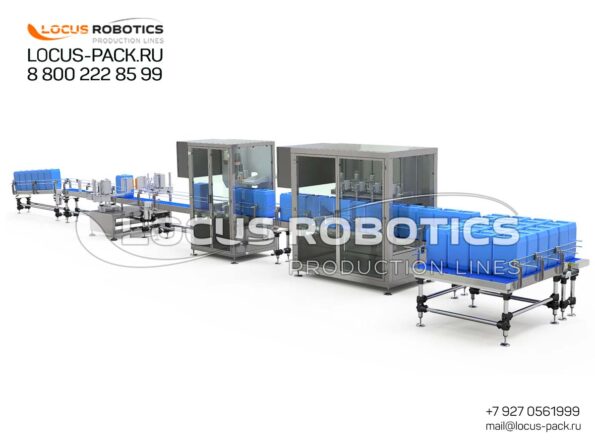
Scalable Architecture: The filling module can be configured from a single head for pilot production to rotary systems with 16, 32, or more heads for outputs exceeding 15,000 bottles per hour. This modularity allows you to start at a feasible scale and expand capacity seamlessly as your business grows.
Robust Capping & Sealing
This focus on precision is not just about cost savings; it is a fundamental commitment to product integrity and brand trust in a highly scrutinized market.
Ensuring Product Integrity and User Safety:
A perfect fill is secured by a perfect seal. Sanitizer packaging employs a wide variety of closures, from simple screw caps and flip-tops to complex spray pumps and tamper-evident seals. Our capping stations are masters of adaptability and precision.
-
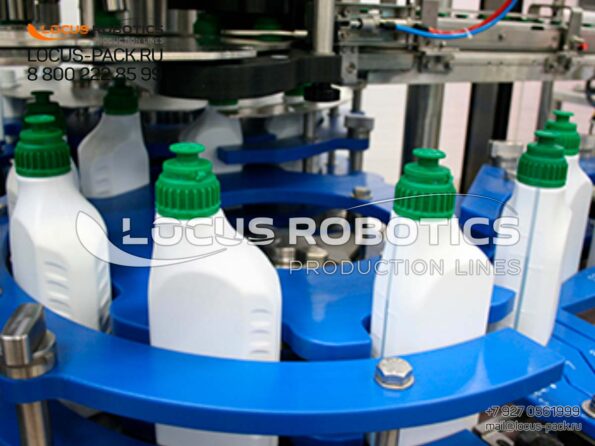
Versatile Closure Handling: We equip lines with automatic cap sorters and elevators to feed closures reliably. The capping technology is then matched to the application: magnetic torque spindles for precise, consistent application of plastic screw caps and CR (child-resistant) closures; press-on heads for flip-tops and spray pumps; and roll-on (ROPP) spinners for aluminum seals on larger containers.
-
Critical Quality Parameters: For screw caps, precise torque control is vital—too loose risks leaks and evaporation of alcohol, too tight can damage containers or frustrate end-users. Our systems provide and log this data. For pumps, consistent activation and sealing force ensures they work perfectly on the first use. Every sealing action is designed to guarantee the product remains effective and safe throughout its shelf life.
-
Integration and Uptime: The capper is fully synchronized with the filler and conveyor, creating a continuous flow. Robust design and easy access for maintenance ensure this critical station does not become a source of downtime in your high-throughput operation.
Labeling, Coding & Inspection
Compliance, Traceability, and Brand Presentation:
In regulated markets, proper identification is not optional. Our lines automate the entire identification process, ensuring compliance and enhancing brand value.
-
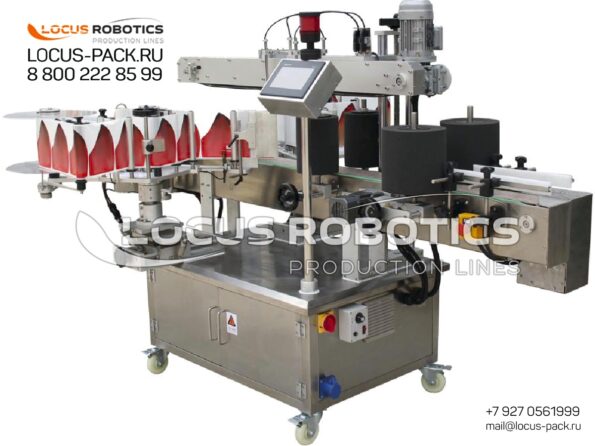
Precision Labeling: We integrate pressure-sensitive (PS) labelers for high-speed application of front, back, and wrap-around labels. For a premium look or specific material requirements, hot-melt glue labelers are available. Systems include automatic label verification to reject misaligned or missing labels.
-
Mandatory Marking: High-resolution inkjet or thermal transfer overprinters are integrated to print batch codes, expiry dates, manufacturing dates, and barcodes directly onto the bottle or label. This is essential for global traceability regulations (e.g., WHO-GMP, FDA guidelines) and supply chain management.
-
100% Quality Assurance: A machine vision inspection system acts as the final quality gate. It can verify fill level (via ullage inspection), cap presence and correct seating, label presence and accuracy, and even print quality. Any non-conforming unit is automatically rejected, ensuring only perfect products are packed.
-
Data Integrity: All coding and inspection data can be logged and integrated into factory MES/ERP systems, providing a complete electronic batch record for audits and quality control.
Regulatory Design & Safety Compliance
Engineered for Trust in a Regulated Sphere:
Producing chemical-based disinfectants carries inherent responsibilities. Our lines are designed to meet the highest applicable standards for safety, hygiene, and documentation.
-
Hygienic Design Philosophy: Even for non-sterile products, we employ GMP-influenced design principles: all frames use rounded, sloped stainless steel to prevent dirt accumulation; equipment is designed for easy access and cleanability; and pneumatic systems use oil-free compressors to avoid product contamination.
-
Intrinsic Safety: For lines handling high-percentage alcohol (a Class I flammable liquid), we offer ATEX-certified components (motors, sensors, control panels) for use in potentially explosive atmospheres (Zone 1 or 2). Comprehensive safety guarding, light curtains, and emergency stop circuits protect your operators.
-
Documentation & Validation Support: We provide comprehensive documentation packages, including P&ID diagrams, electrical schematics, and material certifications. For clients requiring it, we can support Factory Acceptance Tests (FAT), Site Acceptance Tests (SAT), and the creation of validation protocols (IQ/OQ) to satisfy regulatory audits from bodies like the FDA, EMA, or regional health authorities.
Line Flexibility & Scalability
Future-Proof Your Investment:
Market needs evolve. Today’s hand sanitizer line could tomorrow package surface disinfectants, detergents, or automotive chemicals. We build inherent flexibility into our systems.
-
Quick Changeover: The line features tool-less or minimal-tool changeover for starwheels, filling nozzles, cap chucks, and labeler attachments. This allows switching between different container sizes and types in under 30 minutes, minimizing downtime and enabling efficient small-batch production.
-
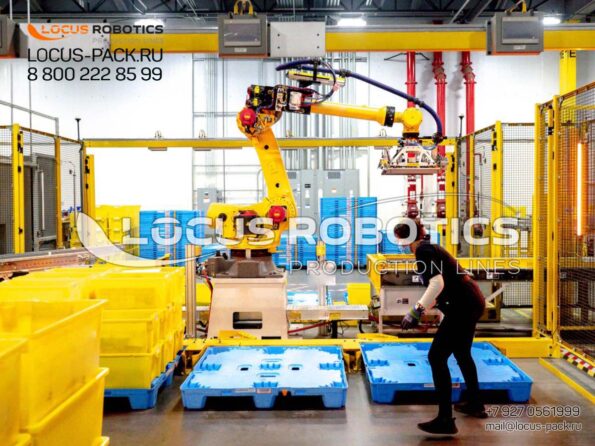
Modular Expansion: The line is conceived modularly. You can begin with a core filler-capper-labeler unit. As volume grows, you can seamlessly add upstream modules like an automatic bottle unscrambler and air cleaner, or downstream modules like an automatic case packer and palletizer. This protects your initial investment and allows capital expenditure to follow growth.
-
Product Versatility: With appropriate material compatibility checks, the same line can often be adapted for a range of water-based or alcohol-based liquid and gel products, maximizing asset utilization for contract manufacturers or diversified brands.
Your Partner in Essential Production
We understand that installing a major production line is a significant decision. Our partnership model ensures your success from day one.
-
Consultation & Feasibility: Our engineers analyze your product samples, container specifications, and output goals to create a tailored line layout and quotation.
-
Collaborative Design: We finalize specifications, ensuring the line meets your exact factory layout, utility constraints, and automation level requirements.
-
Manufacturing & FAT: The line is built and assembled in our facility, where we conduct a comprehensive Factory Acceptance Test (FAT) with your team, proving performance before shipment.
-
Installation & Commissioning: Our engineers supervise installation and perform Site Acceptance Testing (SAT), ensuring the line is fully operational and your staff is trained.
-
Lifelong Support: Through our global network, we provide 24/7 remote support, spare parts, and technical upgrades to guarantee your line’s productivity for its entire lifecycle.
Ready to become a leader in essential hygiene production? Contact our Sanitizer Line Specialists for a detailed project consultation and quote.