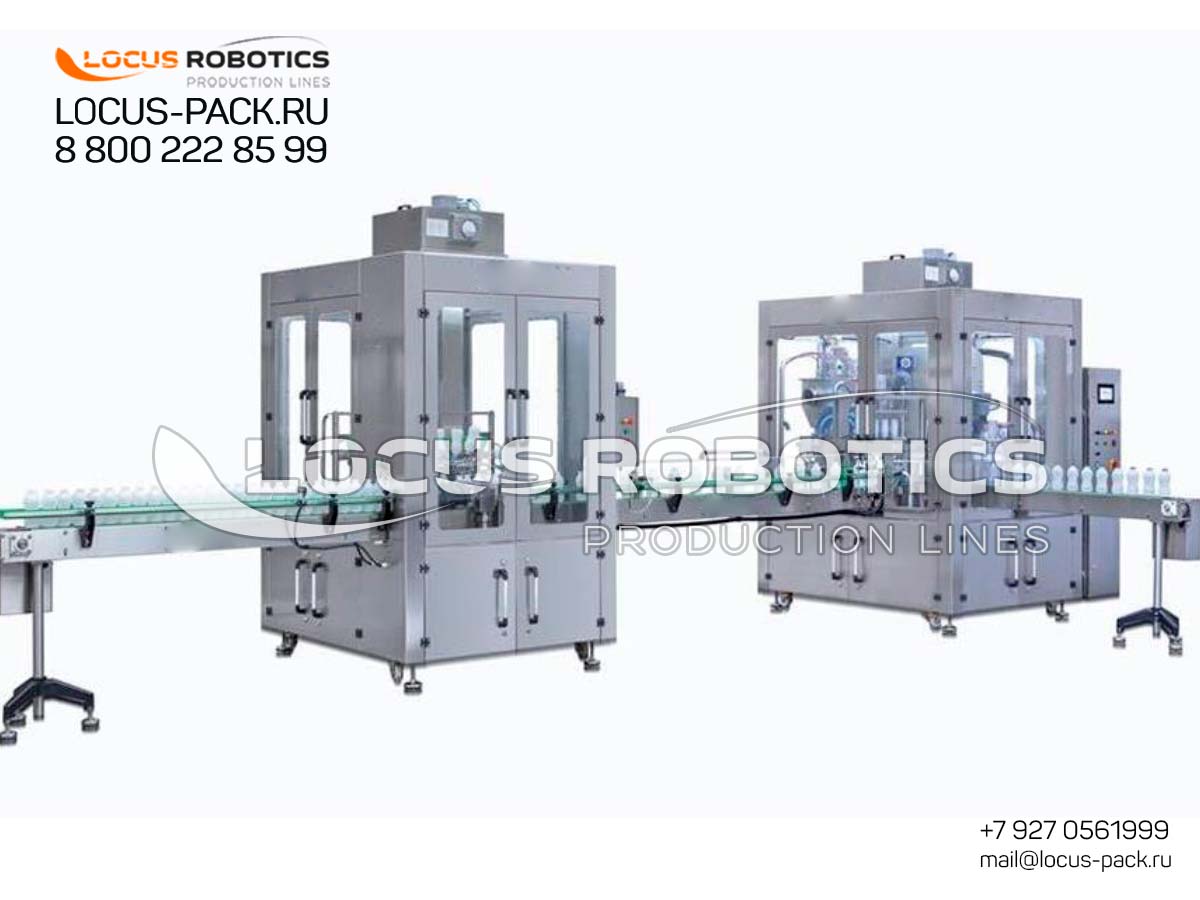
Description
Advanced Aseptic & Hot-Fill Technology for Shelf-Stable Beverages
High-Efficiency Chemical or Sterile Air Bottle Rinser/Sanitizer.
Pressurized Sterile Zone and Positive Air Pressure System.
Temperature-Controlled Rotary Hot-Fill Valve Technology.
Steam or Peroxide Sterilized Cap Handling & Sealing.
The R-600 represents a pinnacle of food packaging engineering, merging aseptic processing with precise hot-fill technology to create a robust barrier against spoilage. This line is not merely a filler; it is a guaranteed sterility delivery system for low-acid (pH >4.6) and high-acid products. The core principle involves filling commercially sterile product into pre-sterilized containers within a sterile environment, followed by a hermetic seal. The «hot-fill» component provides an additional lethality step and creates a vacuum in the headspace upon cooling, further ensuring container integrity and product safety. This dual-technology approach is ideal for challenging climates with inconsistent cold chains, allowing manufacturers in regions across Southeast Asia, Africa, and Latin America to expand their distribution radius significantly, reduce logistics costs, and minimize product waste. The machine’s fully enclosed, pressurized sterile zone, constructed with polished surfaces and minimal joints, is designed to prevent any point of microbial ingress, making it the cornerstone of a modern, audit-ready ESL (Extended Shelf Life) or aseptic production facility.
Detailed Technical Specifications & Sterilization Protocols
-
Machine Type: Fully Automatic, Rotary Monobloc Aseptic Hot-Fill Line.
-
Primary Applications: UHT Milk, Flavored Milk Drinks, Juices & Nectars (citrus, tropical), Dairy Yogurt Drinks, Liquid Coffee/Tea Concentrates, Edible Oils, and Liquid Food Syrups.
-
Process Technology: Combines aseptic sterile zone technology with precision hot-fill process (typically 85°C — 95°C).
-
Container Types: PET (Polyethylene Terephthalate) or PP (Polypropylene) bottles, designed to withstand hot-fill temperatures and vacuum pressure.
-
Bottle Preparation: Integrated chemical (hydrogen peroxide H2O2, peracetic acid PAA) and/or filtered sterile air rinsing/sanitizing station.
-
Filling Accuracy: High-precision volumetric filling with accuracy of ±0.5% or better, critical for cost control and regulatory compliance.
-
Sterile Zone Integrity: Maintained by HEPA-filtered, laminar flow positive air pressure (ISO Class 7/8 equivalent environment) to prevent contamination.
-
Capping System: Aseptic capping with cap sterilization via saturated steam tunnel or hydrogen peroxide bath. Handles screw caps or sports caps.
-
Control & Automation: Redundant control system with a primary PLC and dedicated temperature/pressure controllers. The multi-language HMI provides real-time monitoring of all critical parameters: fill temperature, sterile zone pressure, chemical sterilant concentration, and seal integrity.
-
Key Construction: All product and sterilant contact parts are AISI 316L Stainless Steel. The system includes fully automated CIP (Clean-in-Place) and SIP (Steam-in-Place) circuits for internal sterilization of tanks, valves, and pipelines without disassembly.
-
Output Range: Configurable for outputs relevant to medium and large-scale production, typically from 4,000 to 12,000 bottles per hour (BPH), depending on bottle size.
Integrated System Components: Rinsing, Sterile Filling, and Sealing
1. High-Efficiency Chemical or Sterile Air Bottle Rinser/Sanitizer: The process begins with a critical decontamination step. Bottles are inverted and subjected to a high-velocity spray or mist of a chemical sterilant (like food-grade hydrogen peroxide) followed by jets of sterile, pyrogen-free air to evaporate residuals, leaving an internally sterile surface. Alternatively, for certain applications, a dry sterilization process using filtered, heated sterile air may be employed.
2. Pressurized Sterile Zone and Positive Air Pressure System: Sterilized bottles enter the heart of the machine—a fully enclosed chamber. This zone is continuously supplied with HEPA-filtered air at a pressure higher than the surrounding room, creating a clean, outward air flow that prevents airborne contaminants from entering. All mechanisms inside this zone, including the filler carousel, are designed for hygienic operation and can be sterilized with steam (SIP).
3. Temperature-Controlled Rotary Hot-Fill Valve Technology: The product, held at the precise UHT temperature, is fed into a sterile product tank within the zone. From there, rotary filling valves, often with double-seat design to prevent drip, dispense the hot liquid. Each valve is temperature-controlled and features a product reheater circuit to ensure every bottle receives product at the exact lethal temperature required for sterilizing the container neck.
4. Steam or Peroxide Sterilized Cap Handling & Sealing: Caps are sterilized inline before application. A common method is a saturated steam tunnel that exposes caps to high-temperature steam for a specified time. Sterilized caps are then transported via a sterile chute to the capping heads, which apply them to the filled bottles. The immediate capping within the sterile zone completes the hermetic seal, locking in sterility.
Target Products, Market Advantages, and Operational Benefits
This line is the definitive solution for processors aiming to capture market share in several key segments:
-
Dairy Processors: Transitioning from chilled fresh milk to shelf-stable UHT milk and flavored drinks for wider distribution.
-
Juice Manufacturers: Producing clear, high-quality tropical fruit juices (mango, guava, litchi) without refrigeration for export markets.
-
New Product Developers: Creating value-added, nutritionally fortified dairy or juice beverages for school feeding programs or retail.
The operational benefits are transformative. Product Shelf Life Extension from days to months revolutionizes logistics. Elimination of Preservatives meets clean-label consumer demand in urban centers. Reduced Cold Chain Dependency drastically cuts energy costs and expands reach into rural or emerging retail networks. For a plant manager, the fully automated CIP/SIP reduces labor-intensive cleaning, enhances repeatability, and provides auditable sterilization records.
Compliance, Validation, and Global Technical Support Framework
The R-600 is engineered to facilitate compliance with the most stringent global food safety standards, including FDA regulations, EU directives on food machinery, and ISO 22000/FSSC 22000. Its design is inherently GMP-compliant and supports HACCP plans with defined Critical Control Points (CCPs) for sterilant concentration, fill temperature, and sterile zone pressure. We provide a complete validation support package (IQ/OQ/PQ) to document the machine’s installation, operational performance, and production of consistently sterile product. This technical documentation is crucial for passing customer and third-party audits. Our global support model for this critical technology includes specialized aseptic training for your engineers, region-stocked spare parts for critical sterile components, and 24/7 remote access for diagnostics from our hubs in Dubai, Hanoi, and Lagos. This ensures that your investment is protected and your production of high-margin, shelf-stable products maintains uninterrupted, guaranteed sterility.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.