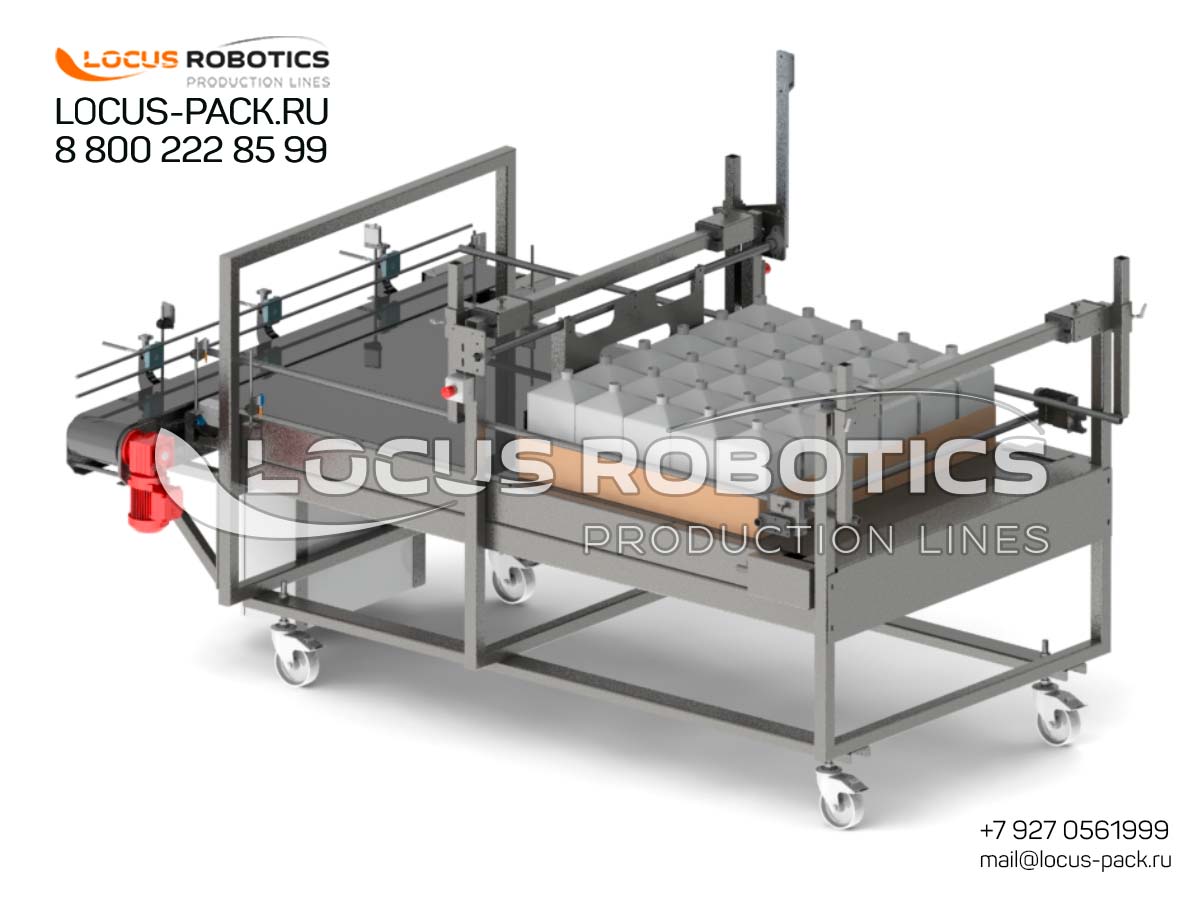
Description
Streamline Your Canister Packaging and Logistics Line
The K-10 Distribution Conveyor solves the critical challenge of handling medium-sized liquid containers in high-volume production environments. It is designed to accommodate the specific dimensions and weight of 5-liter and 10-liter HDPE canisters, which are commonly used for motor oil, cleaning chemicals, and food-grade liquids. By automating the transport and distribution of these canisters, you can eliminate manual handling bottlenecks, reduce product damage, and significantly increase your line’s overall throughput.
Key Features and Technical Advantages
-
Optimized for Standard Canisters: The conveyor’s guiding and drive systems are calibrated for the stable dimensions of common 5L and 10L canisters, ensuring reliable operation.
-
Robust Frame and Belting: Constructed to support the weight of filled canisters, using durable components that resist wear from industrial use and potential chemical exposure.
-
Accumulation and Sorting Logic: Can be equipped with sensors and control logic to create accumulation zones or divert canisters to different lanes for multi-SKU production.
-
Easy Maintenance and Cleaning: Designed with accessibility in mind, allowing for quick maintenance and cleaning to meet hygiene standards in food and pharmaceutical applications.
Technical Specifications
| Parameter | Specification |
|---|---|
| Model | K-10 |
| Target Container Types | 5L & 10L HDPE Canisters (Jerry Cans) |
| Conveyor Type | Distribution/Feeding Conveyor |
| Load Capacity | Max. XX kg per linear meter |
| Speed Range | Adjustable, 0-XX m/min |
| Power Supply | 380V / 50Hz |
| Frame Material | Powder-coated carbon steel or Stainless Steel |
Industries and Applications
This distribution conveyor is essential for high-volume manufacturers across multiple sectors:
-
Chemical & FMCG: Transporting detergent concentrates, automotive fluids (motor oil, coolant), and household chemicals packaged in 5L and 10L cans.
-
Food & Beverage: Handling cooking oils, syrups, and other liquid food ingredients.
-
Cosmetics & Personal Care: Moving bulk liquids for lotions, shampoos, and soaps.
-
Agriculture: Distributing pesticides, fertilizers, and other agro-chemicals.
Built for Global Industrial Demands
The K-10 conveyor is engineered to meet the rigorous requirements of international markets, including Southeast Asia, Africa, the Middle East, Latin America, and Eastern Europe. Its focus on durability, reliability, and ease of integration ensures it delivers consistent performance, reduces downtime, and provides a rapid return on investment for your canister packaging operations.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.