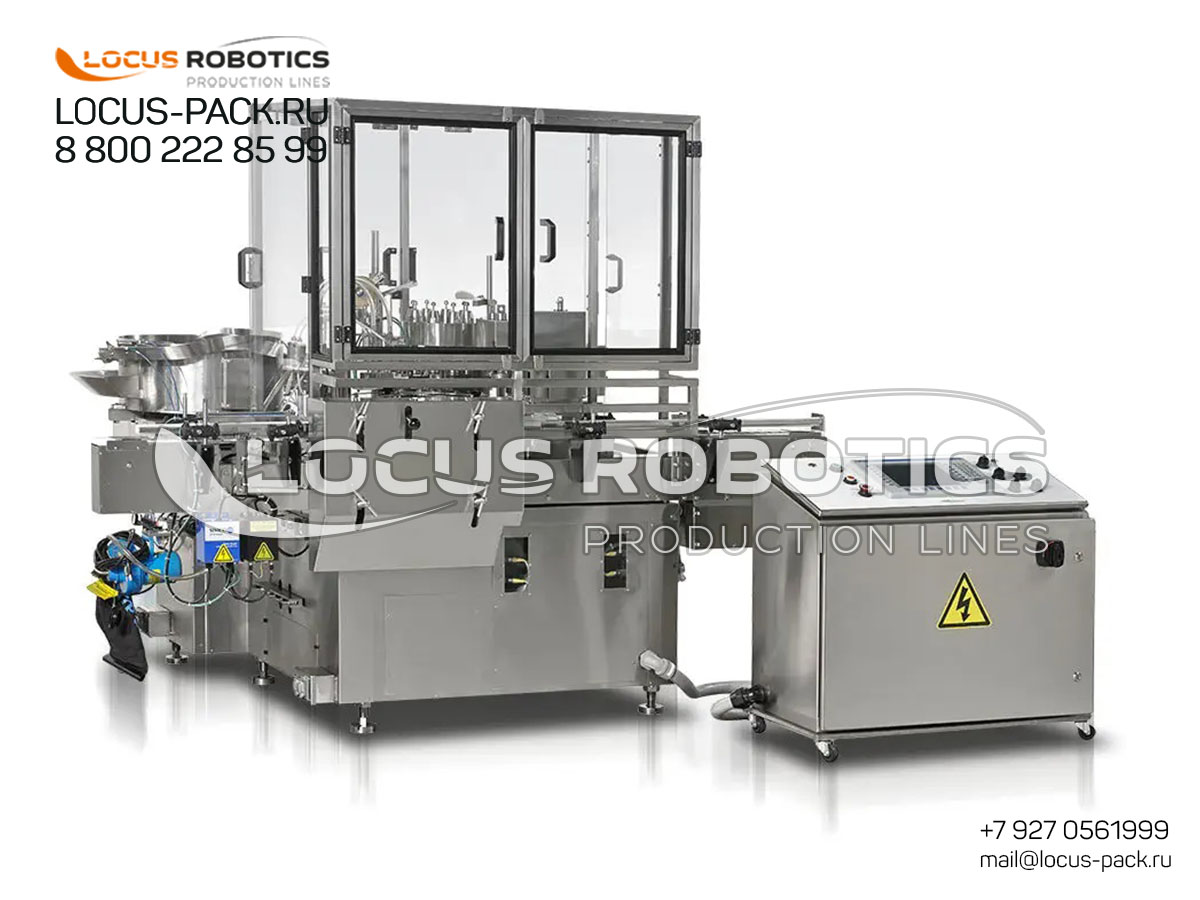
Description
Engineered Safety for Flammable and Volatile Liquid Packaging
This LR-100 variant is purpose-built for applications where standard equipment poses a significant risk. Its core design adheres to stringent explosion-proof (Ex) standards, meaning all electrical components, motors, and controls are engineered to prevent ignition of flammable vapors. Key safety features include a remote control panel that allows operators to manage the machine from a safe distance and specialized construction that contains any potential internal spark or explosion. This allows for the safe handling of Flammable Liquids (FL) and Combustible Liquids (CL) such as high-percentage alcohol solutions, organic solvents, and other volatile chemicals.
Technical Specifications & Safety-Centric Design
-
Machine Type: Automatic, rotary filling and capping monoblock in explosion-proof (ATEX) execution.
-
Core Safety Feature: Remote control panel for operation outside hazardous zones.
-
Filling Technology: Two high-precision peristaltic pump dosing heads (safe for flammable liquids).
-
Automation & Safety: Vibratory cap orienters, protective guarding, and explosion-proof electrical fittings.
-
Primary Application: Alcohol-based tinctures, flammable solvents, volatile chemical products.
-
Certification: Designed to meet ATEX (EU) / IECEx (International) directives for equipment in potentially explosive atmospheres.
Critical Applications for Hazardous Environments
This monoblock is essential for industries where product properties demand the highest level of operational safety:
-
Pharmaceuticals & Herbal Extracts: High-alcohol tinctures, herbal extracts, and medicinal spirits.
-
Chemical & Industrial Manufacturing: Solvents, thinners, adhesives, primers, cleaning concentrates, and volatile additives.
-
Cosmetics & Fragrances: Products with high concentrations of alcohol or flammable aromatic compounds.
-
Automotive & Specialty Chemicals: Fuel additives, brake cleaners, and other aerosol propellant fills.
Certified Safety & Global Operational Support
We provide the certified technology and specialized support required for hazardous material handling worldwide.
-
Safety by Certification: Engineered and constructed to comply with ATEX Directive 2014/34/EU (or local equivalent Ex standards), providing legally mandated safety for Zone 1/21 or Zone 2/22 areas.
-
GMP & Ex Compliance: Combines GMP-ready 316L stainless steel hygiene with explosion-proof safety for a unique dual-compliance solution.
-
Global Hazardous-Support Network: Includes a 24-month performance guarantee, IQ/OQ/PQ support, and access to technicians trained in explosion-proof equipment via our hubs in Dubai, Hanoi, and Lagos.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.