Description
Mastering Shelf-Stable Packaging for the Modern Global Dairy and Beverage Industry
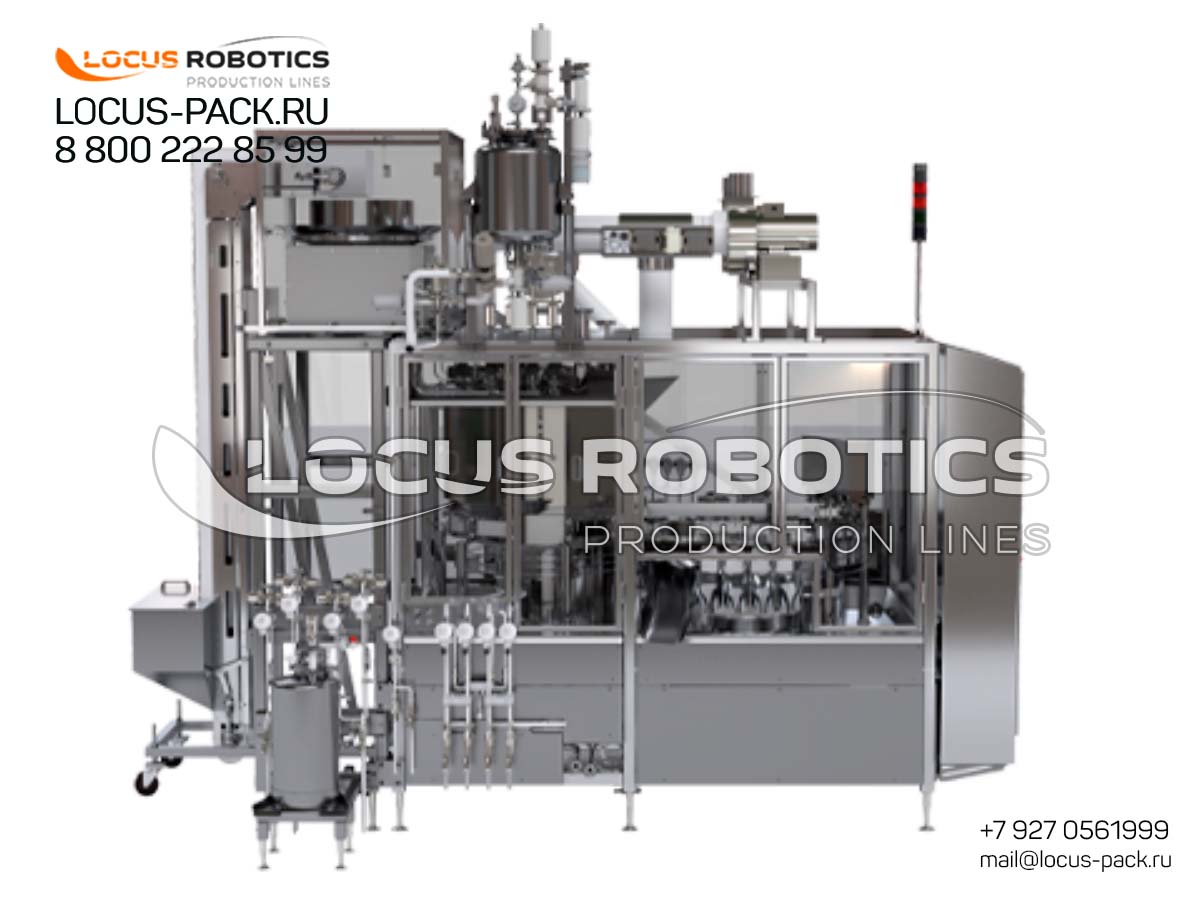
The LR-200 Aseptic Monoblock is a strategic investment for food producers targeting growth in regions with limited cold chain infrastructure or for brands seeking to innovate with convenient, ambient-stable products. This machine is specifically engineered to handle the critical aseptic fill-finish process, where commercially sterile product is filled into pre-sterilized plastic bottles within a sterile environment, and hermetically sealed with sterilized caps. This technology is fundamental for producing the long-life milk, probiotic-rich fermented dairy drinks (like lassi or doogh), and pure fruit juices that dominate supermarket shelves worldwide. The monoblock’s design prioritizes hygiene and cleanability, featuring smooth surfaces, minimal crevices, and components compatible with aggressive sterilization procedures such as steam (SIP) or chemical sanitizers. By adopting this technology, manufacturers can dramatically reduce spoilage, expand their distribution radius, offer consumers greater convenience, and compete effectively in the fast-growing shelf-stable beverage segment. It is an essential platform for companies producing UHT-treated dairy, plant-based milk alternatives, juice blends, and liquid nutritional supplements for retail, food service, and export markets where product safety and longevity are paramount to commercial success.
Detailed Technical Specifications & Hygienic Design
-
Machine Type & Process: Fully Automated Aseptic Rotary (Carousel) Monoblock. Designed to operate within or interface with a sterile zone (e.g., an ISO Class 5 clean air enclosure or a pressurized sterile tunnel) to maintain asepsis during the filling and capping of pre-sterilized plastic bottles.
-
Core Filling Technology: Hygienic volumetric piston dosing system utilizing AISI 316L stainless steel cylinders with sanitary check valves. This positive displacement method provides exceptional accuracy independent of product viscosity, ensuring consistent fill volumes for both thin milk and thicker, viscous drinking yogurts.
-
Aseptic Capping System: Integrated sterilizable screw capping head. This station is designed to accept pre-sterilized plastic screw caps (often treated with hydrogen peroxide vapor or other methods) and apply them with consistent, controlled torque to create a hermetic seal on the bottle.
-
Hygiene & Sterilization Integration: All product-contact surfaces are electropolished AISI 316L / 1.4404 stainless steel. The machine is designed to be Clean-in-Place (CIP) and Sterilize-in-Place (SIP) capable, allowing for thorough internal cleaning and sterilization without disassembly, which is critical for aseptic process validation and preventing biofilm formation.
-
Aseptic Environmental Control: The machine is engineered to integrate with external sterilization systems for bottles (e.g., hydrogen peroxide rinsers or tunnels) and caps. Its design minimizes turbulence and particle generation, maintaining the integrity of the sterile field during operation.
-
Control & Data Recording: Advanced PLC-based control system with a multi-language HMI touchscreen. Provides precise control over all process parameters and includes features for batch reporting, alarm logging, and user access control to support stringent food safety standards (like HACCP, FSSC 22000) and regulatory audits.
Ideal Product Applications & Packaging Formats
-
Target Products: Specifically designed for commercially sterile, low-acid and acidified liquid foods: UHT/HTST milk and cream, fermented milk drinks (yogurt drinks, kefir, buttermilk), liquid yogurt, fruit and vegetable juices/nectars, plant-based milk beverages (soy, almond, oat), and ready-to-drink (RTD) tea or coffee beverages.
-
Target Containers & Closures: Configured for pre-sterilized plastic bottles, typically PET or HDPE, of various sizes. Applies pre-sterilized plastic screw caps, snap-on lids, or sports caps.
Transformative Business Advantages for Shelf-Stable Production
-
Dramatically Extended Shelf Life & Market Expansion: Aseptic packaging enables shelf stability of 6-12 months or more without refrigeration. This allows you to ship products over longer distances, reduce costly cold chain logistics, enter new geographic markets, and reduce retail returns due to spoilage.
-
Superior Product Quality & Nutrient Retention: By filling products sterilely after UHT treatment, you lock in fresh flavor, color, and vitamins much more effectively than with traditional hot-fill methods for plastics. This results in a higher-quality product that better meets consumer expectations for taste and natural goodness.
-
Packaging Flexibility & Consumer Appeal: Aseptic technology allows for the use of lightweight, cost-effective, and recyclable plastic bottles that are convenient and safe for consumers. This modern packaging format is highly attractive for on-the-go consumption and helps build a contemporary brand image.
-
Reduced Operational Costs & Environmental Impact: The long ambient shelf life minimizes warehouse refrigeration costs and product waste. Lightweight plastic bottles also reduce transportation fuel costs and carbon footprint compared to glass, contributing to more sustainable operations.
-
Globally Certified & Supported Food Safety Platform: The machine is designed to meet the most rigorous international food safety standards (ISO 22000, SQF) and GMP guidelines. Coupled with our 24/7 global support network—including specialized service hubs in Dubai, Hanoi, and Lagos—and validation support documentation, we ensure your aseptic line is compliant, reliable, and supported anywhere you produce.
Unlock the Potential of Shelf-Stable Dairy and Beverages
Ready to explore how aseptic technology can revolutionize your product portfolio and distribution capabilities? Contact our food and beverage processing specialists today for a comprehensive consultation and a free aseptic process review. We can provide a detailed feasibility analysis and throughput simulation to demonstrate how the LR-200 Aseptic Monoblock can be the cornerstone of your next growth phase.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.