Description
Safe, Precise, and Contained Dosing for Demanding Industrial Liquids
Engineered for Safety and Accuracy in Chemical Processing
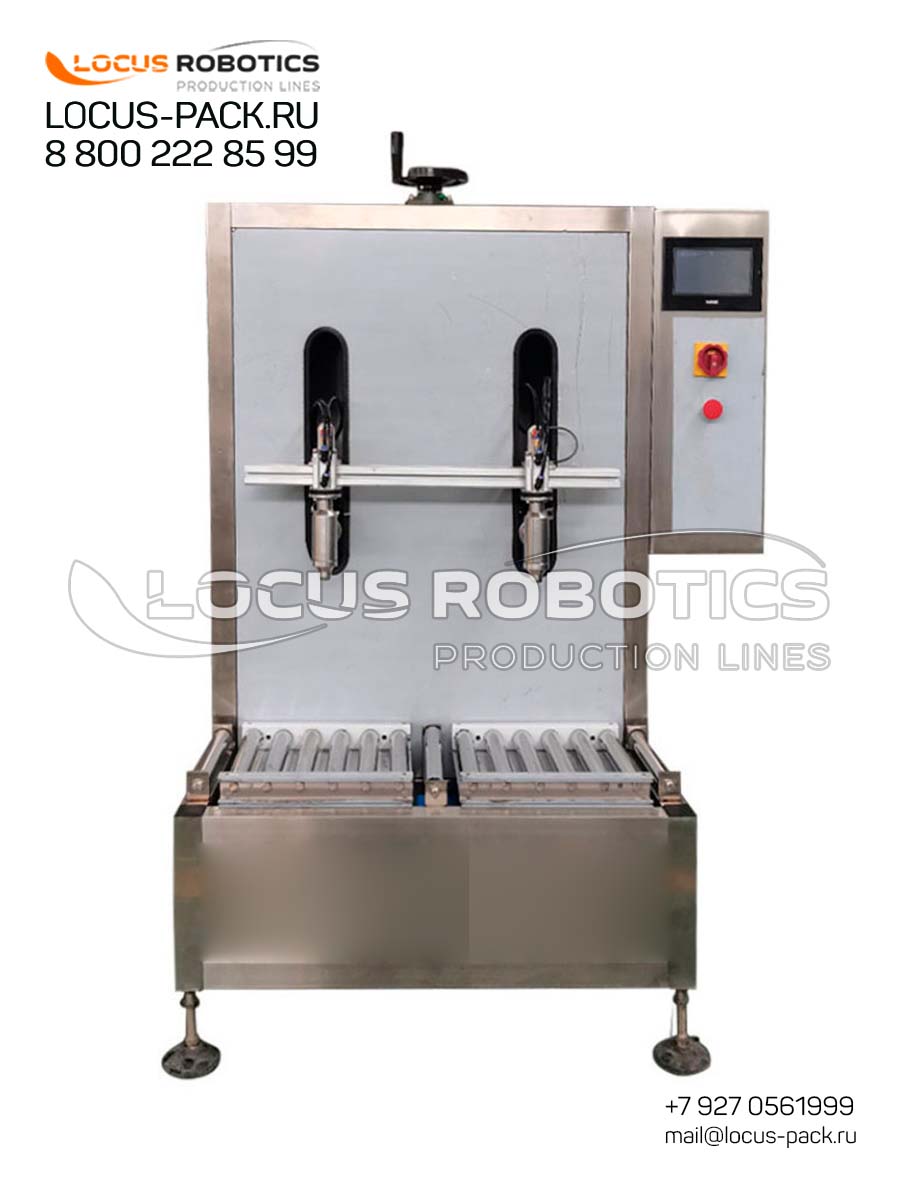
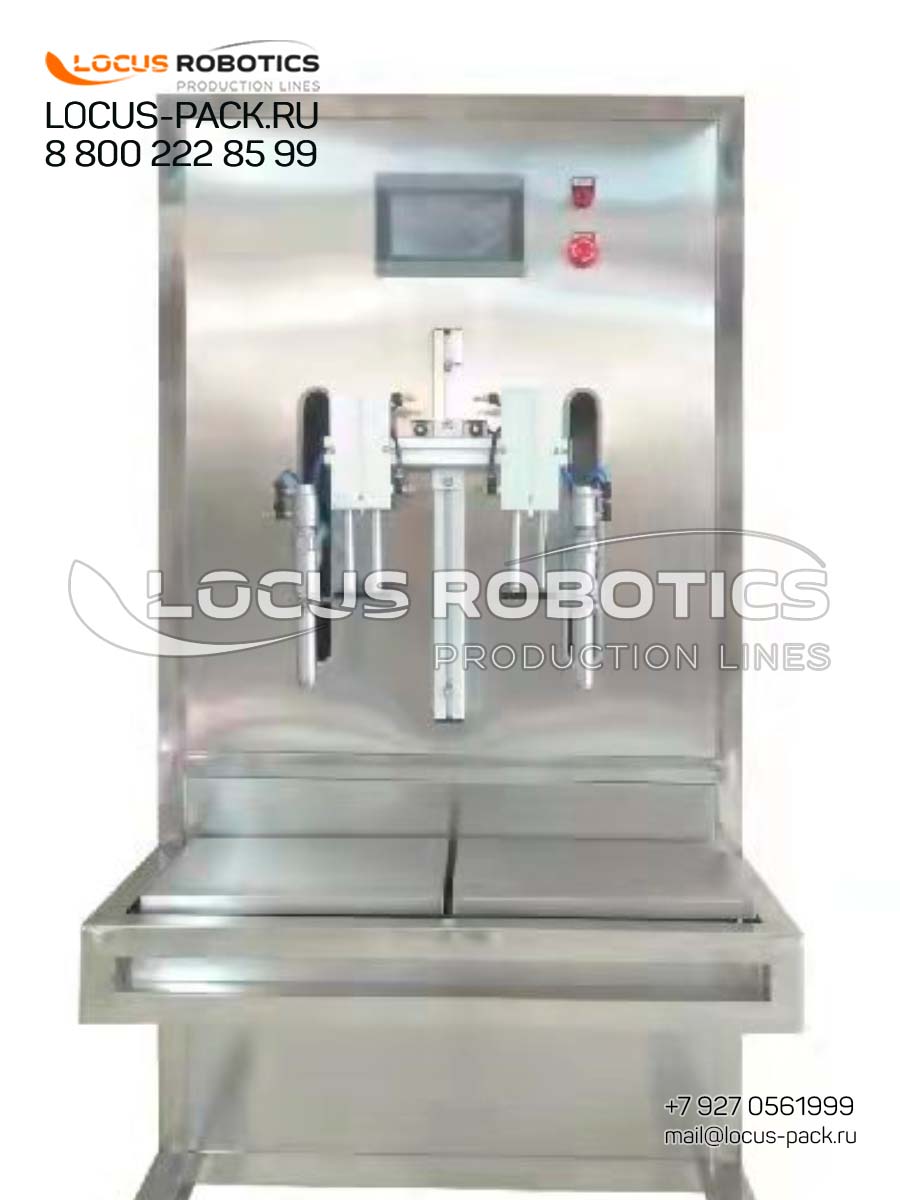
In industries where operator safety and product consistency are paramount, the LB-10 provides a robust solution. The enclosed design is not just a feature but a critical safety system for managing aggressive substances, aligning with the highest standards for industrial hygiene and risk mitigation. Its weight-based dosing method guarantees accuracy unaffected by changes in liquid viscosity or temperature.
Technical Highlights and Key Features
-
Enclosed Safety Design: The primary feature that sets this system apart. It completely contains the filling process, preventing the escape of hazardous vapors and protecting the product from external contaminants. This is essential for potent, toxic, or hygroscopic chemicals.
-
Dual Descending Nozzles: Two independently controlled nozzles that lower into the containers, enabling bottom-up filling. This method significantly reduces turbulence, aerosol generation, and static electricity buildup, which is vital for foaming liquids or volatile solvents.
-
Gravimetric (Weight-Based) Filling: The core of the system relies on high-precision strain gauge technology (load cells) to ensure fill weight accuracy. This method is superior to volumetric filling for aggressive chemicals, as it provides consistent mass measurement regardless of product density or aeration.
-
Corrosion-Resistant Construction: To withstand harsh chemicals, the LB-10 is constructed with compatible materials such as AISI 316/316L stainless steel, PTFE, or PVDF for all wetted parts and the cabinet interior, ensuring long-term durability and resistance to corrosion.
-
Automated Control System: The system is managed by a Programmable Logic Controller (PLC) with a touchscreen Human-Machine Interface (HMI). This allows for easy recipe management, setpoint adjustment, and comprehensive data logging for batch traceability and quality control.
Industries and Applications
The LB-10 is specialized for sectors handling hazardous liquids:
-
Industrial & Specialty Chemicals: Filling aggressive solvents, acids, alkalis, and chlorinated products.
-
Petrochemicals: Handling lubricants, additives, and chemical intermediates.
-
Water Treatment: Packaging chlorine-based disinfectants and other treatment chemicals.
Why Choose This System?
-
Enhanced Operational Safety: The enclosed design and automated process minimize operator exposure to hazardous chemicals.
-
Exceptional Accuracy: Weight-based filling ensures consistent fill mass, minimizing product giveaway of expensive raw materials.
-
Process Integrity: Contained environment and cleanable design prevent cross-contamination and support compliance with stringent regulatory standards.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.