Description
Efficient and Simple Liquid Transfer: A Rugged Filling Station for Diverse Containers
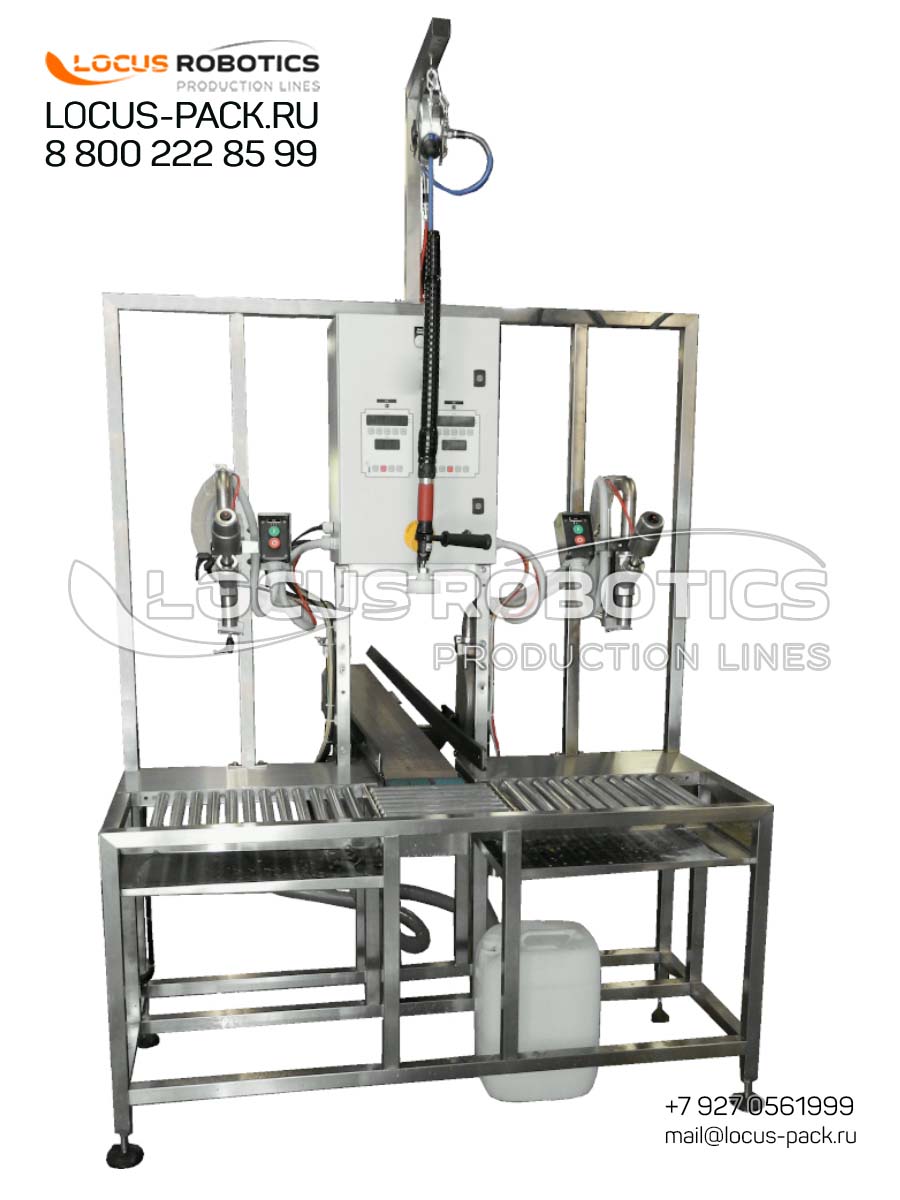
Not all packaging tasks require complex, high-speed automation. For operations centered on dispensing free-flowing liquids from bulk storage into intermediate or final containers, simplicity, reliability, and ease of maintenance are paramount. The R-500 Semi-Automatic Gravity Filling Station embodies this philosophy, providing a mechanically simple, highly reliable, and operator-friendly alternative to manual pouring or more expensive pump-driven systems. Its design focuses on minimizing downtime and maximizing ease of use, with straightforward components that are easy to clean and service. This station is the ideal choice for facilities that require flexibility in container type and product, have moderate throughput needs, or operate in environments where electrical complexity is undesirable. It effectively eliminates the strain, spillage, and inconsistency of purely manual methods, offering a significant upgrade in process control and worker efficiency.
Technical Overview: Gravity-Based Dosing, Dual Nozzles, and Ergonomic Handling
-
Gravity-Feed Dosing System: The operation is based on a simple yet effective principle. A product supply tank (not always included) is positioned above the filling nozzles. Liquid flows by gravity, and the fill volume is controlled by manually operated ball valves or timers on each nozzle. This system is inherently reliable, requires no complex pumps for thin liquids, and is easy to maintain.
-
Twin Nozzle Configuration & Roller Conveyor: The station is equipped with two filling nozzles, enabling the filling of two containers simultaneously or providing a backup. Nozzles are often height-adjustable to accommodate different container sizes. The powered or gravity-based output roller conveyor is a critical ergonomic feature, allowing operators to smoothly roll heavy filled containers (like 20L jerrycans) to the next station (capping, labeling) without lifting.
-
Construction & Operation: Built with a heavy-duty steel frame for stability. Product contact parts are typically stainless steel or chemical-resistant plastics for compatibility with a wide range of liquids. Operation is purely mechanical/semi-automatic: an operator places containers, opens the valve for a timed duration, and closes it.
-
Typical Specifications & Options:
-
Filling Method: Time-based gravity fill.
-
Nozzles: 2 standard, with various drip-free tip options.
-
Conveyor: Short-length roller conveyor for ergonomic offloading.
-
Options: Stainless steel construction, different nozzle types, integration with a supply tank or IBC adapter.
-
Target Applications: Versatile Use in Chemical, Automotive, and Food Sectors
The R-500’s simplicity makes it applicable across multiple industries for secondary packaging or bulk transfer:
-
Chemical & Industrial Supply: Dispensing liquid detergents, mild acids/alkalis, water-based solutions, and industrial lubricants from drums into smaller jerrycans or pails for distribution or in-plant use.
-
Automotive Fluids & Workshops: Handling motor oils, transmission fluids, antifreeze, windshield washer fluid, and brake fluid for repackaging or workshop dispensing.
-
Food & Beverage (with appropriate materials): Transferring edible oils, vinegar, syrups, and other free-flowing food liquids in small-scale production or packaging environments.
-
Agriculture: Dispensing liquid fertilizers, pesticides, and herbicides into portable containers.
The Practical Solution for Flexible and Low-Maintenance Production Needs
For businesses prioritizing operational simplicity and cost-effectiveness, the R-500 offers clear advantages:
-
Low Initial Investment and Operating Cost: Provides a significant productivity boost over manual methods at a very accessible price point, with minimal ongoing maintenance or energy costs.
-
Extreme Operational Simplicity: Requires minimal operator training, has no complex electronics or programming, and can be maintained by in-house personnel, ensuring maximum uptime.
-
Durability in Tough Environments: The robust, primarily mechanical design is less susceptible to failure in dusty, humid, or otherwise challenging industrial settings compared to sensitive electronic equipment.
-
Flexibility: Easily adapts to different container shapes and sizes and can be used for various products with simple cleaning between batches.
Built for Reliability with Foundational Support
This equipment is supported by a straightforward and effective service model:
-
Easy Self-Maintenance: Designed for simple troubleshooting and part replacement, with clear manual guidance. Common spare parts (seals, valves) are standard and readily available.
-
Global Supply Network: Although mechanically simple, it is still backed by the ability to source replacement components through our global logistics channels if needed.
-
Robust Warranty: Covered by a standard product warranty on materials and workmanship, ensuring quality and reliability.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.