Description
Automatic Case Packer LRC-100 — Complete Packaging Automation
Robotic Gripper Technology & Gentle Handling.
Production Line Integration & Compatibility.
Operational Benefits & ROI Analysis.
Product Overview & Technical Specifications
System Overview
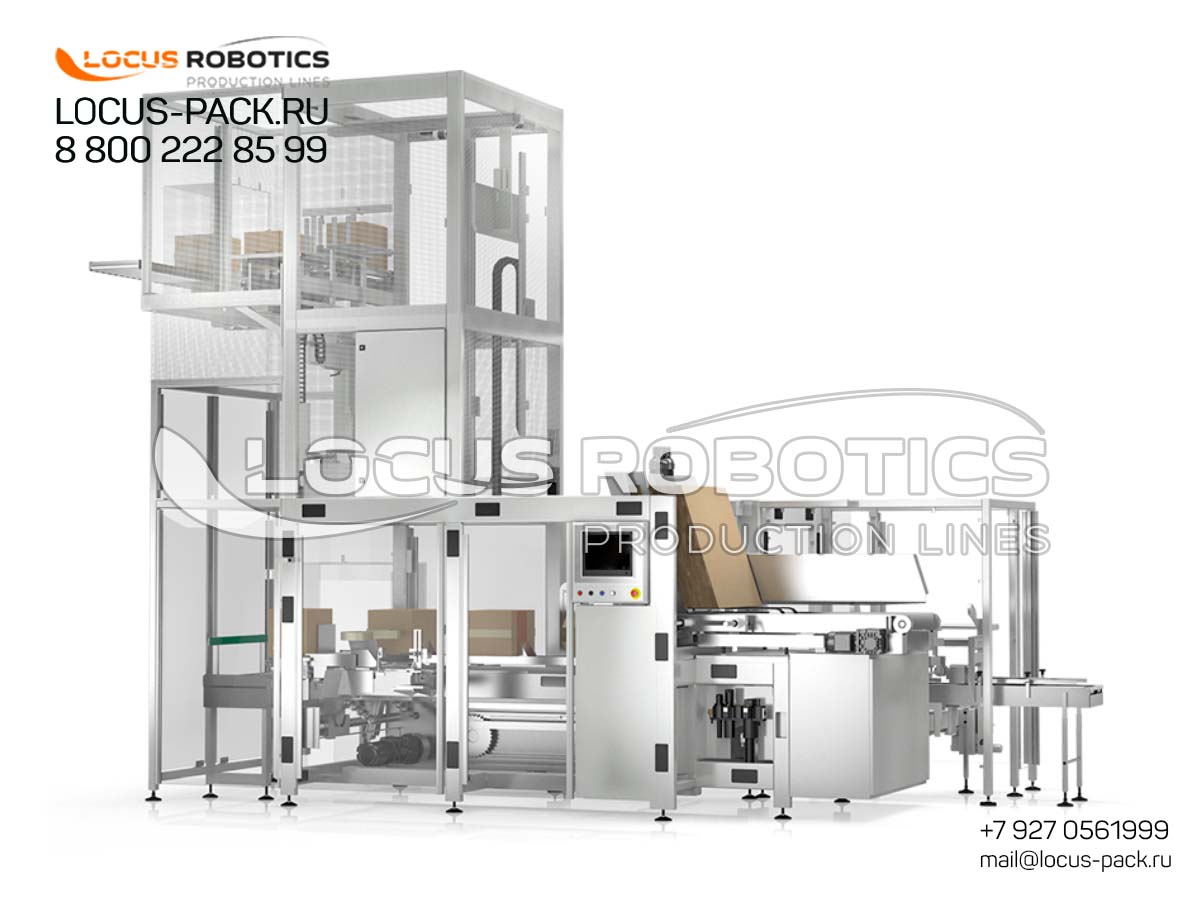
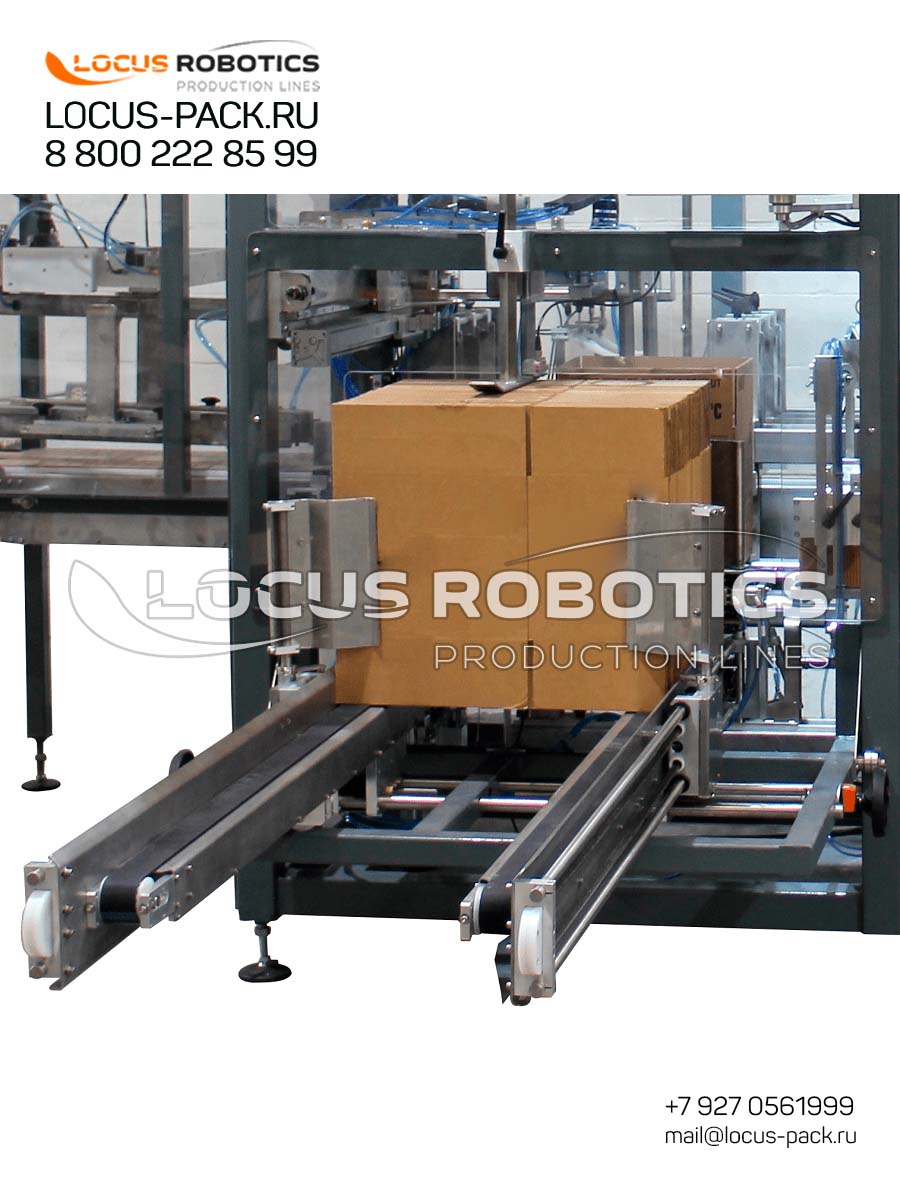
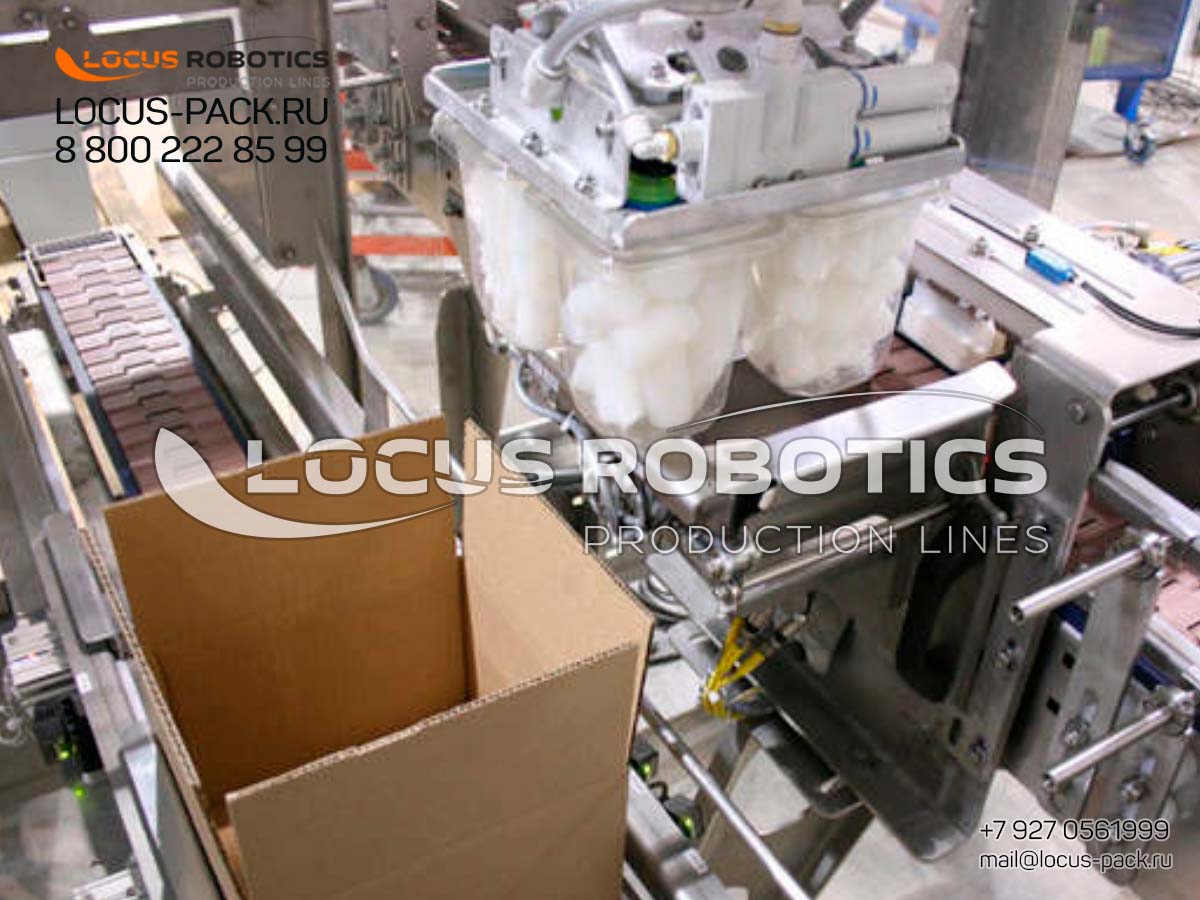
The LRCP-100 appears to be a fully automated case packing system specifically engineered for handling various food products with integrated lift mechanism for efficient case handling. This system combines case erecting, product loading, lift-assisted positioning, and case sealing functions in a single integrated system. The machine is constructed with food-grade stainless steel to meet hygiene standards required for food packaging applications.
The system employs servo motor technology for precise movement control and PLC-based automation for operational management. The LRCP-100 features quick-change capabilities allowing for rapid format adjustments between different container sizes and package configurations.
Technical Specifications
Technical Specifications for LRCP-100 Automatic Case Packer
| Parameter | Specification Range | Technical Notes |
|---|---|---|
| Production Capacity | 10-120 cases/minute | Depending on product type and configuration |
| Lift Mechanism | Integrated elevating system | For efficient case handling |
| Product Types | Various food products | Industry-standard packaging |
| Control System | PLC with HMI interface | Multi-language support |
| Construction Materials | Stainless steel (AISI 304/316) | Food-grade, corrosion-resistant |
| Power Requirements | 380V/3PH/50Hz | Standard industrial power |
Core Features & Technological Advantages
Integrated Lift Mechanism
The LRCP-100 incorporates a specialized lift mechanism that enables efficient case handling and product loading:
-
Vertical case movement: Efficient positioning of cases for product loading
-
Height adjustment: Adaptability to different product and case sizes
-
Gentle product handling: Minimizing damage to food products during loading
-
Space optimization: Efficient use of vertical space in production facilities
This lift mechanism is particularly valuable for food products requiring careful handling and precise positioning during the packaging process.
Automated Case Handling System
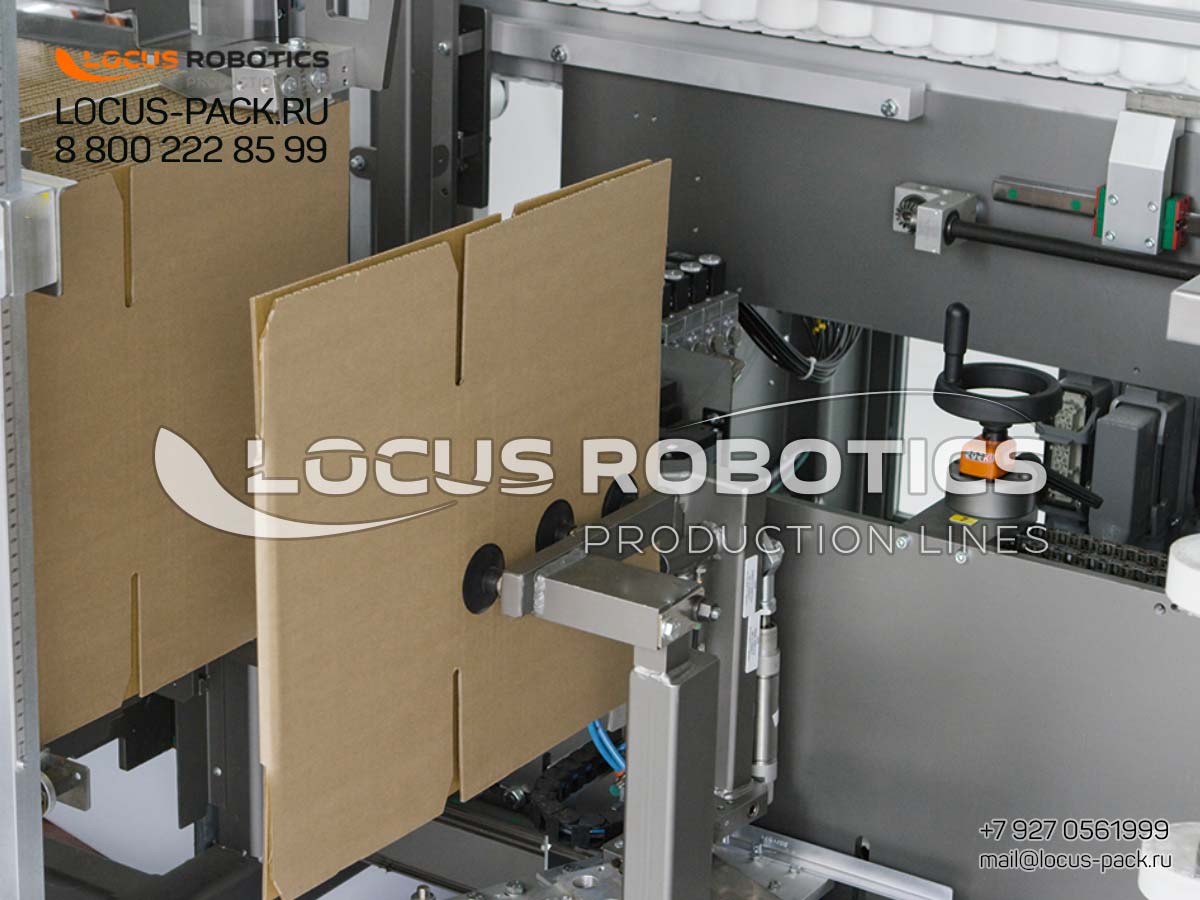
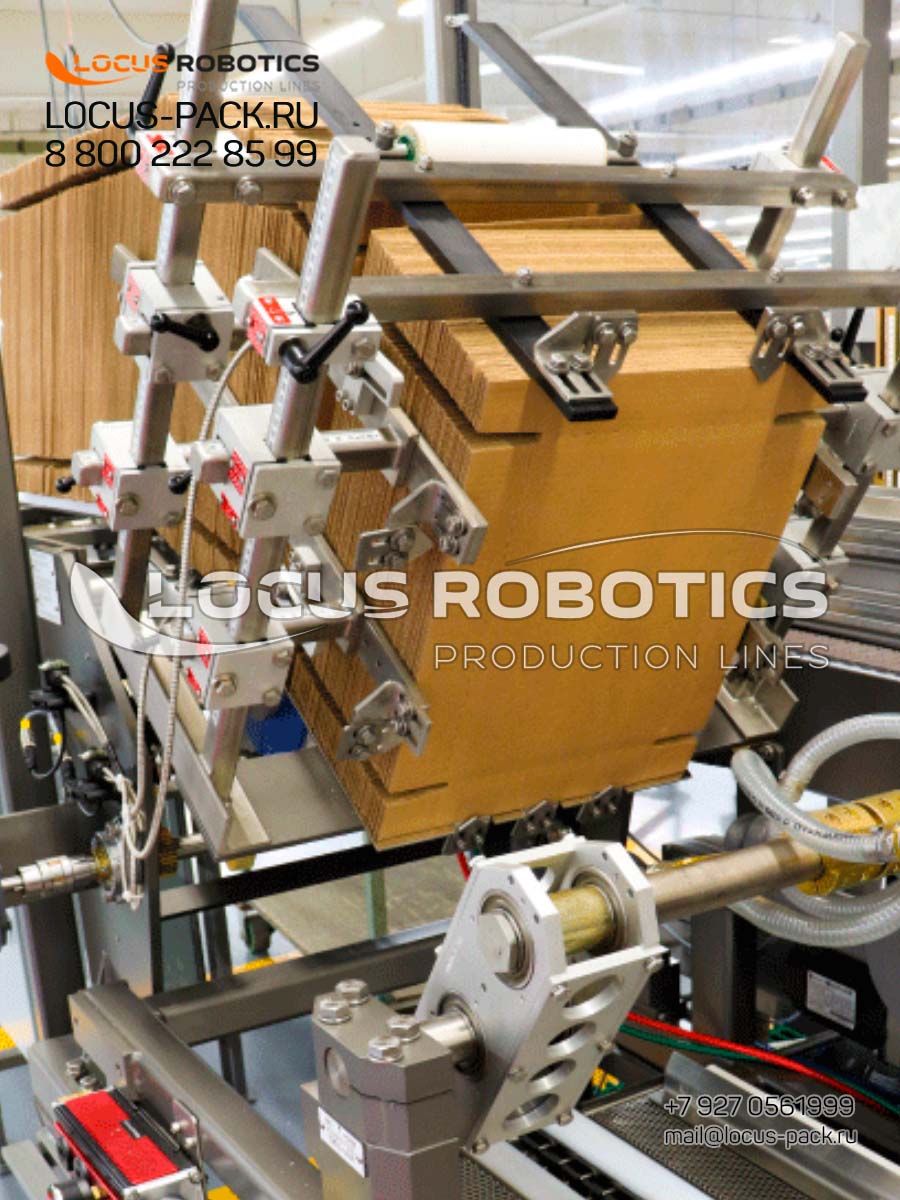
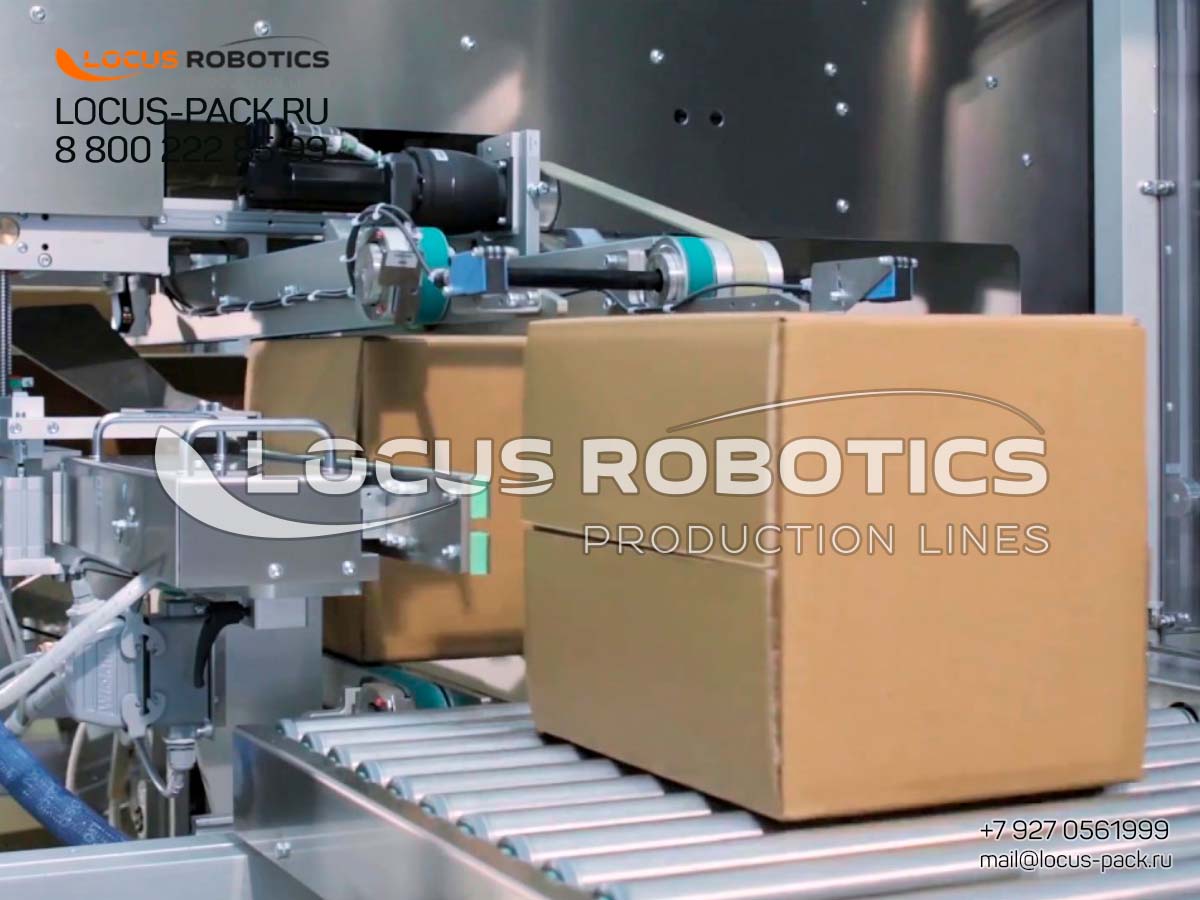
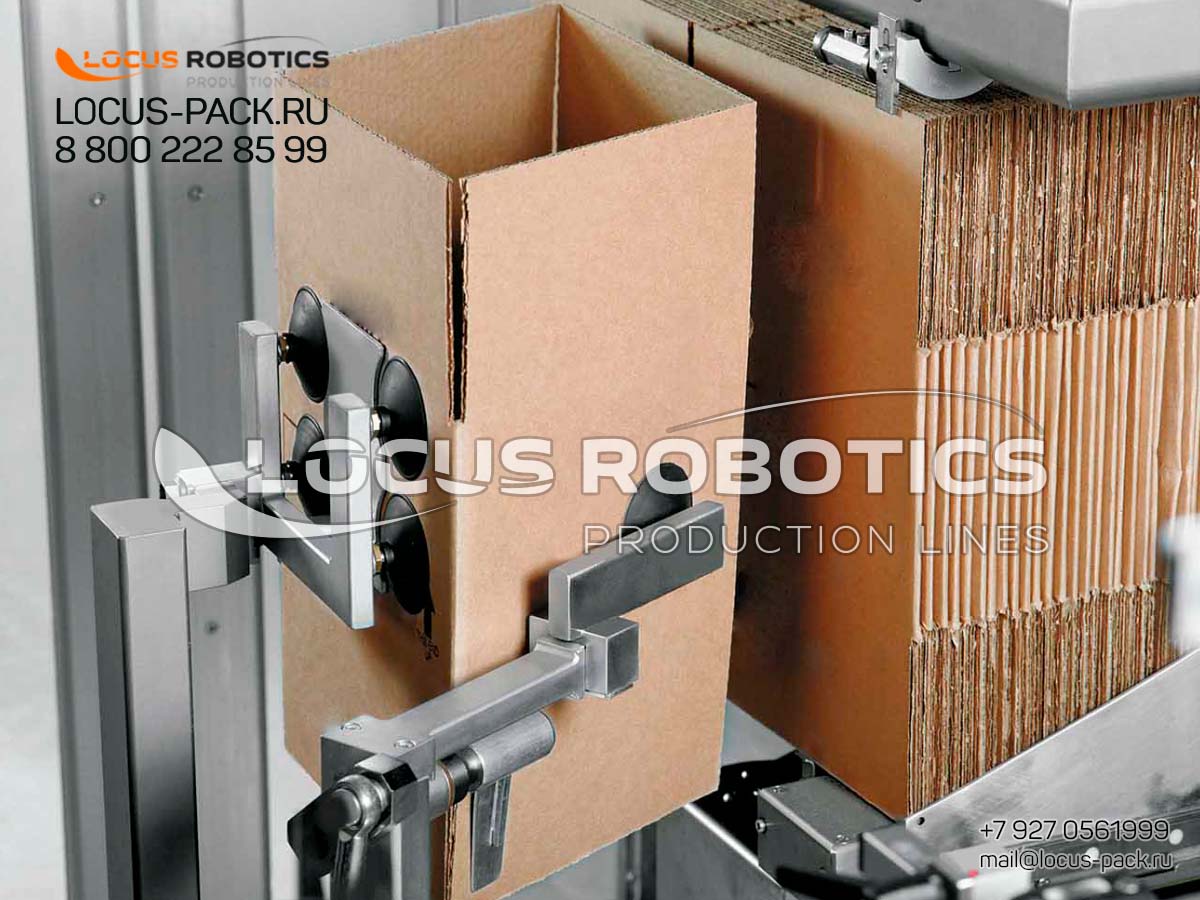
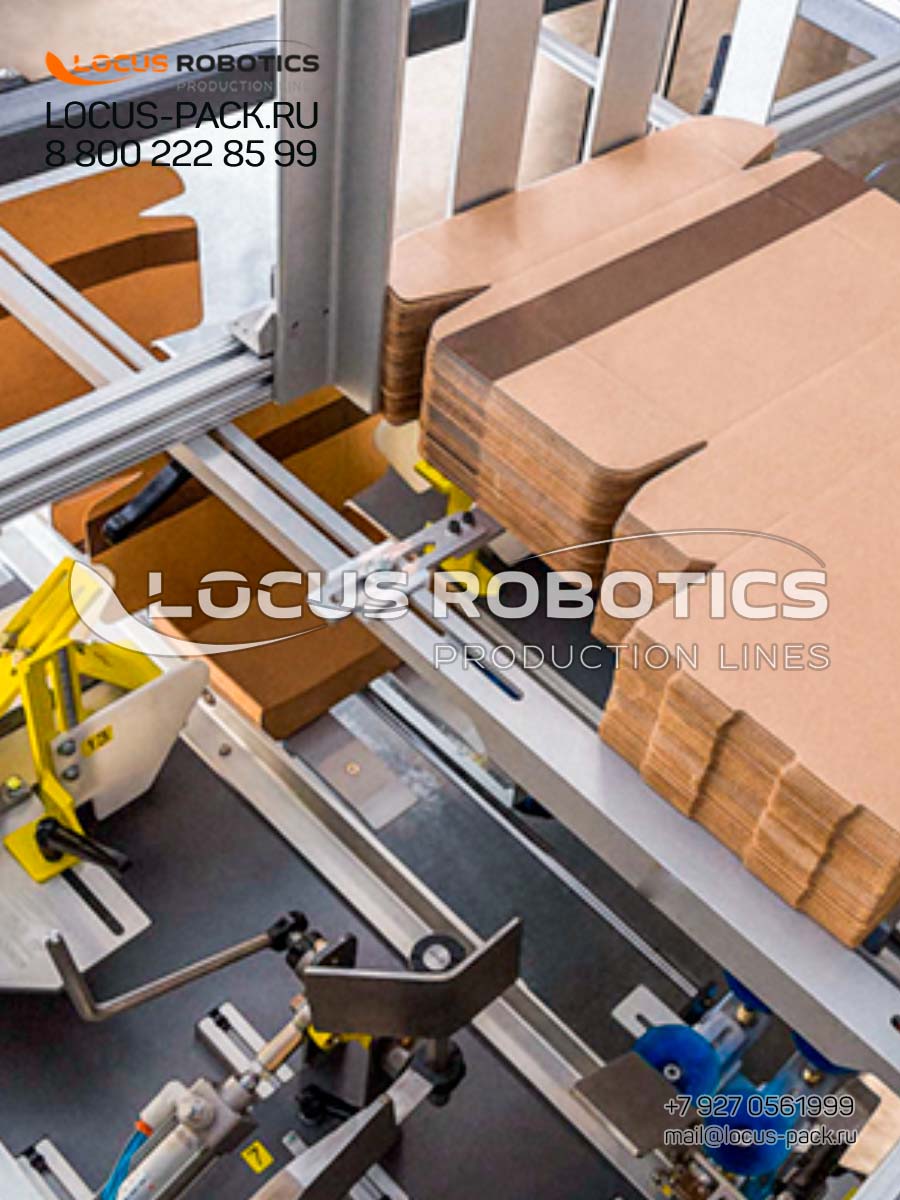
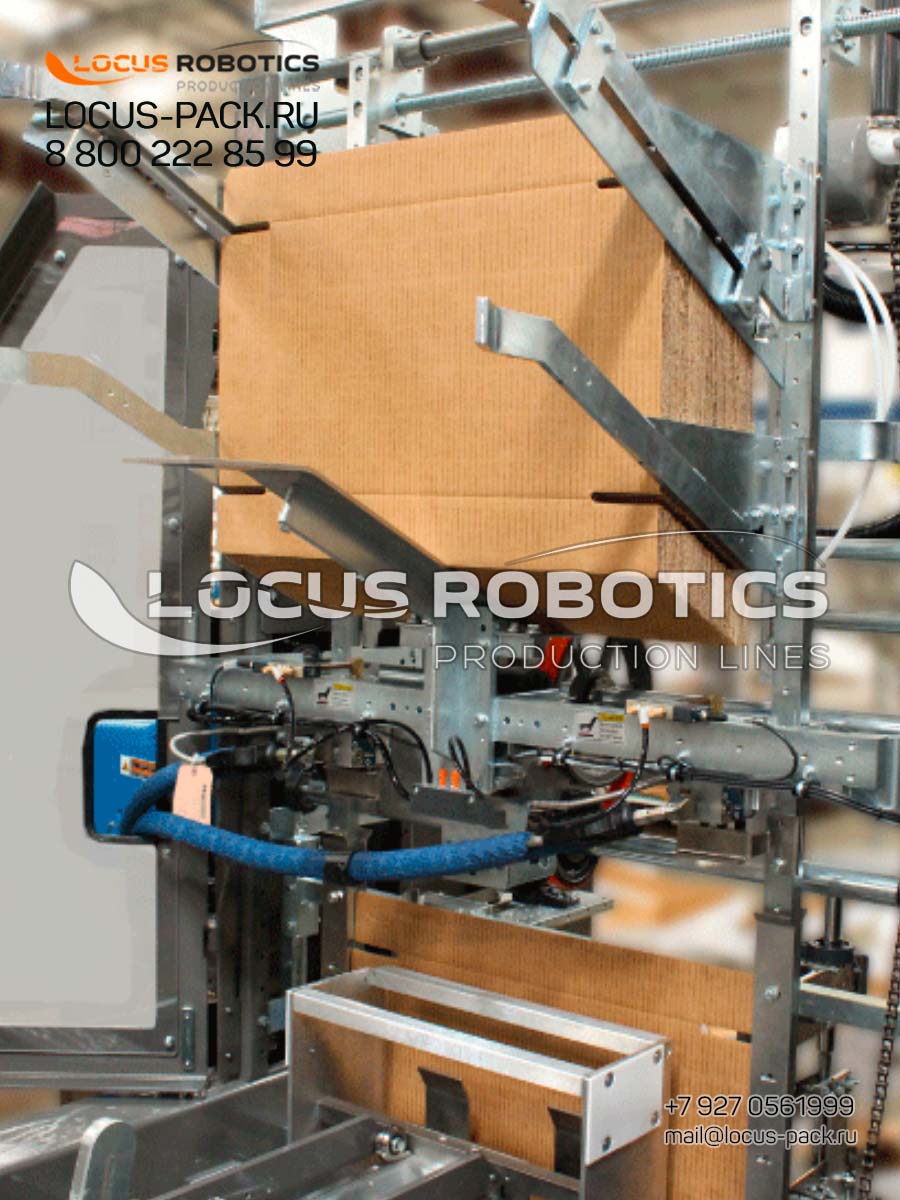
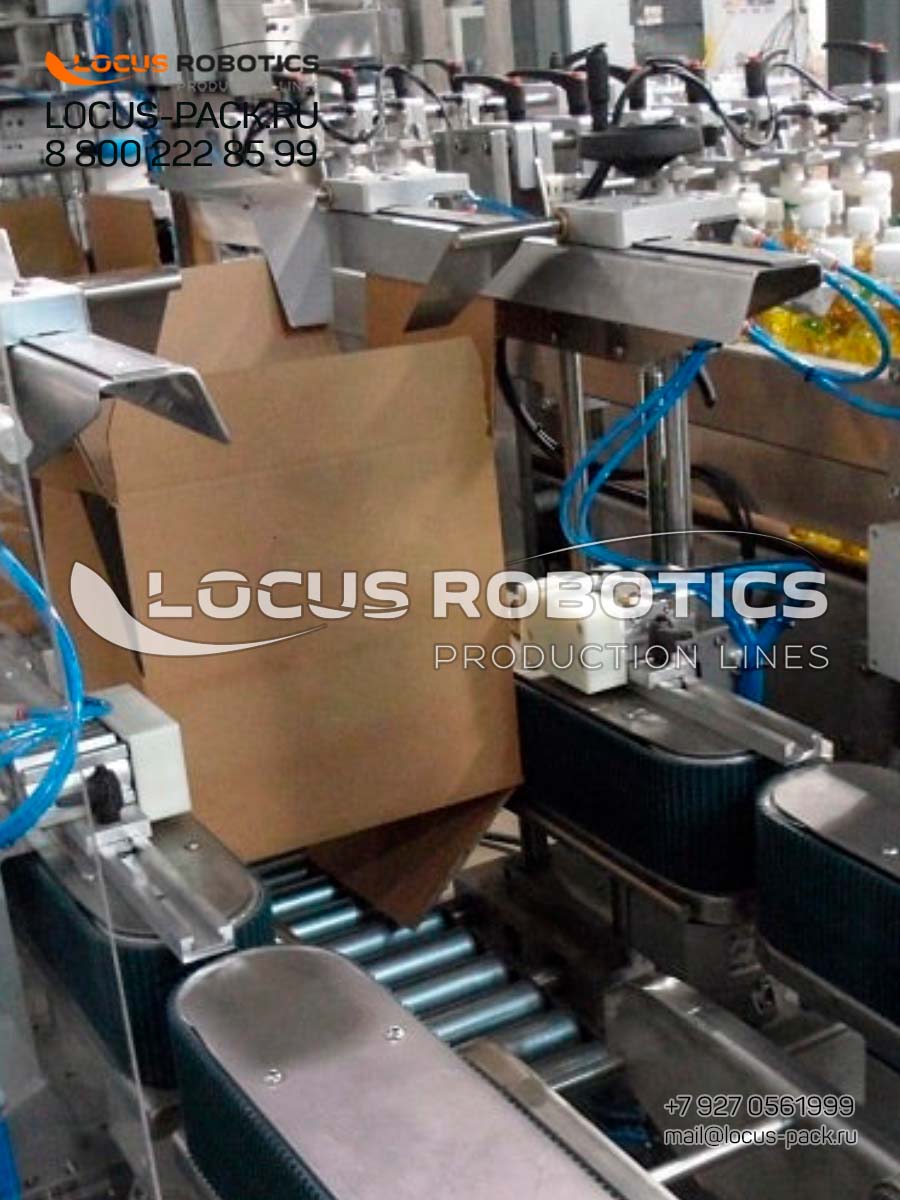
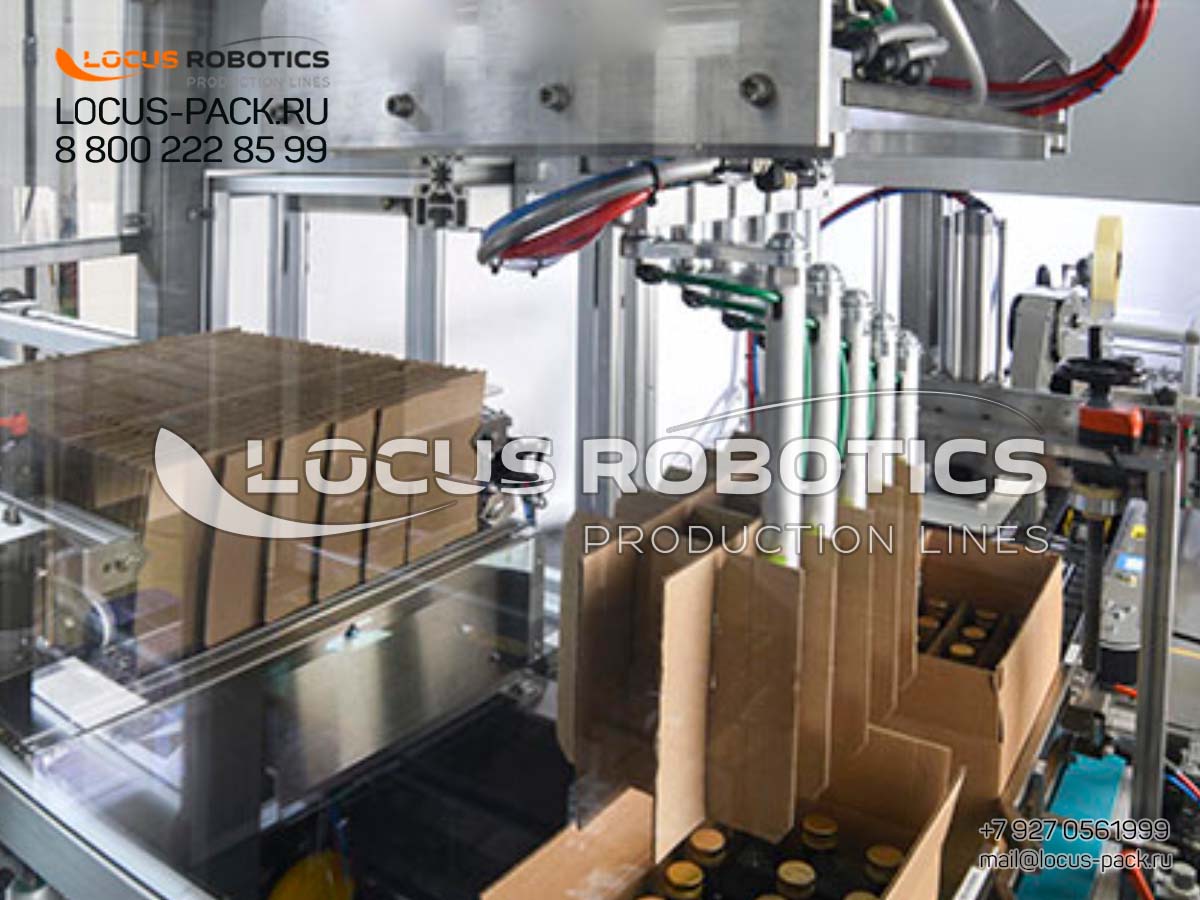
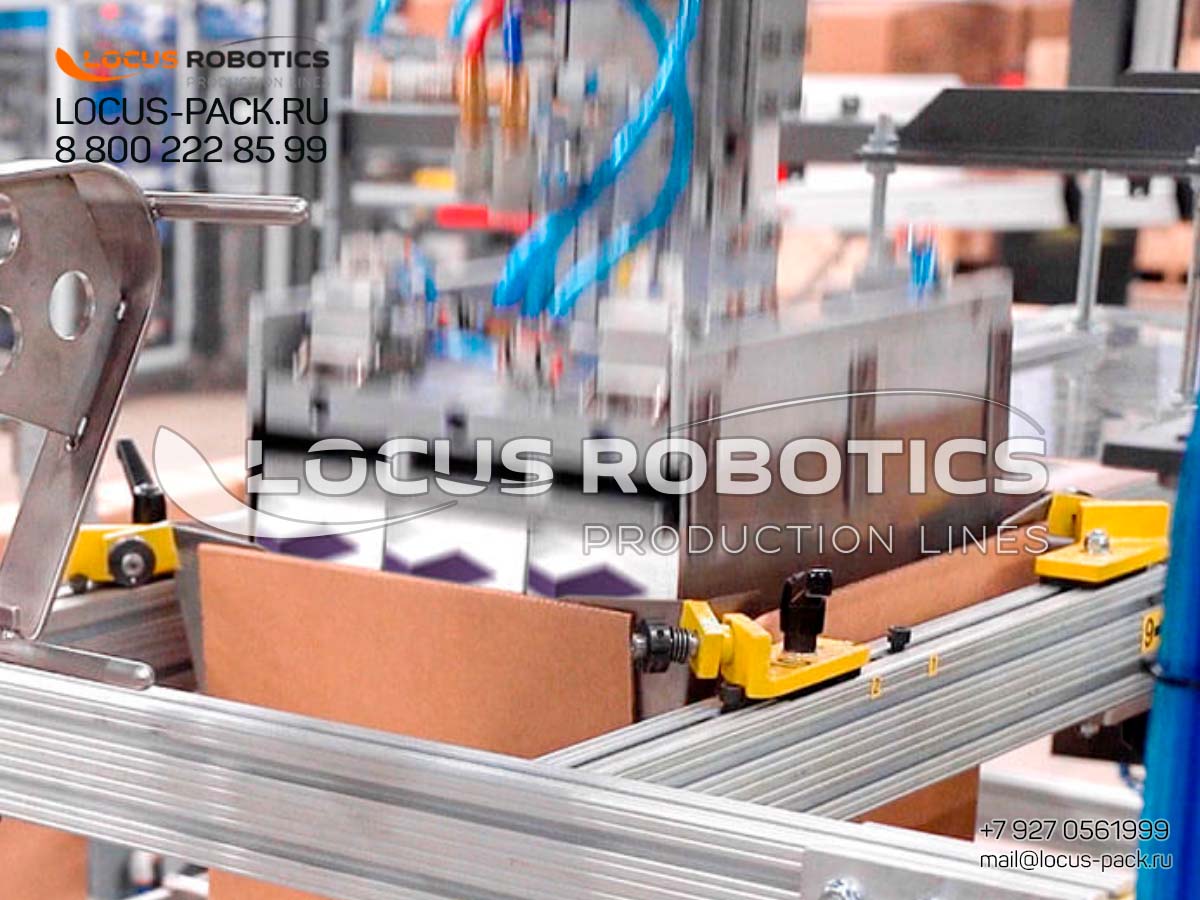
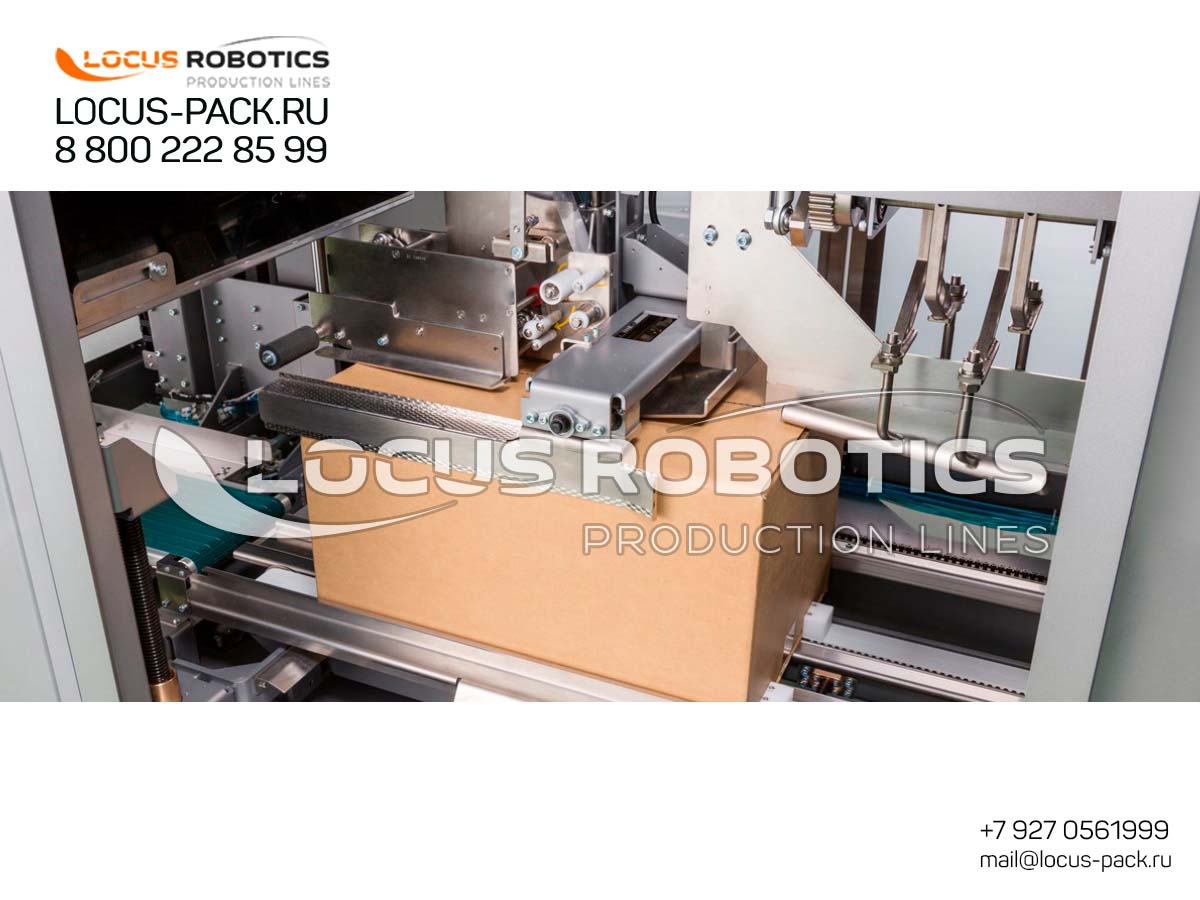
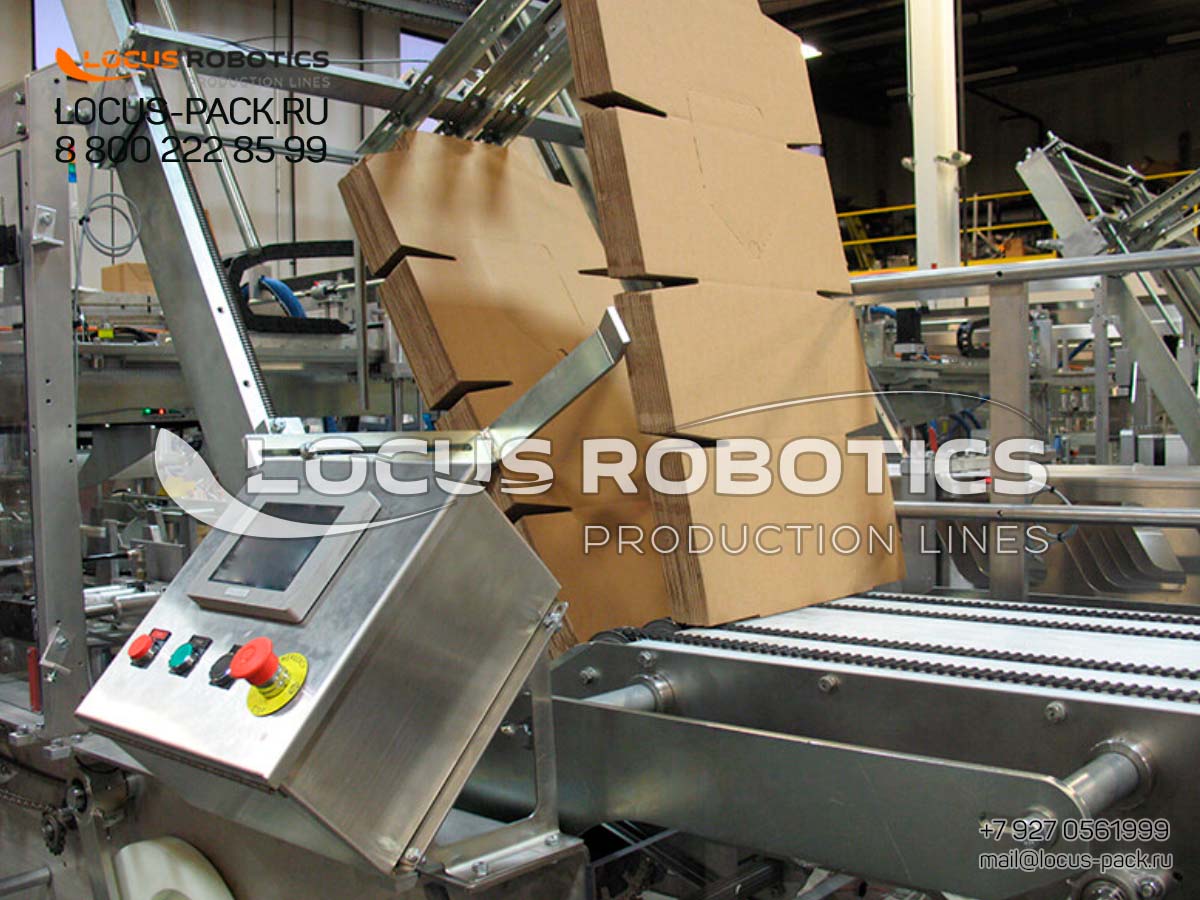
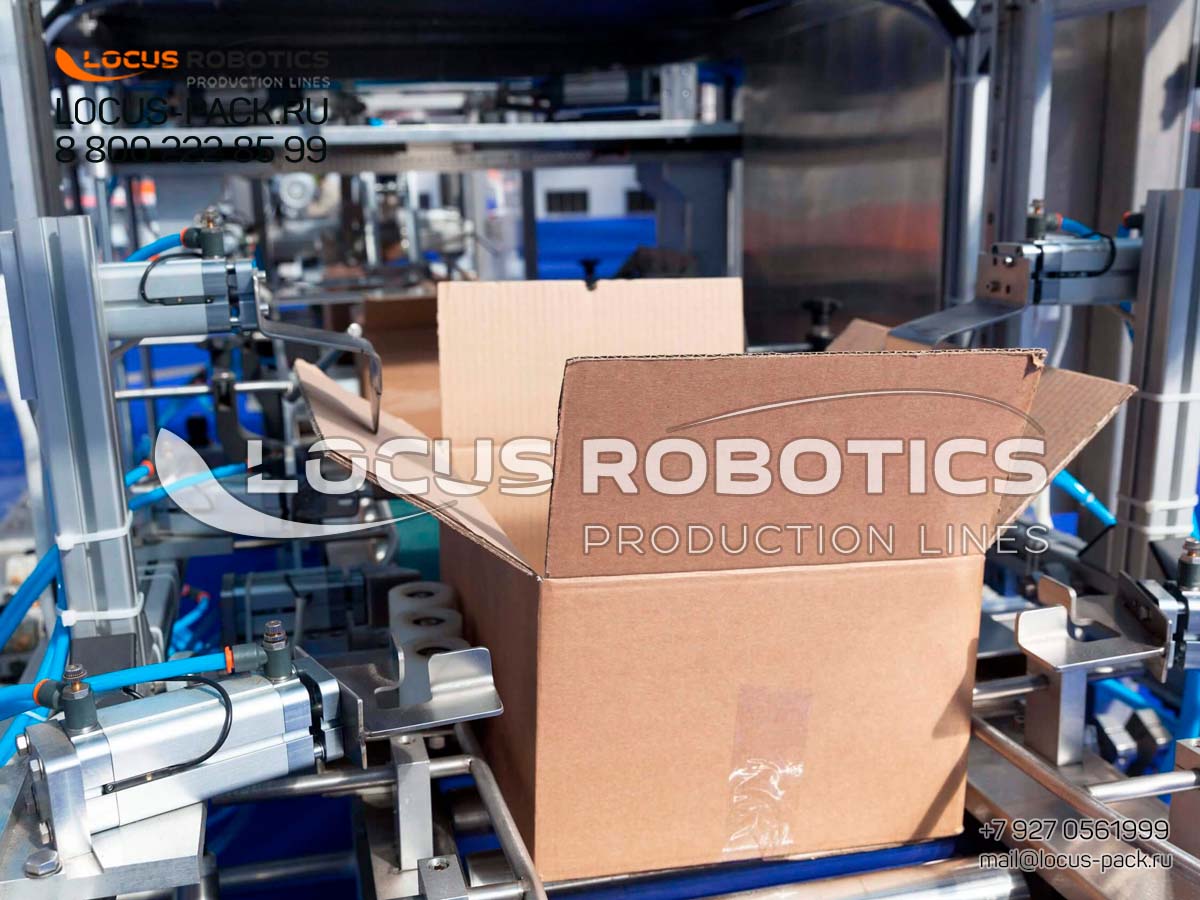
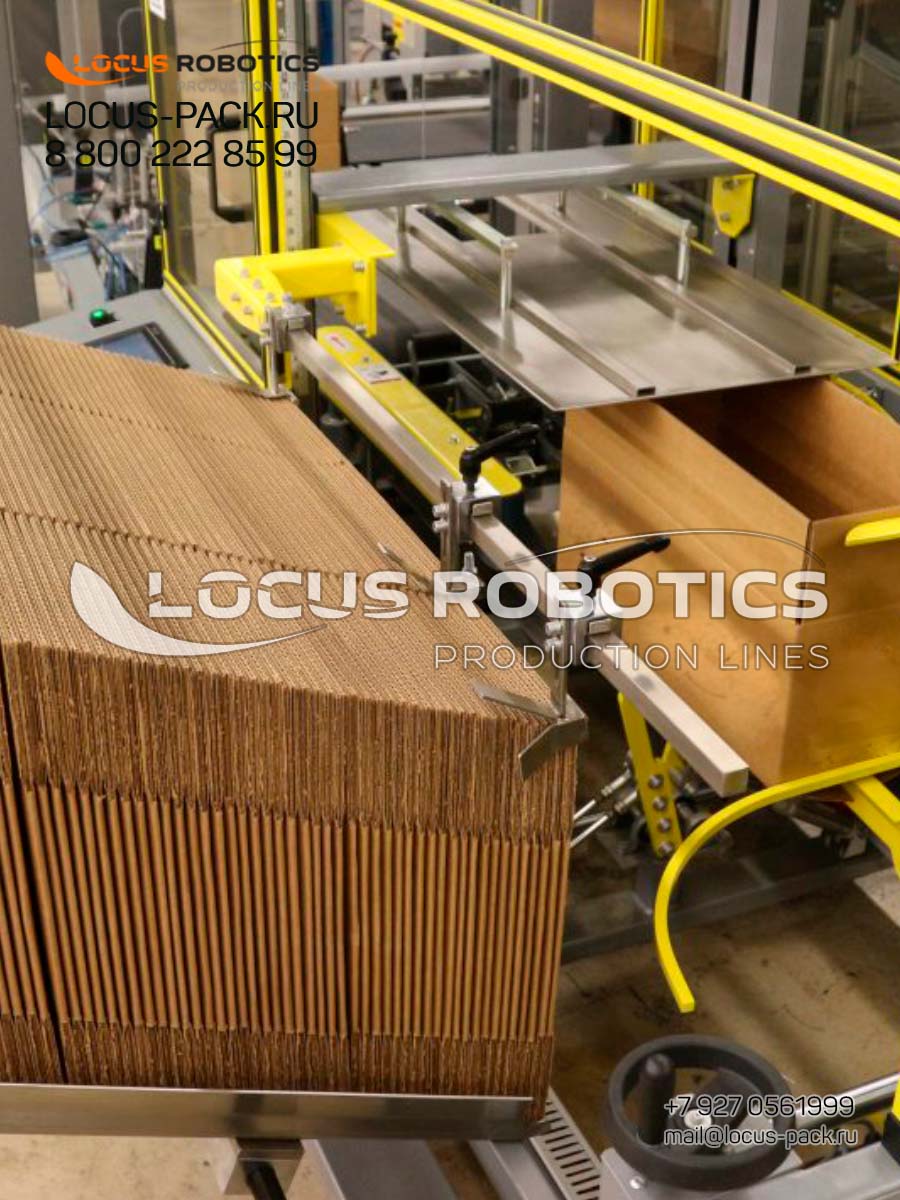
The LRCP-100 incorporates an advanced case erecting system that automatically forms flat corrugated blanks into ready-to-fill cases. This system includes:
-
Automatic case magazine that can hold significant quantities of flat blanks
-
Suction cup extraction system for precise case handling
-
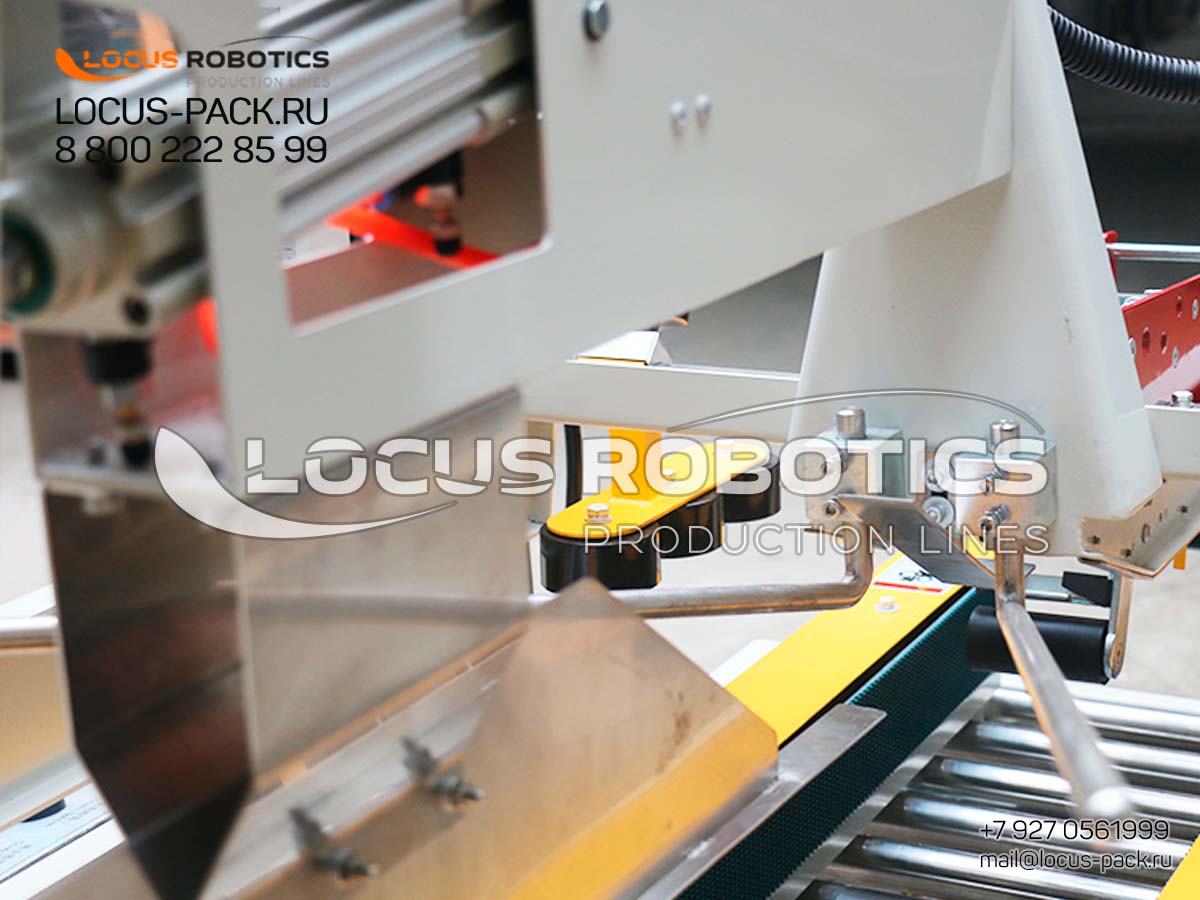
Bottom folding mechanisms for case formation
-
Automatic bottom sealing with hot melt adhesive or tape
The machine handles various case styles including Regular Slotted Containers (RSC), Half-Slotted Containers (HSC), and wrap-around cases, providing flexibility for different packaging requirements.
Precision Food Product Handling
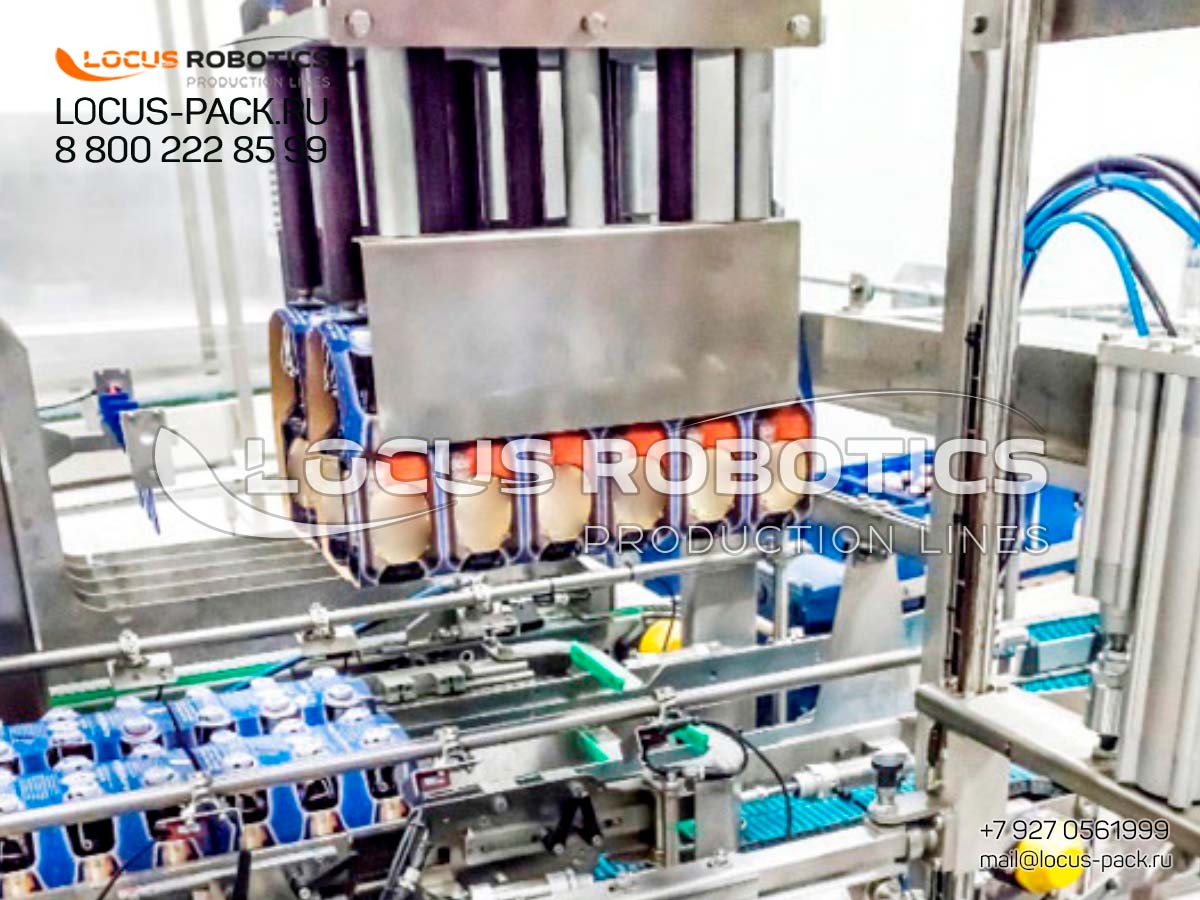
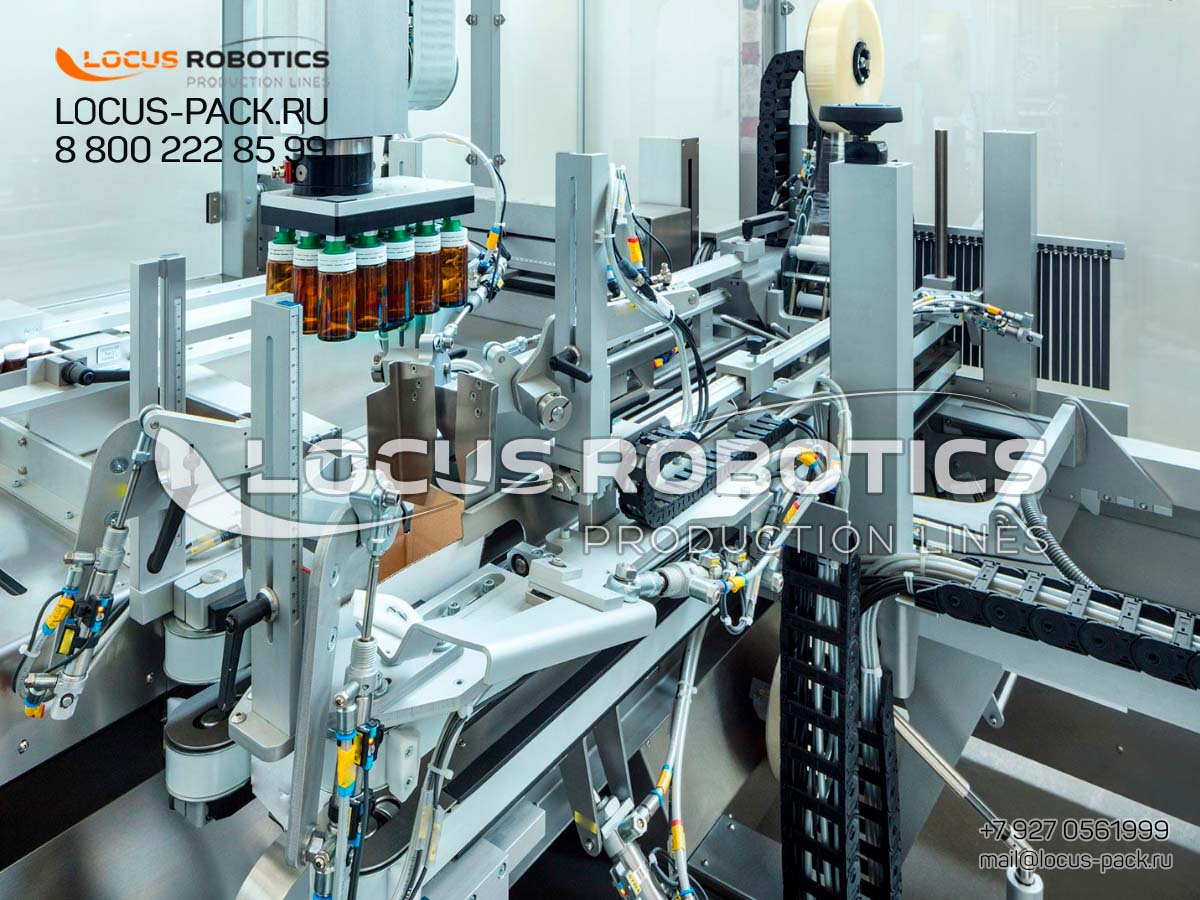
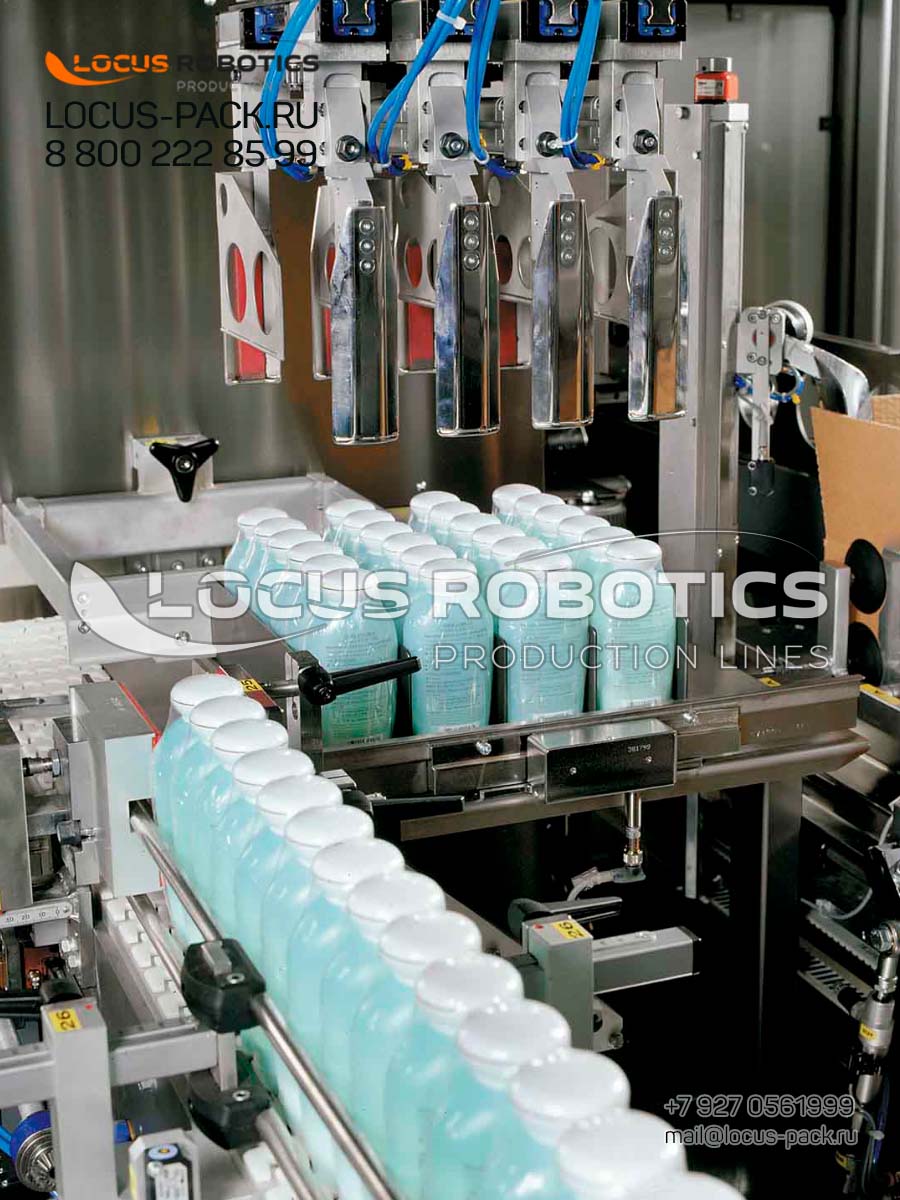
The LRCP-100 incorporates advanced product handling technology for accurate placement of food products into cases:
-
Gentle handling systems: Preventing product damage during transfer
-
Pattern formation capabilities: Creating optimal packing configurations
-
Vision systems: Ensuring correct product orientation and placement
-
Quick-change grippers: Adapting to different product sizes and shapes
The system achieves high positioning accuracy (typically ±0.5mm to ±1.0mm) as seen in equipment.
Applications & Industry Solutions
Food Industry Applications
The LRCP-100 is particularly suited for food packaging applications with its ability to handle various product types including:
-
Bakery products: Bread, pastries, and baked goods
-
Dairy products: Cheese, yogurt, and dairy-based products
-
Frozen foods: Vegetables, fruits, and prepared meals
-
Snack foods: Chips, crackers, and convenience foods
The system’s gentle handling ensures product integrity while the precise placement maintains package appearance throughout the distribution chain.
Quality Assurance & Compliance
Food product packaging requires strict quality control measures to ensure product safety and compliance with international standards. The LRCP-100 system incorporates several features to maintain quality:
-
Hygienic design: Easy cleaning and maintenance for food safety
-
Material compatibility: Food-grade materials throughout product contact surfaces
-
Quality verification: Systems to ensure proper packaging and sealing
-
Regulatory compliance: Meeting food safety standards and regulations
The system is designed to meet international certification requirements including FDA, EU food contact regulations, and various regional food safety standards, making it suitable for global deployment in food packaging operations.
Comparative Analysis with Similar Machines
TComparison with Similar Case Packing Systems
| Feature | LRCP-100 | competitor A | competitor B | competitor C |
|---|---|---|---|---|
| Packing Speed | 10-120 cases/min | 3-4 cases/min | High-speed | 1-5 cases/min |
| Special Feature | Lift mechanism | Pick and place technology | Gravity-based | PLC-controlled |
| Automation Level | Fully automatic | Fully automatic | Fully automatic | PLC-controlled |
| Industry Focus | Food products | General packaging | Flexible packages | Food, medical |
Operational Benefits and ROI Considerations
Production Efficiency
The LRCP-100 offers significant operational benefits:
-
Labor reduction: Automation reduces manual packing requirements
-
Increased throughput: High-speed operation boosts production capacity
-
Consistent quality: Automated systems ensure uniform packaging
-
Space optimization: Compact design maximizes floor space utilization
Economic Considerations
The machine offers favorable return on investment through:
-
Reduced product damage: Gentle handling minimizes losses
-
Lower labor costs: Automation reduces manual labor requirements
-
Material optimization: Efficient packing reduces material usage
-
Improved uptime: Reliable operation reduces downtime
Implementation and Support Considerations
Integration Requirements
Implementing the LRCP-100 would require:
-
Factory space assessment: Ensuring adequate space and utilities
-
Existing line integration: Connecting with upstream and downstream equipment
-
Operator training: Ensuring staff competency with the new system
-
Maintenance planning: Establishing preventive maintenance routines
Support and Service
The LRCP-100 comes with:
-
Comprehensive warranty: Typically 12 months or more
-
Technical support: Remote and on-site assistance
-
Spare parts availability: Ensuring minimal downtime
-
Training programs: For operators and maintenance staff
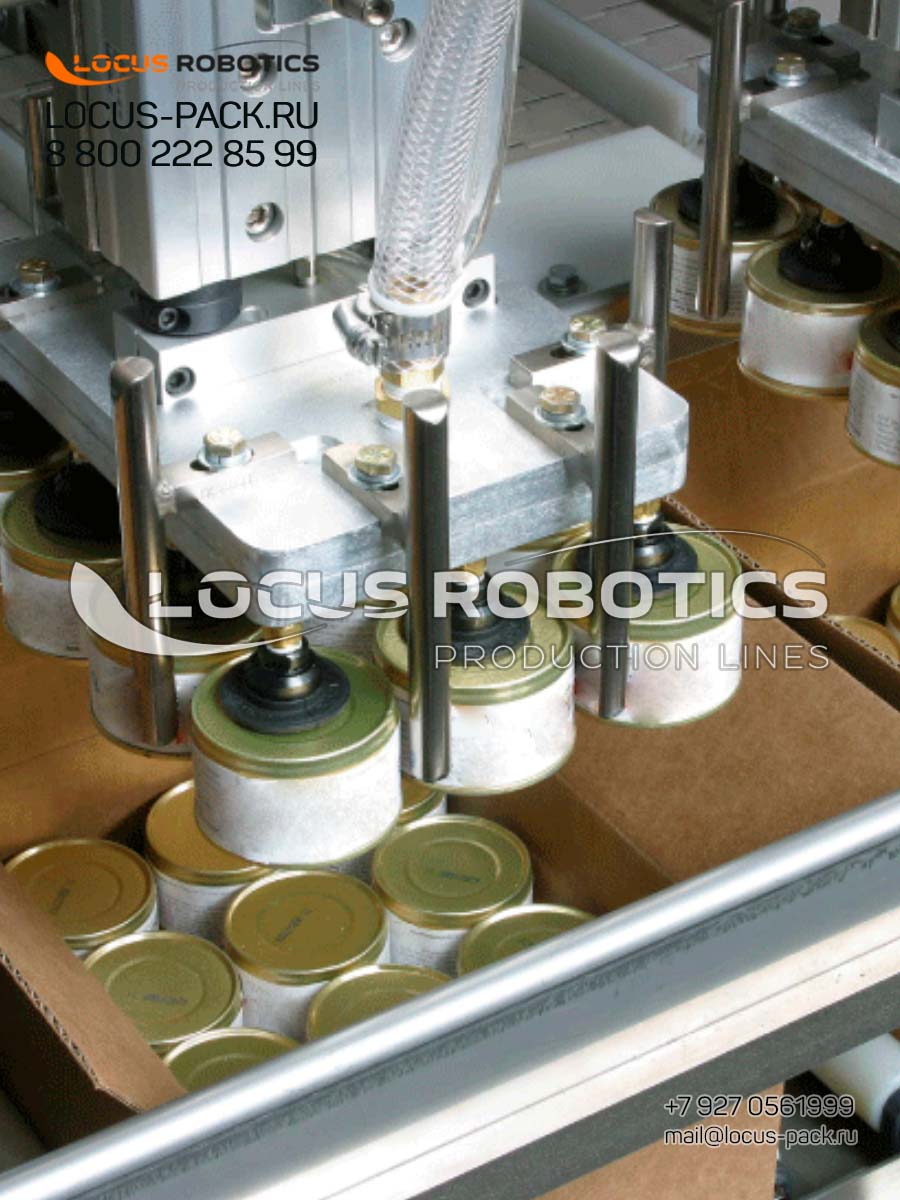
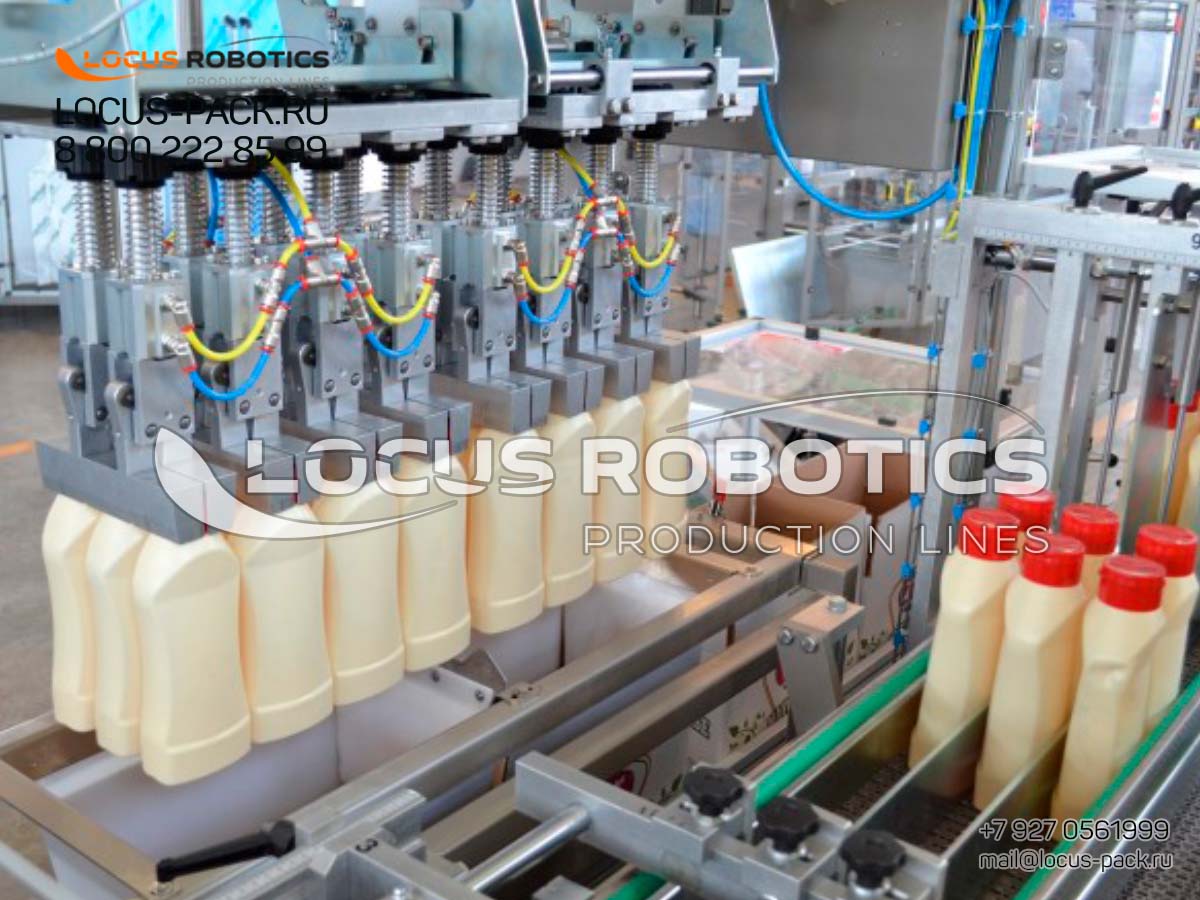
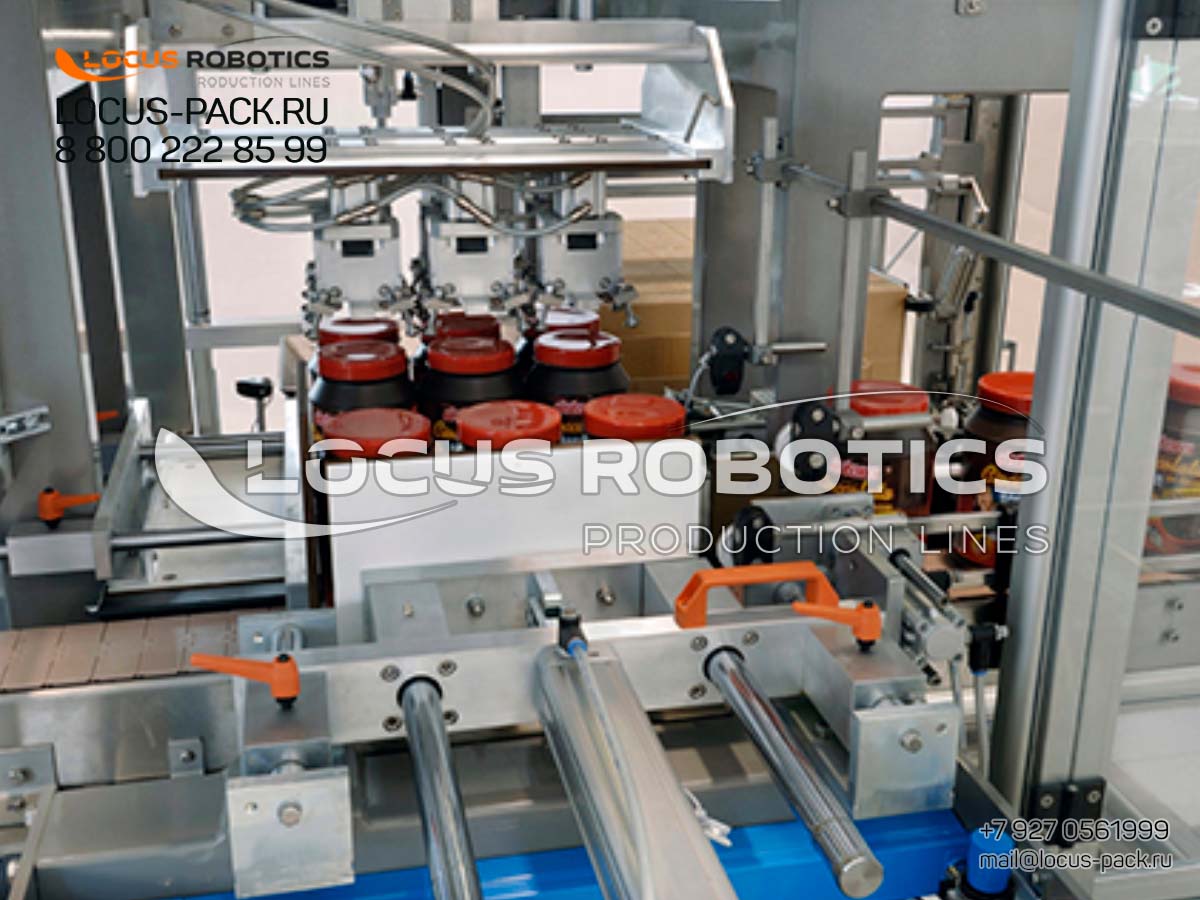
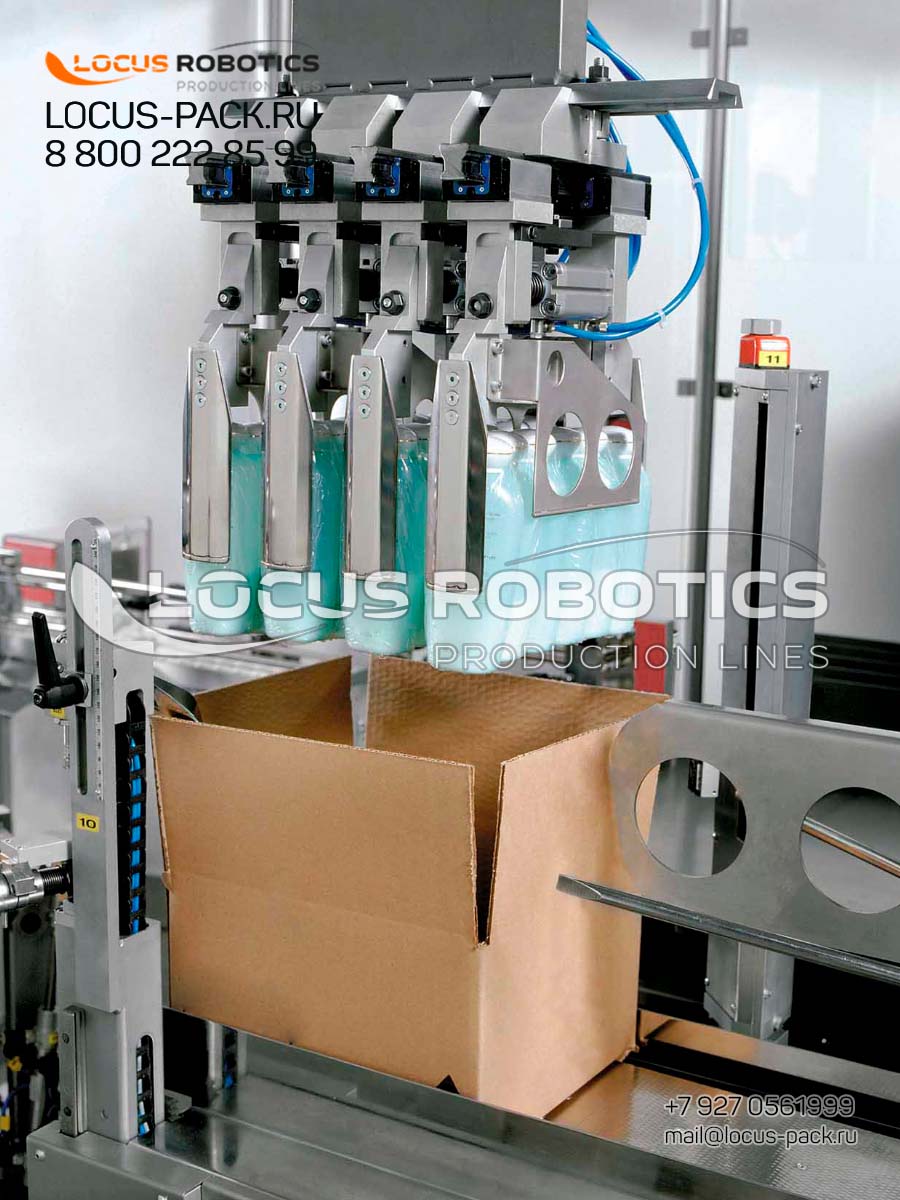
The Automatic Case Packer LRC-100 is a fully automated packaging system designed for high-speed bottling lines. This advanced machinery performs three primary functions: automatic case erection, precise bottle loading using mobile gripper technology, and secure case sealing. The system integrates seamlessly between labeling/packaging equipment and palletizers, eliminating the need for manual operators while ensuring consistent packaging quality and efficiency.
Key Features & Technical Specifications
| Parameter | Specification |
|---|---|
| Production Capacity | 20-120 cases/minute (depending on configuration) |
| Bottle Compatibility | Various glass and plastic containers |
| Case Formats | RSC, HSC, wrap-around styles |
| Gripper System | Adaptive mobile grippers with vacuum technology |
| Integration Position | After labeling/cartoning machines |
| Output Connection | Direct to palletizers |
| Control System | PLC with HMI touchscreen interface |
| Construction | Stainless steel (304/316L) with food-grade coatings |
Core Functions
-
Automatic Case Erection
-
Forms flat corrugated blanks into ready-to-fill boxes
-
Handles various case sizes from 200x100x100mm to 600x400x400mm
-
Automatic bottom sealing with hot melt adhesive
-
-
Precision Bottle Loading
-
Mobile gripper systems with vacuum technology
-
Gentle handling to prevent bottle damage (±0.5mm accuracy)
-
Pattern formation capabilities for optimal case utilization
-
Quick-changeover system (<5 minutes for format changes)
-
-
Automatic Case Sealing
-
Top flap closure and sealing
-
Hot melt adhesive or tape sealing options
-
Secure closure for transportation
-
Integration & Compatibility
-
Upstream Equipment: Labeling machines, cartoners, packaging systems
-
Downstream Connectivity: Palletizers, wrapping systems (500-1200mm height adjustment)
-
Line Synchronization: Maintains consistent flow with production speeds
-
Flexible Layout: Adaptable to existing production line configurations
The LRCP-100 automatic case packer with lift mechanism represents a specialized solution for food producers seeking to enhance their packaging capabilities while maintaining efficient product handling. The system’s robust construction, hygienic design, and lift mechanism make it particularly suitable for food production facilities where product handling efficiency and food safety are critical considerations.
Operational Benefits
-
Labor Reduction: Eliminates 2-3 manual operators per shift
-
Increased Efficiency: 99.5% operational efficiency with minimal downtime
-
Consistent Quality: Automated precision ensures uniform packaging
-
Space Optimization: Compact design (3000x2000x1800mm) minimizes floor space
-
Quick Changeover: Rapid adjustment between different formats
Technical Details
-
Power Supply: 380V/50Hz/3PH (alternative voltages available)
-
Air Consumption: 0.6-0.8 MPa, 100 L/min
-
Machine Weight: 1200-1500 kg (depending on configuration)
-
Noise Level: <75 dB during operation
This advanced case packing solution represents cutting-edge automation technology, offering beverage producers complete packaging automation while eliminating manual labor costs and ensuring consistent packaging quality. The system’s robust construction and flexible design make it ideal for high-speed production environments requiring reliable secondary packaging solutions.
By implementing this technology, producers can achieve higher throughput, improved package quality, and reduced operational costs while maintaining flexibility in their packaging operations. The integrated lift mechanism adds significant value by addressing specific product handling needs that may not be adequately met by traditional case packing systems.
For specific technical specifications and pricing information, direct consultation with Locuspack would be recommended to ensure the system meets particular production requirements and integration needs.
Automatic Case Packer LRCP-100.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.