Description
RC-100 High-Speed Rotary Monoblock for Chemical and Aggressive Liquid Packaging
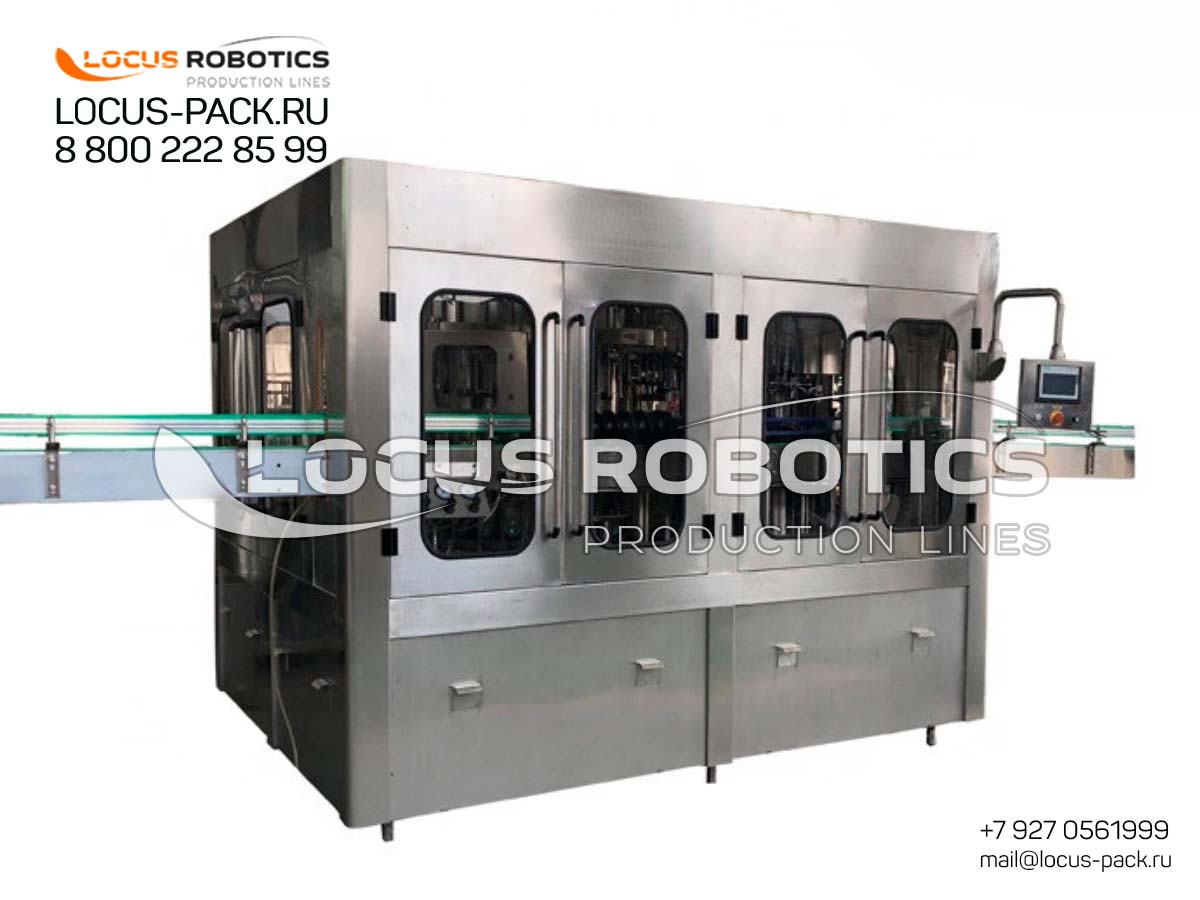
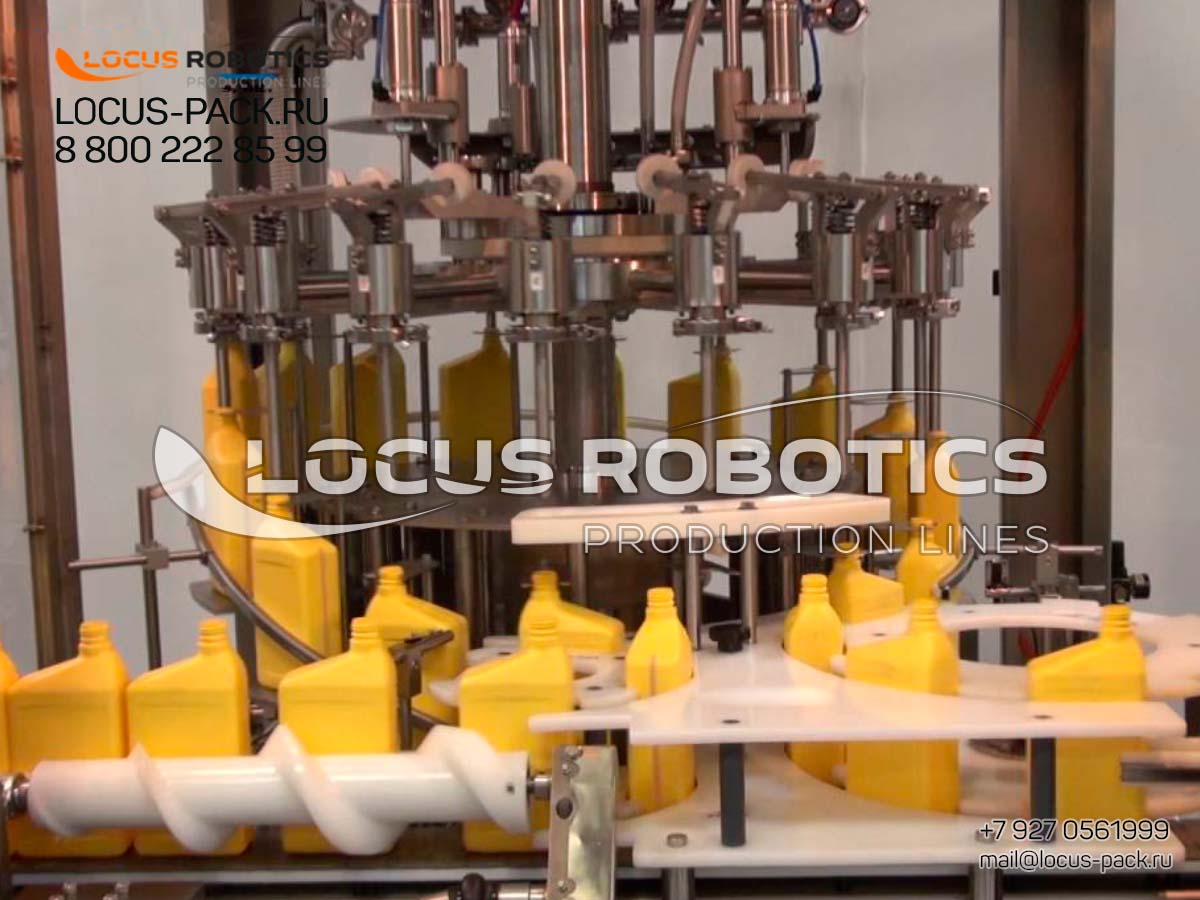
Industrial Monoblock with protective guarding and vapor extraction hood, filling corrosive chemicals into large HDPE containers.
Integrated Process: Rinsing, Precision Dosing, and Secure Capping.
Engineered for Reliability with Aggressive and Hazardous Products.
The RC-100 is a high-speed rotary monoblock engineered for the rapid and reliable packaging of a wide range of chemical products, including aggressive solvents, acids, cleaners, and detergents into plastic containers and jerry cans. Its robust construction, featuring a rotary bottle rinser, precision rotary dosing pump, and rotary capper, is built to withstand harsh industrial environments. The machine includes full protective guarding for operator safety, a plate conveyor for stable container handling, and programmable logic control (PLC) for effortless operation and quick changeover between products. Achieve exceptional output of over 5,000 containers per hour without compromising on accuracy or safety.
Corrosion-Resistant Construction: Built with 316L stainless steel, PTFE, and EPDM seals to resist the harshest chemicals.
Enhanced Safety: Options include full protective guarding, integrated fume extraction, and explosion-proof (ATEX) rated components.
Precision Dosing: Piston filler ensures accurate volume control, minimizing waste of expensive or hazardous products.
Global Compliance: Designed to meet international standards for safety and hazardous material handling.
Engineered for the Most Demanding Industrial Environments
Standard packaging equipment fails when faced with aggressive chemicals. The RC-100 is built from the ground up for these extreme applications. It is the reliable solution for industries where product integrity, operator safety, and equipment durability are non-negotiable. By integrating rinsing, filling, and capping into a single, sealed platform, it minimizes exposure points, contains vapors, and provides a controlled environment for packaging the world’s most challenging liquids.
Safe and Contained Handling of Aggressive Liquids
The monoblock is designed around the principle of containment and resistance:
-
Container Rinsing (Optional): An initial purge with inert gas or air ensures containers are free of contaminants.
-
Precision Filling: A sealed piston filler, constructed with chemically inert materials, accurately doses the product without leakage or exposure.
-
Secure Capping: Torque-controlled capping heads apply closures securely to prevent leaks during storage and transport.
Technical Specifications & Safety Features
-
Model: RC-100
-
Type: Industrial-Grade Monoblock
-
Process: Rinsing, Filling, Capping (for aggressive products)
-
Applications: Acids (e.g., HCl, H2SO4), Solvents, Caustics (e.g., NaOH), Pesticides, Herbicides, Concentrated Cleaners, Agrochemicals.
-
Construction Material: 316L Stainless Steel (standard), Hastelloy options available. Seals made from PTFE, EPDM, Viton.
-
Filling System: Sealed Piston Filler
-
Filling Accuracy: ≤ ±0.5% (critical for costly/ hazardous chemicals)
-
-
Safety Options:
-
Vapor Extraction Hood: Contains and removes toxic fumes.
-
Explosion-Proof Rating: ATEX-certified motors and components for flammable solvents.
-
Full Protective Guarding: Protects operators from splashes and mechanical hazards.
-
Drip Trays & Containment: Secondary containment for spills.
-
-
Power Supply: 380V/50Hz/3Ph (Explosion-proof configurable)
-
Control System: PLC with Touchscreen HMI, often with remote mounting option for safe operation outside hazardous areas.
Built to Withstand Acids, Solvents, and Toxic Chemicals
-
Chemical Resistance: The use of 316L SS provides excellent resistance to a wide range of corrosives. For extreme acids, Hastelloy C-22 options are available.
-
Seal Integrity: Specialty seals are selected based on the chemical being packaged to prevent degradation and failure.
-
Durability: The entire system is built with a heavier gauge of metal and hardened components to withstand the rigors of an industrial chemical plant.
Compliance and Safety for Hazardous Material Handling
This machine is not just built for performance; it’s built for compliance. Its design helps manufacturers meet stringent international safety regulations (OSHA, EPA, REACH) for handling hazardous materials. The optional features like vapor extraction and explosion-proofing are not luxuries but necessities for responsible and legal operation in many industries and regions.
-
Industrial-Grade Construction: Built with corrosion-resistant materials and components to handle aggressive chemistry.
-
High-Speed Operation: Rotary design delivers outputs exceeding 5,000 bottles per hour.
-
Complete Process Integration: Performs rinsing, filling, and capping on a single platform.
-
Enhanced Safety: Includes protective guarding and is compatible with optional vapor extraction systems.
High-Throughput Packaging for Demanding Chemical Applications
In the chemical industry, efficiency and equipment durability are paramount. The RC-100 High-Speed Rotary Monoblock is designed to meet the rigorous demands of packaging everything from household cleaners to industrial-strength acids and solvents. Its rotary platform ensures continuous, high-volume operation, maximizing productivity for large-scale manufacturers. The machine’s design focuses on minimizing downtime and maximizing uptime, providing a rapid return on investment for high-volume production facilities.
Integrated Process: Rinsing, Precision Dosing, and Secure Capping
The RC-100 streamlines the packaging process into one seamless operation:
-
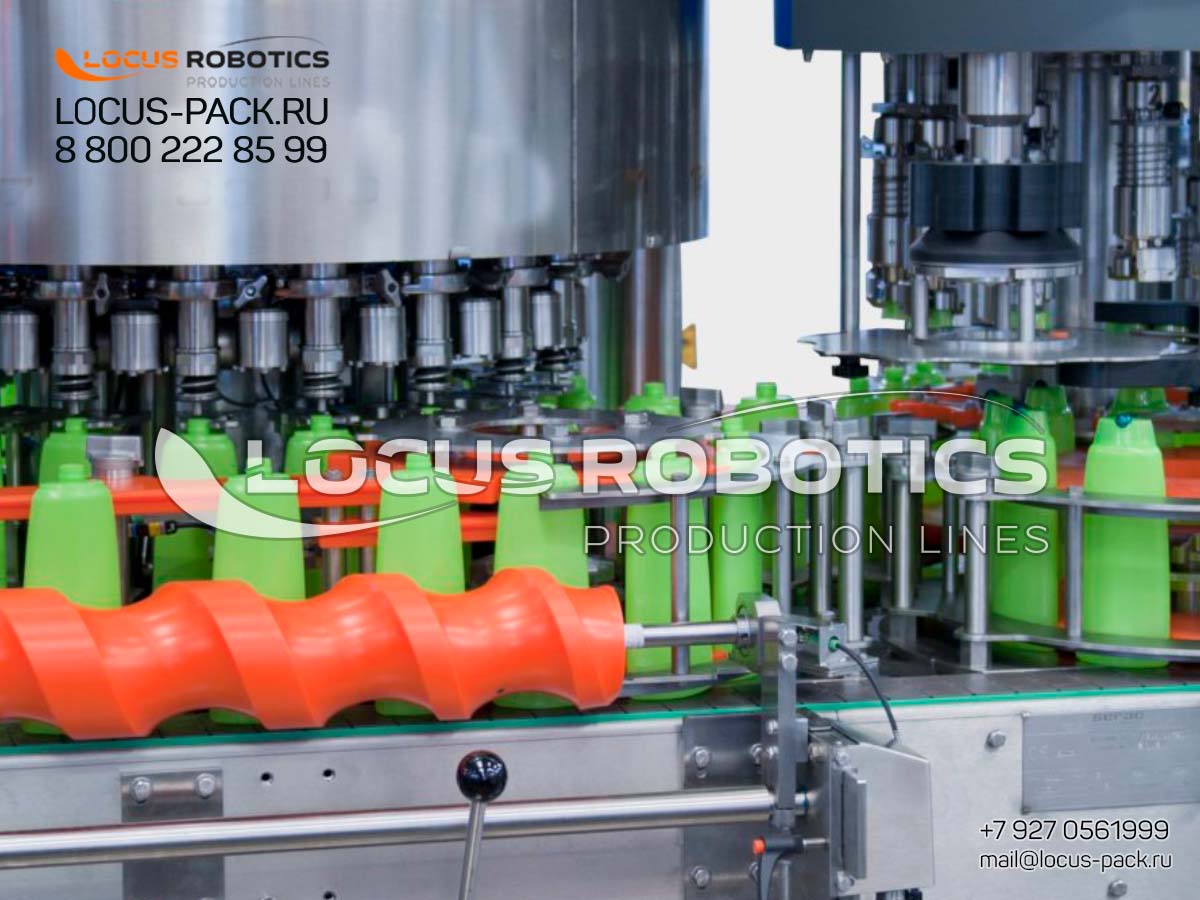
Rotary Rinsing: Containers are fed into the system and undergo a high-speed internal rinsing cycle with air or an inert gas to remove any particulate contaminants before filling.
-
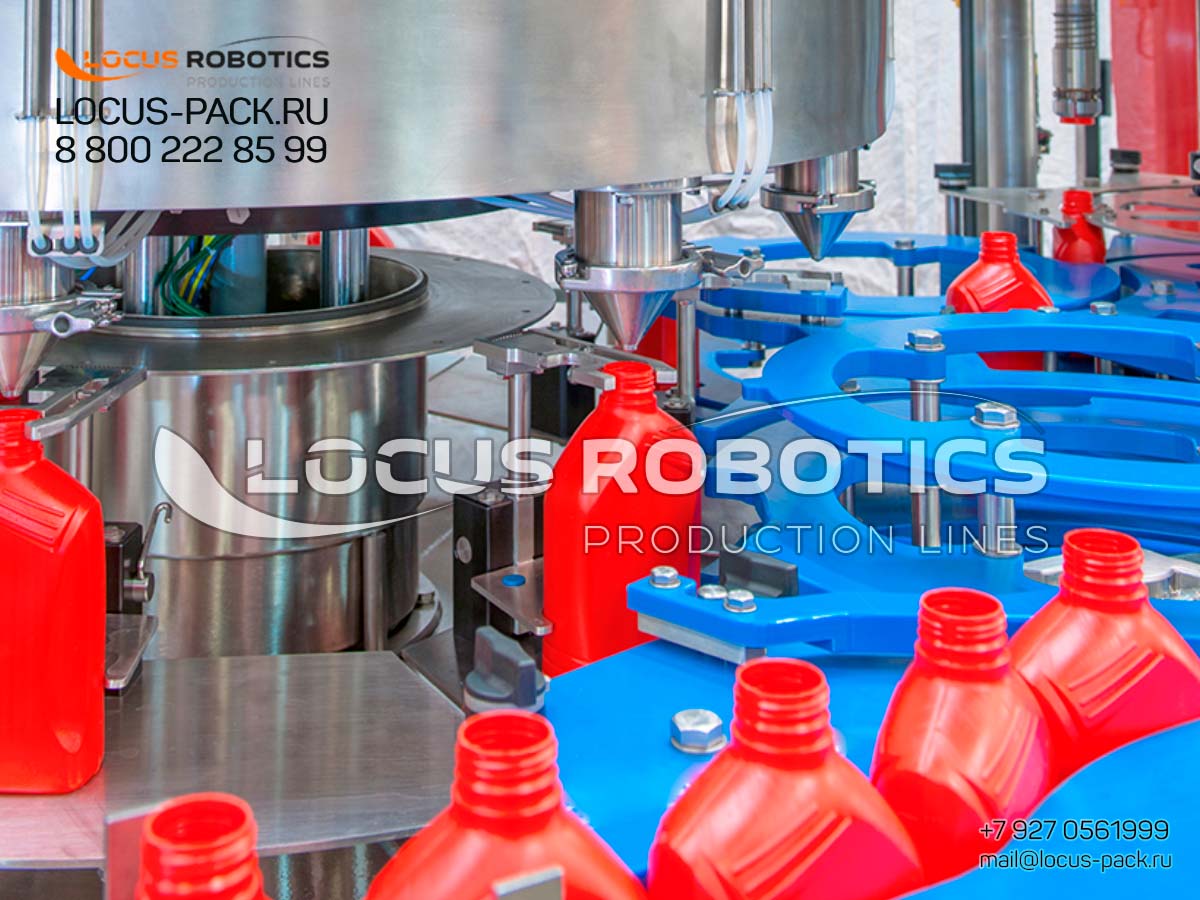
Rotary Precision Dosing: A rotary piston filler or specialized chemical pump accurately meters the product into each container. This is critical for minimizing giveaway of expensive chemicals and ensuring consistent fill volumes.
-
Rotary Capping: A rotary capper applies screw caps or closures with consistent torque, ensuring a leak-proof and secure seal that is vital for the safe transport of hazardous materials.
Technical Specifications & Construction Details
-
Model: RC-100
-
Type: High-Speed Rotary Monoblock
-
Functions: Rinsing, Filling, Capping
-
Speed: Up to 5,000+ containers per hour
-
Container Types: Plastic bottles, HDPE jerry cans, plastic containers (100ml — 5L)
-
Filling System: Rotary Piston Filler or Chemical Diaphragm Pump
-
Filling Accuracy: ≤ ±0.5% (dependent on product viscosity)
-
-
Capping System: Rotary Chuck Capper with adjustable torque control
-
Conveying System: Stainless Steel Plate Conveyor
-
Construction Materials: 316L Stainless Steel, PTFE, EPDM, Viton (standard on wetted parts)
-
Safety: Full protective guarding, emergency stop buttons
-
Control System: PLC with Touchscreen HMI for intuitive operation and recipe storage
Engineered for Reliability with Aggressive and Hazardous Products
This isn’t a standard food-grade machine. The RC-100 is built with components selected specifically for chemical resistance:
-
Seals & Gaskets: Made from PTFE, EPDM, or Viton to resist degradation from solvents, oils, and acids.
-
Surface Finishes: Electropolished stainless steel surfaces prevent corrosion and allow for easy cleaning.
-
Durability: Heavy-duty construction throughout to handle the day-to-day demands of an industrial chemical plant.
Safety and Containment Features for Industrial Environments
Operator safety is integrated into the design. The full protective guarding prevents accidental contact with moving parts. The machine can be easily integrated with optional peripherals such as:
-
Vapor Extraction Systems: To remove harmful fumes from the operator’s environment.
-
Drip Trays and Containment Sumps: To capture any accidental spills or leaks.
-
Explosion-Proof (ATEX) Components: For use with flammable solvents and liquids.
Unmatched Speed and Durability for Industrial Chemical Packaging.
Engineered for the Most Demanding Industrial Environments.
Safe and Contained Handling of Aggressive Liquids.
Built to Withstand Acids, Solvents, and Toxic Chemicals.
Compliance and Safety for Hazardous Material Handling.
High-Throughput Packaging for Demanding Chemical Applications.
Safety and Containment Features for Industrial Environments.
RC-100 Heavy-Duty Monoblock for Filling Aggressive, Corrosive, and Hazardous Products.
RC-100 Industrial Monoblock for Filling Aggressive and Corrosive Chemicals.
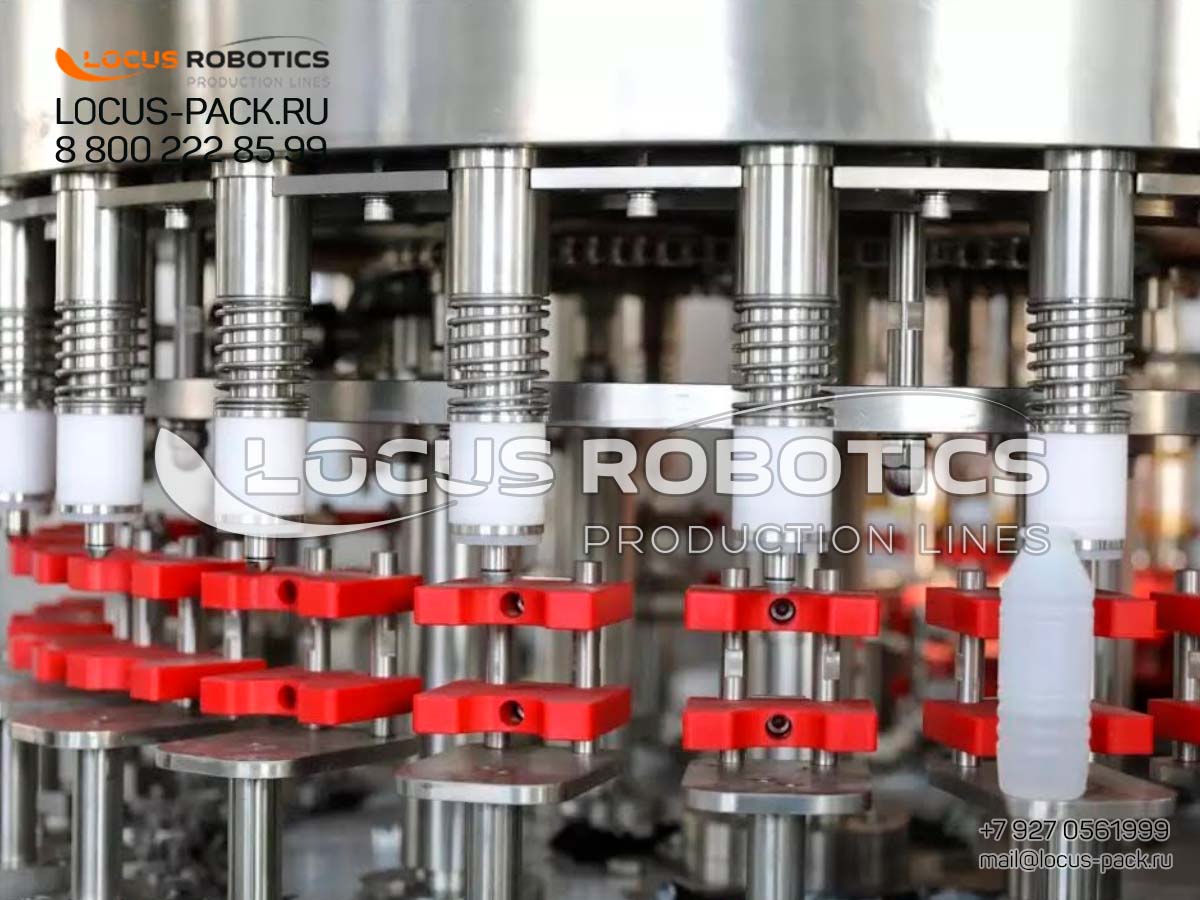
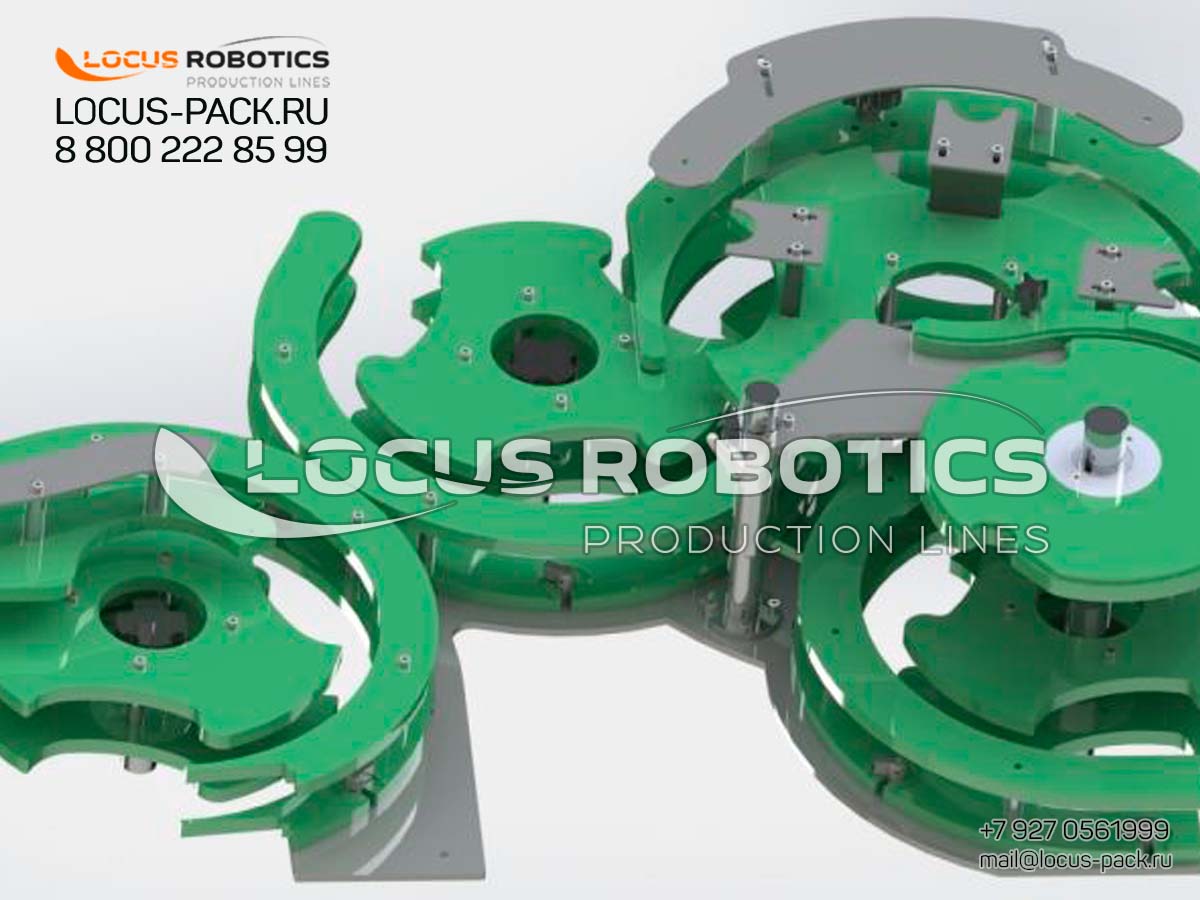
RC-100 High-Speed Rotary Monoblock for chemical products, protective guarding, plate conveyor, and rotary filling stations handling plastic jerry cans.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
Ready to Eliminate Production Bottlenecks?
Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🌡️ For a free product compatibility test using your materials.
Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.