Description
Precision Dosing for Ready-to-Drink Coffee and Dairy-Based Beverages
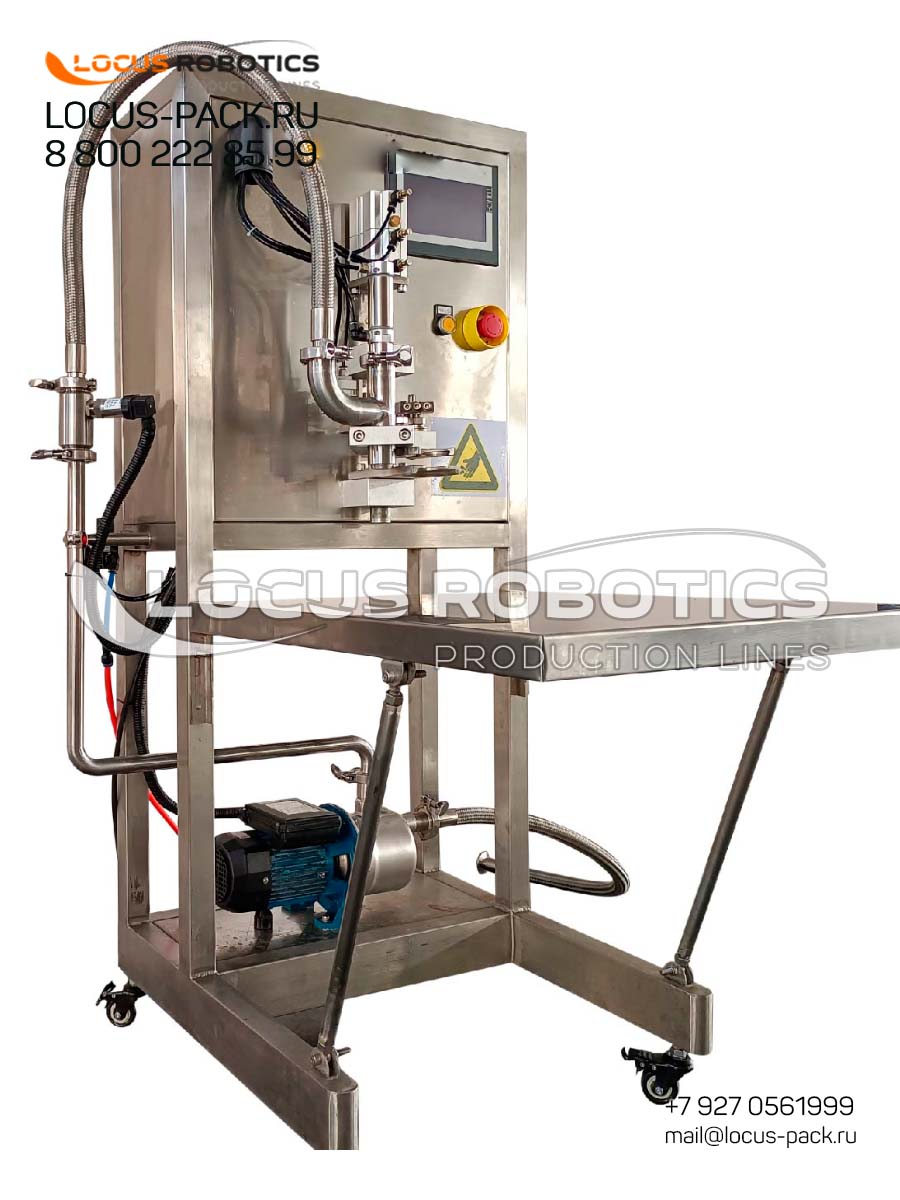
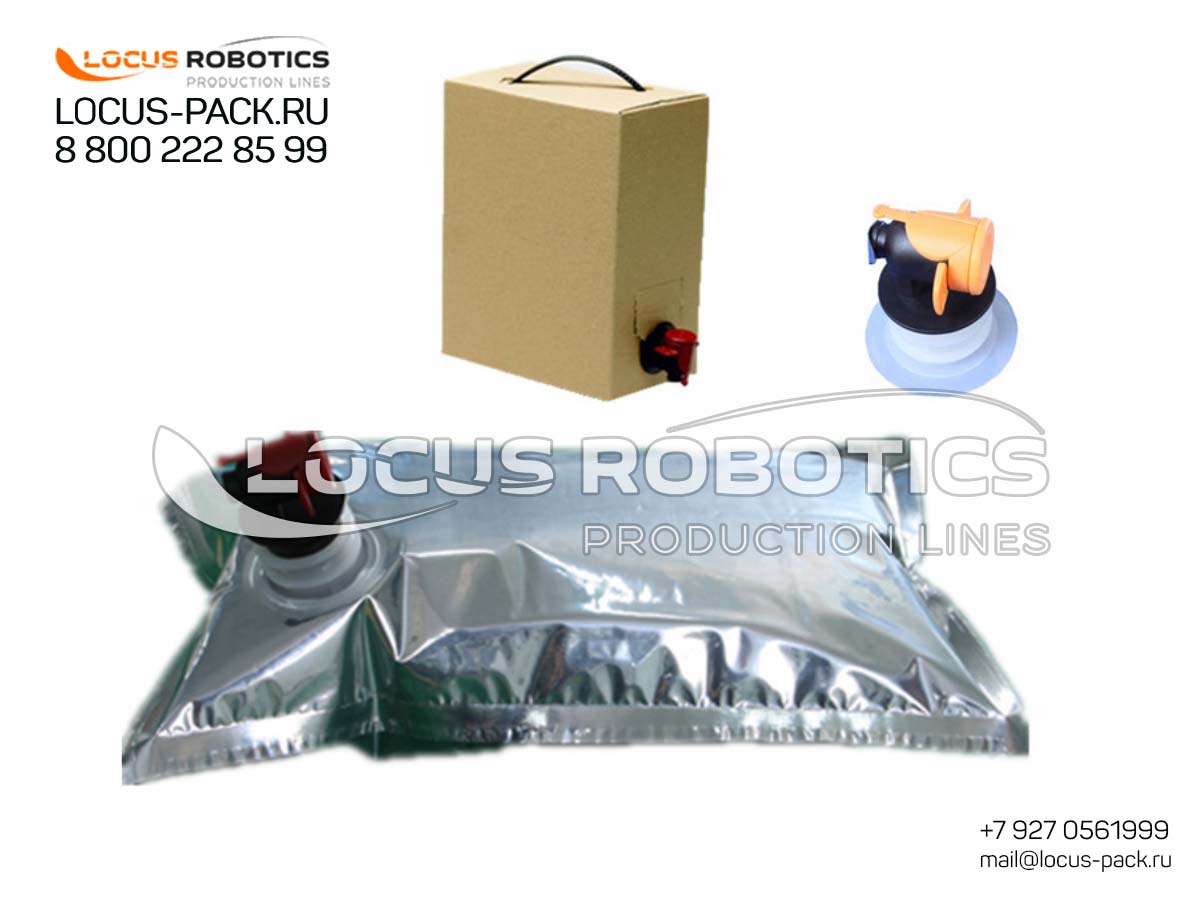
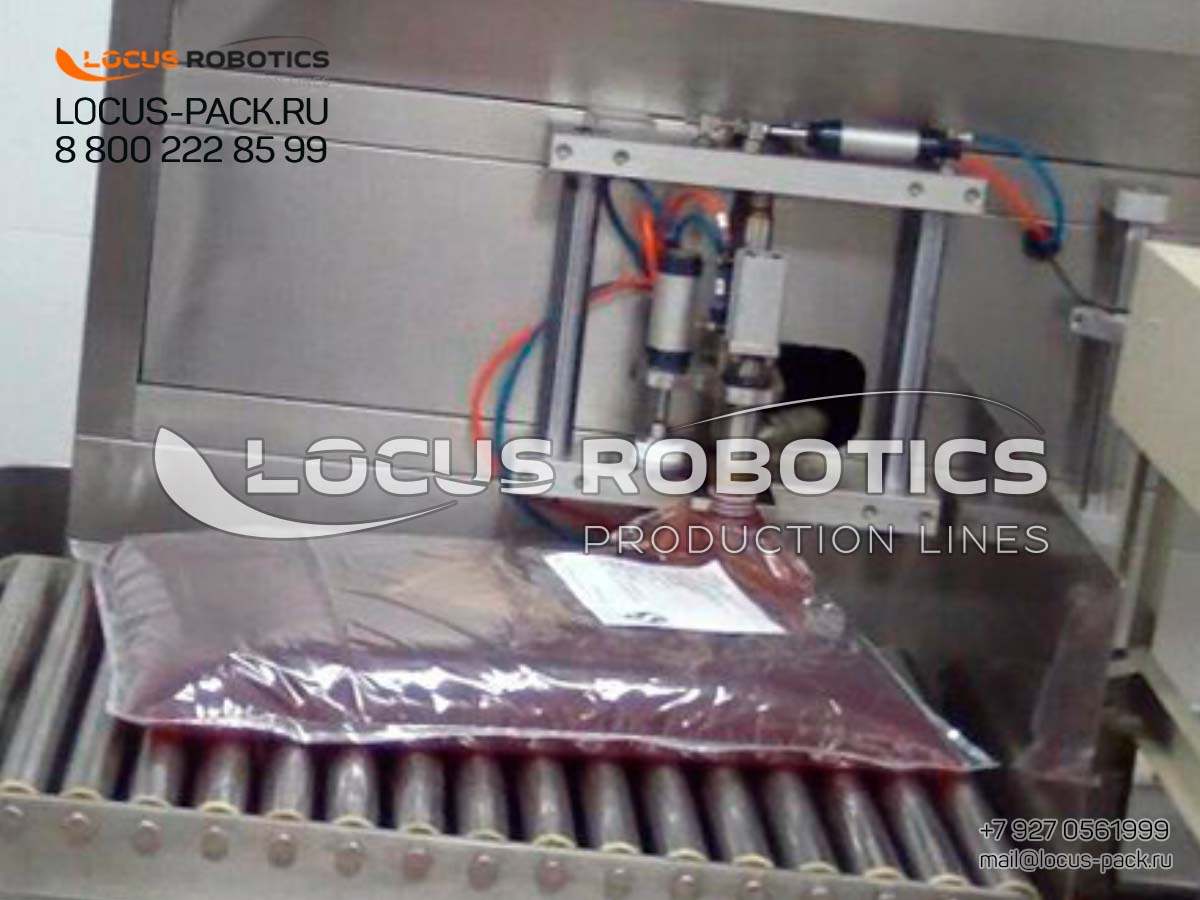
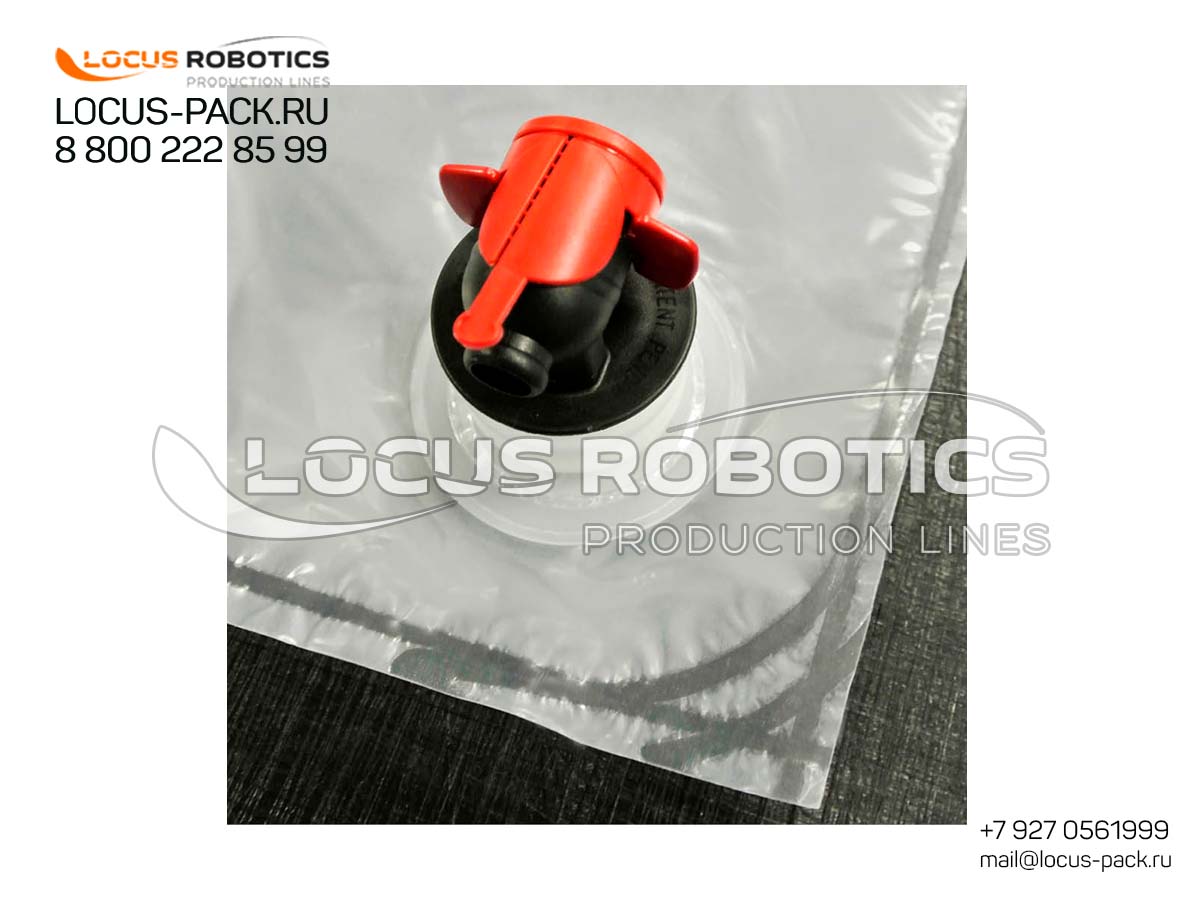
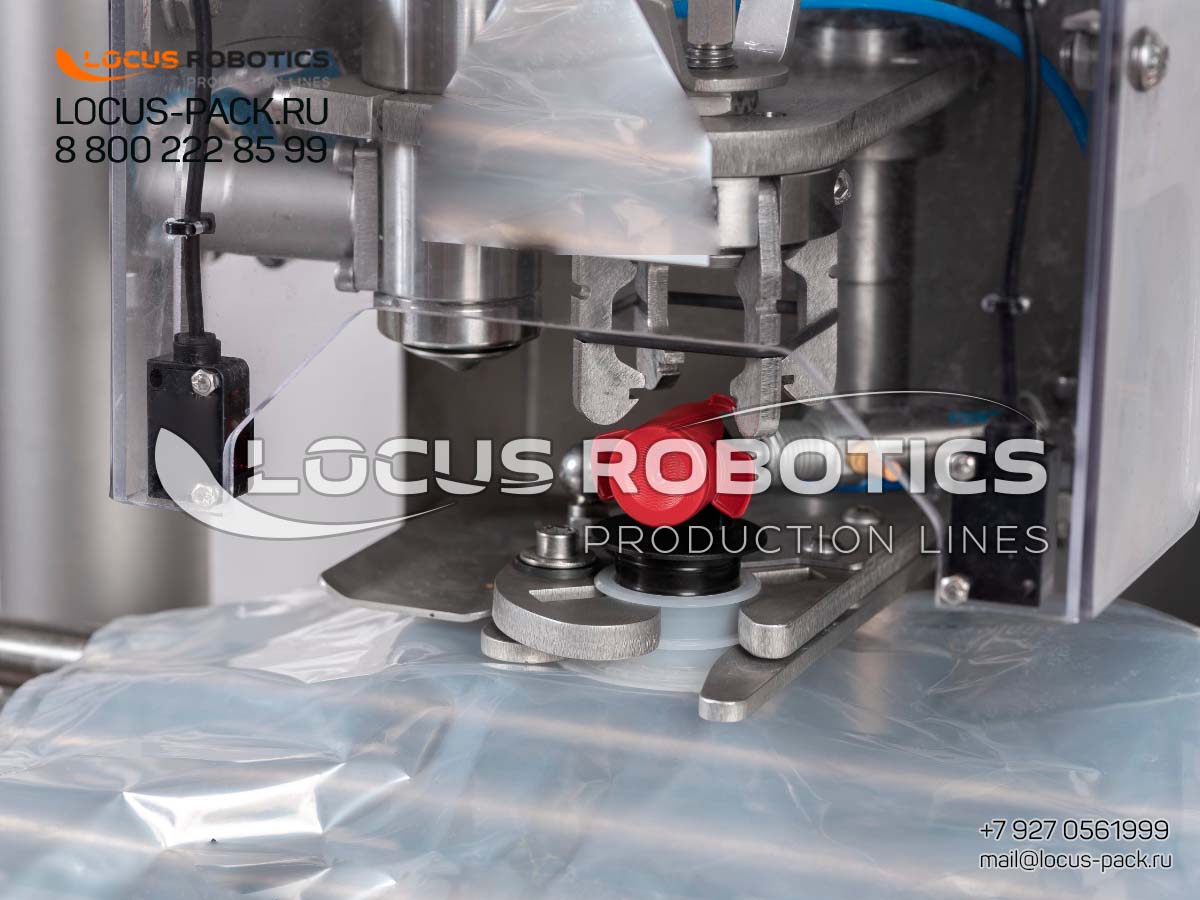
Automatic Dosing System for Coffee Beverages in Bag-in-Box with Transfer Pump: LFBB-100.
The LFBB-100 Automatic Dosing System addresses the unique challenges of packaging modern coffee beverages. This system is perfect for contract packagers and beverage companies producing cold brew coffee, canned latte equivalents, coffee concentrates, and milk-based coffee drinks for retail and food service. Its gentle pumping action and hygienic flow path are designed to protect the quality and shelf-life of sensitive products, making it a reliable solution for brands in Southeast Asia, the Middle East, and Latin America looking to capitalize on the growing ready-to-drink coffee market .
Technical Specifications & Performance Data
| Specification Category | Details / Placeholders |
|---|---|
| Model | LFBB-100 |
| Operation Type | Automatic/Semi-Automatic |
| Dosing Volume Range | 1 to 25 Liters |
| Dosing Accuracy | ±0.5% — ±1.0% |
| Production Capacity | Bags per Hour |
| Transfer Pump Type | Sanitary Centrifugal, Positive Displacement |
| Power Requirements | 220V / 380V |
| Control System | Touchscreen HMI & PLC |
| Materials in Contact | AISI 304 or 316L Stainless Steel, Food-Grade Plastics |
Key Features & Benefits for Coffee Beverage Production
-
Gentle Transfer Pump: The system utilizes a sanitary pump designed to handle products with varying viscosities and particulates, such as those found in oat milk lattes or coffee with cocoa particles, without damaging the product or compromising fill accuracy .
-
Hygienic & Compliant Design: All product contact surfaces are made from food-grade AISI 304 or 316L stainless steel, ensuring easy cleaning and compliance with international food safety standards. The design supports CIP (Clean-in-Place) processes, which are crucial for dairy-based coffee beverages to prevent bacterial growth .
-
User-Friendly Control & Flexibility: An intuitive Human-Machine Interface (HMI) allows for easy operation and quick changeovers between different bag sizes and coffee products. This flexibility is key for producers who package multiple SKUs.
Industries & Applications
-
Coffee Roasters & Beverage Companies: Perfect for cold brew coffee producers, ready-to-drink (RTD) latte brands, and coffee concentrate manufacturers. The system allows them to move into bag-in-box formats for keg-free distribution to cafes or larger-volume retail packs.
-
Contract Packagers (Co-packers): Offers a reliable and efficient solution for businesses that package beverages for multiple brands, requiring quick changeover and validated cleaning processes for different coffee and dairy products.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.