Description
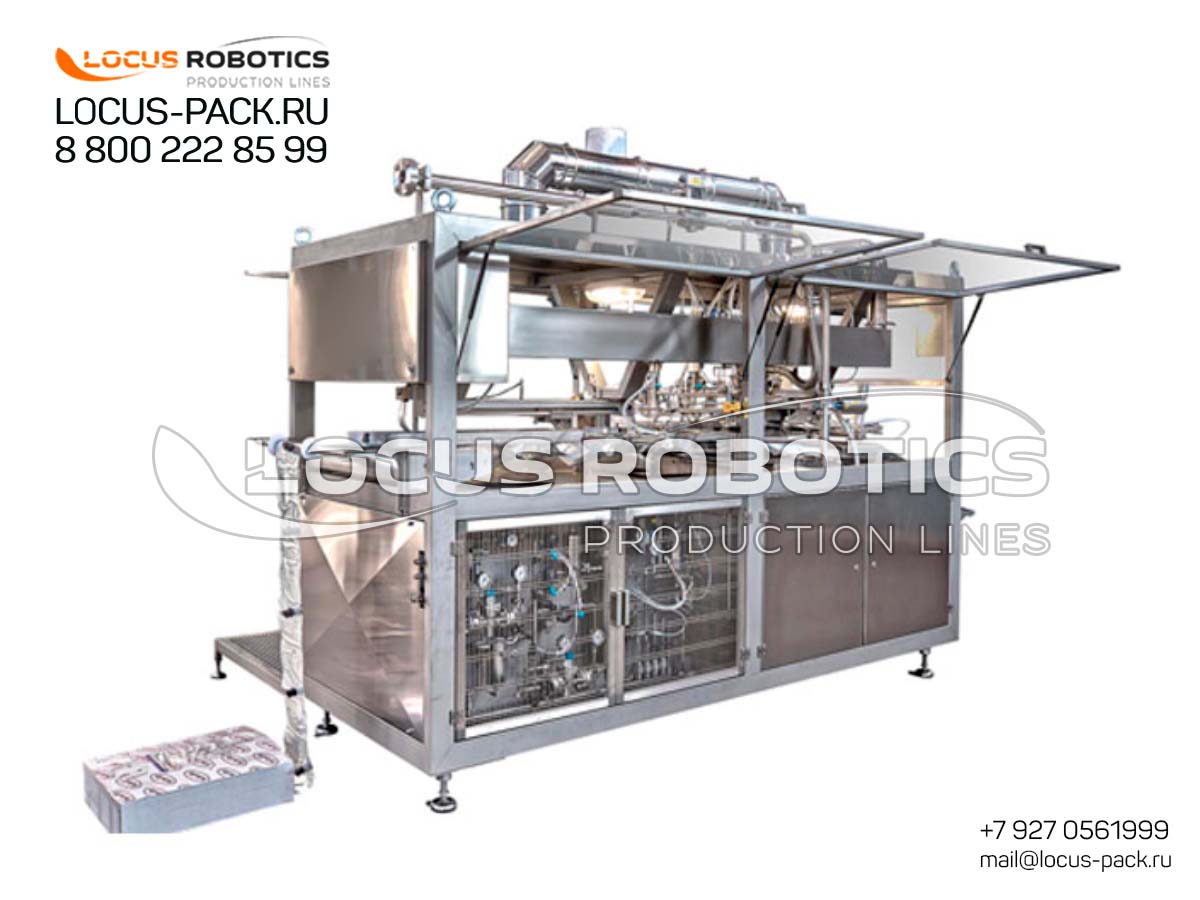
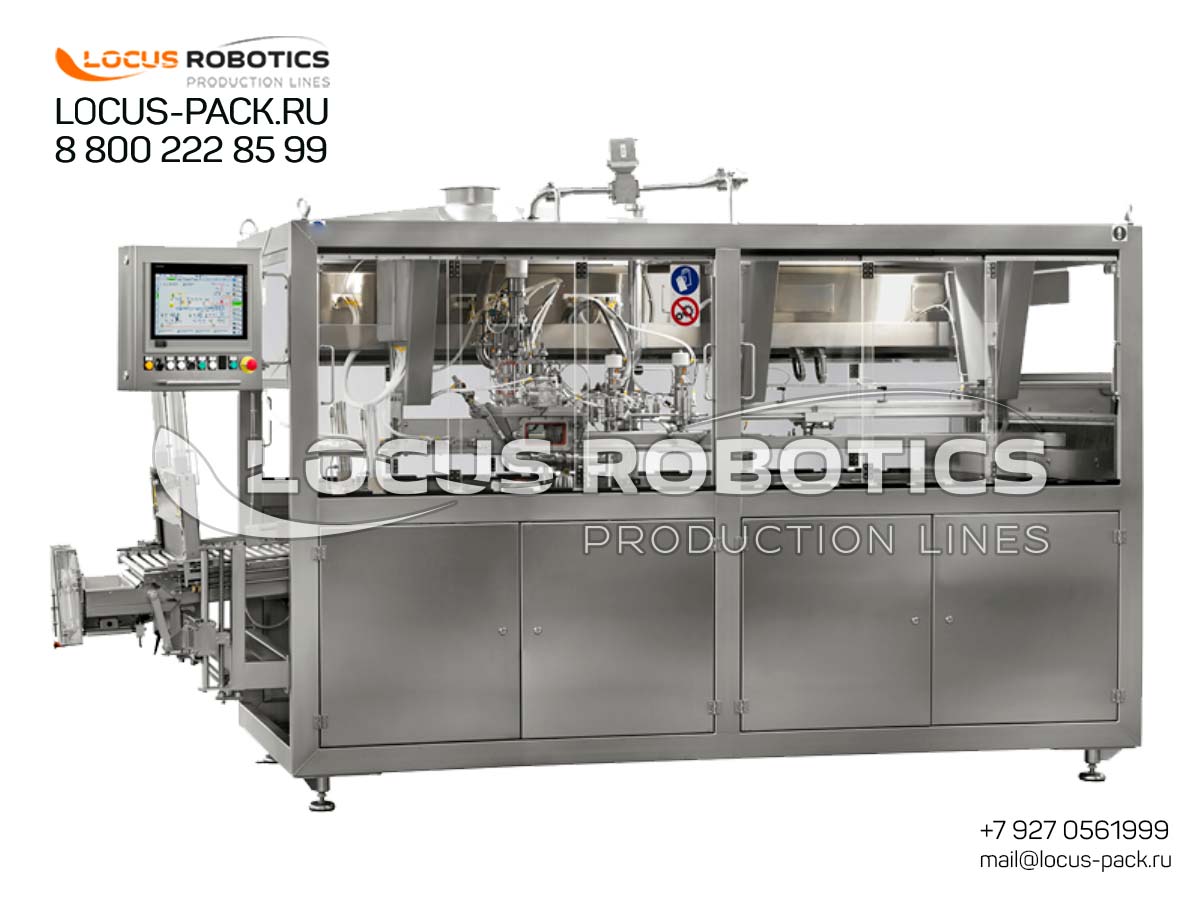
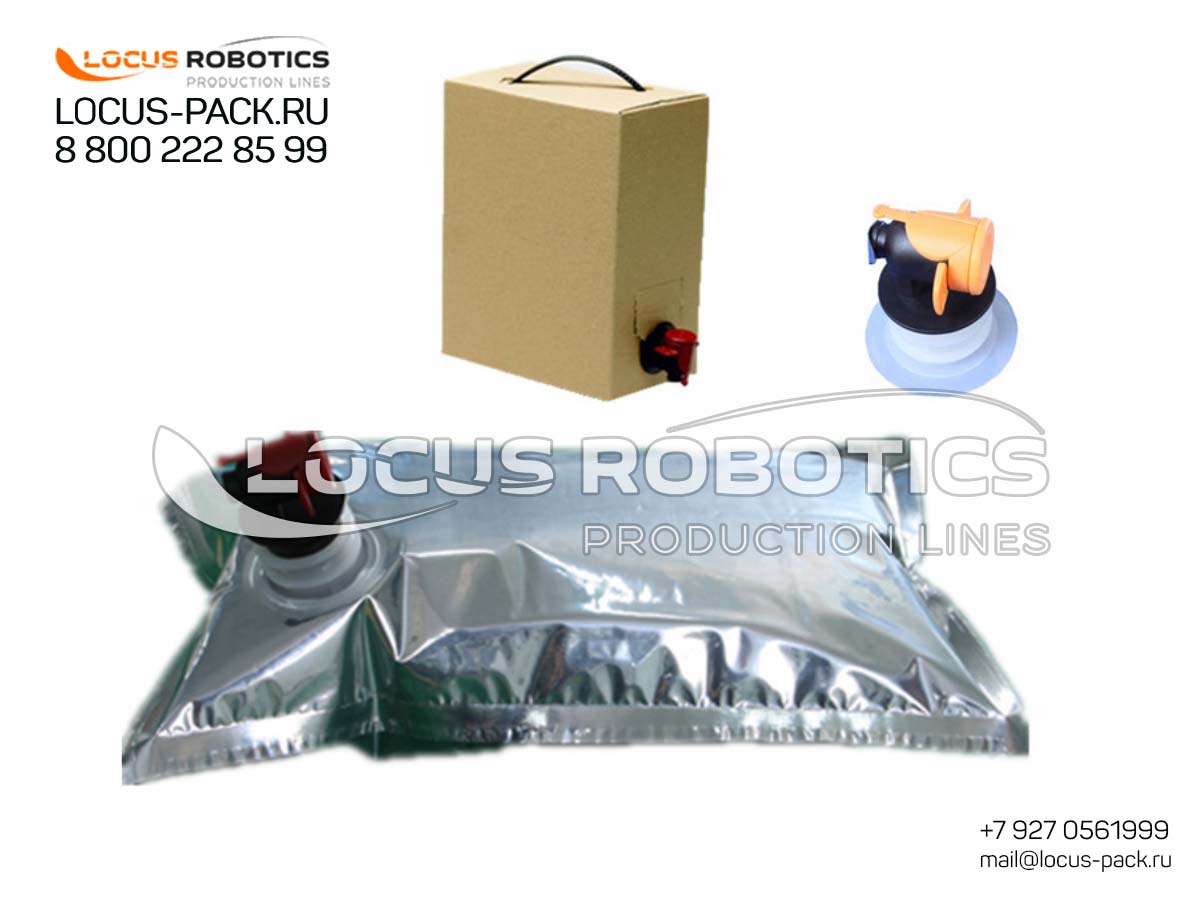
Automatic Single-Line Monoblock for Hot-Fill Juice Packaging in Bag-in-Box: LFBB-1000 Series
Advanced Hot-Fill Technology for Shelf-Stable Beverage Packaging
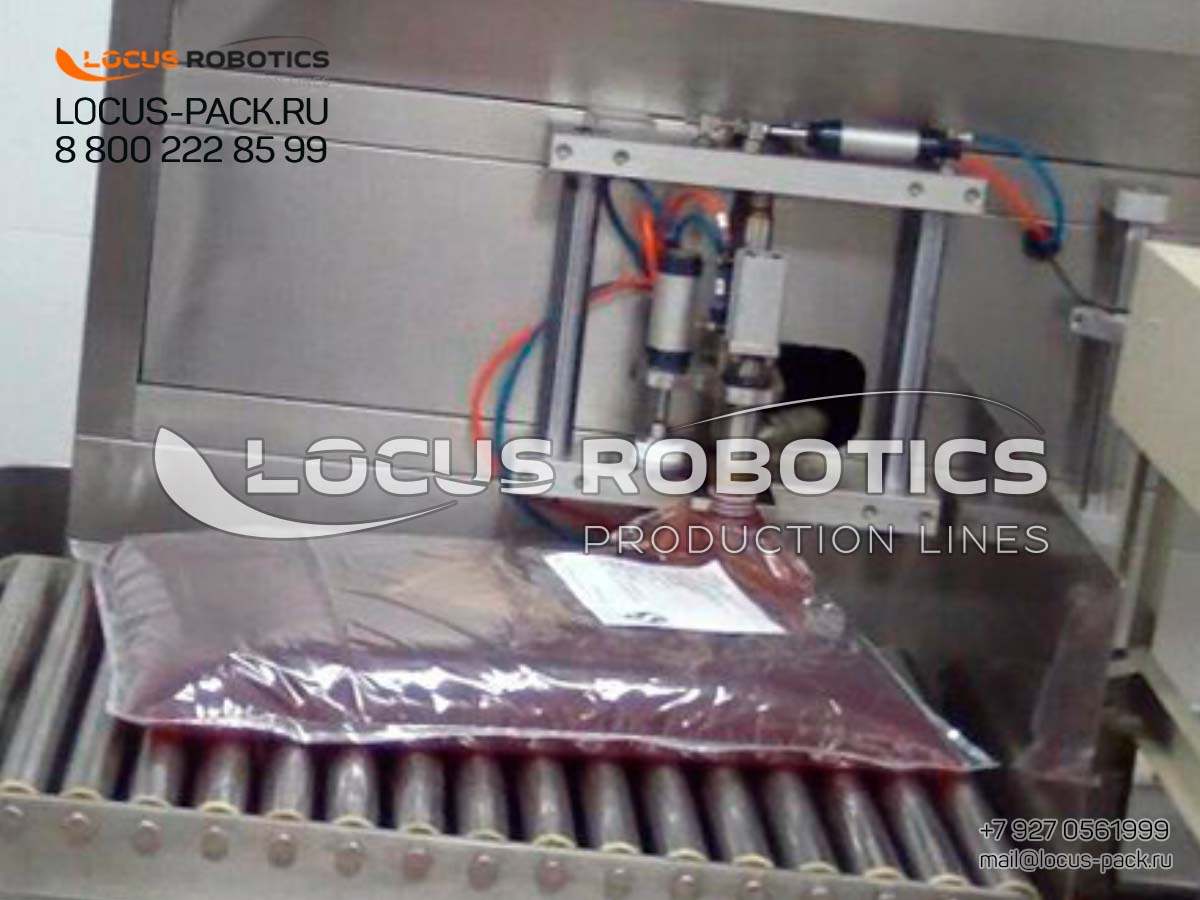
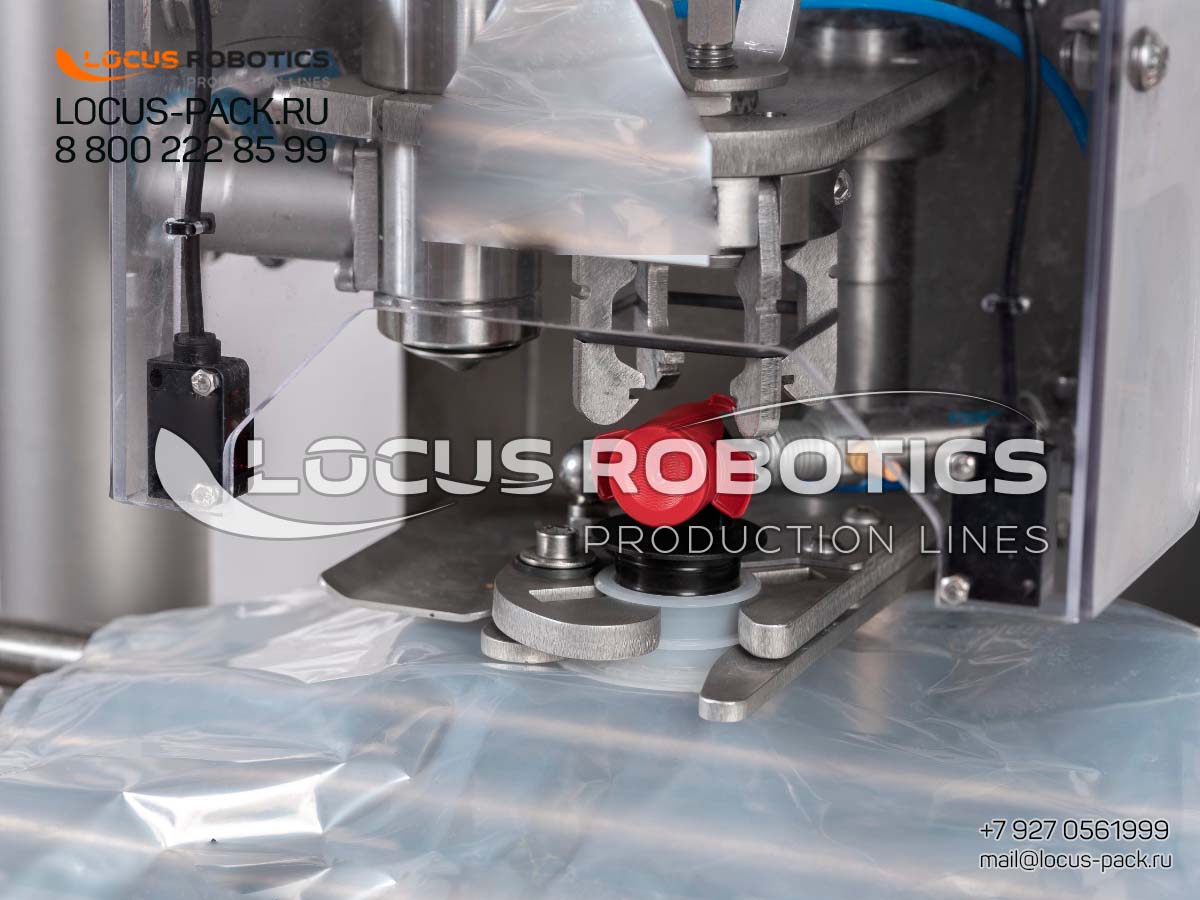
The LFBB-1000 Automatic Single-Line Monoblock represents the pinnacle of beverage packaging technology for hot-fill applications. This specialized system integrates bag feeding, high-temperature filling, and hermetic sealing in one compact, hygienic unit. By maintaining precise temperature control throughout the packaging process, it destroys microorganisms and ensures product stability at ambient temperatures—critical for markets in Southeast Asia, Africa, and Latin America where refrigeration infrastructure may be limited.
Technical Specifications & Performance Data
| Specification Category | Technical Details |
|---|---|
| Model | LFBB-1000 Series |
| Process Type | Hot-Fill/Aseptic |
| Filling Temperature Range | 85°C — 95°C (185°F — 203°F) |
| Production Capacity | Up to 1,200 bags per hour |
| Bag Size Range | 1L, 2L, 3L, 5L |
| Filling Accuracy | ±0.5% |
| Temperature Control | ±1°C precision |
| Materials | AISI 316L Stainless Steel (product contact) |
| Sterilization Method | Steam or chemical sterilization (CIP/SIP available) |
Key Features & Beverage Industry Benefits
-
Precision Hot-Fill System: Advanced heat exchangers and holding tubes maintain exact filling temperatures, ensuring proper pasteurization and product quality preservation for acidic fruit juices and sensitive beverages.
-
Aseptic Bag Environment: Integrated H₂O₂ vapor or steam sterilization creates a sterile packaging environment, preventing post-fill contamination and enabling ambient temperature distribution.
-
Juice-Optimized Components: Specialized food-grade pumps and valves handle particulate-containing juices, fruit pulps, and viscous nectars without damage or separation.
-
Quality Assurance Systems: Optional inline Brix monitoring, metal detection, and checkweighers ensure consistent product quality and compliance with international food safety standards.
Industries & Beverage Applications
-
Juice & Fruit Processing: Ideal for orange juice, apple juice, tropical blends, and fruit concentrates. Maintains vitamin content and fresh taste through controlled hot-fill process.
-
Dairy Alternatives: Perfect for soy milk, almond milk, and oat milk beverages requiring extended shelf life without refrigeration.
-
Functional Beverages: Handles vitamin-fortified drinks, sports beverages, and health tonics with precise temperature control for sensitive ingredients.
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
🔍Ready to Eliminate Production Bottlenecks?
💎Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
📈Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🧼Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.