Description
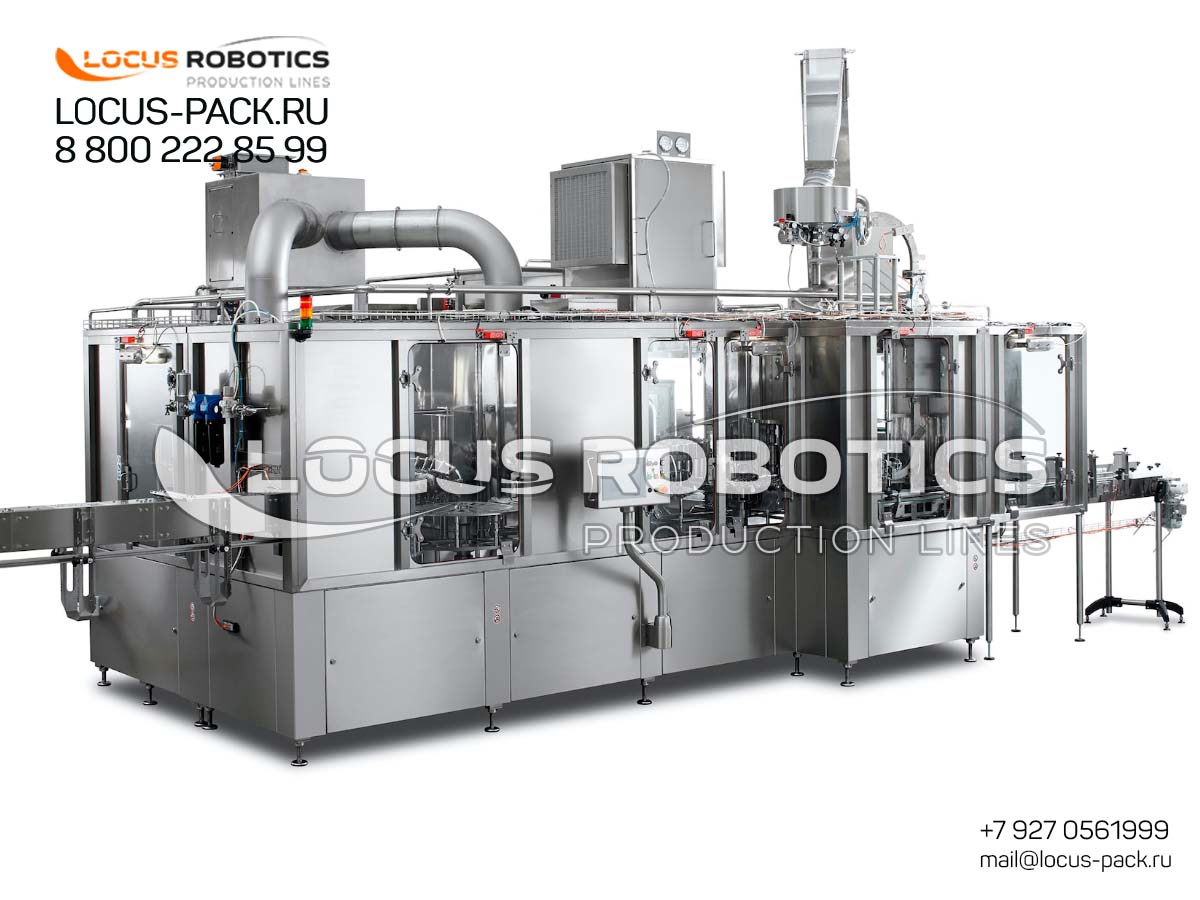
RC-100 Integrated Hot-Fill Monoblock showing the process from PET preform to a filled and capped bottle of sauce on a single machine
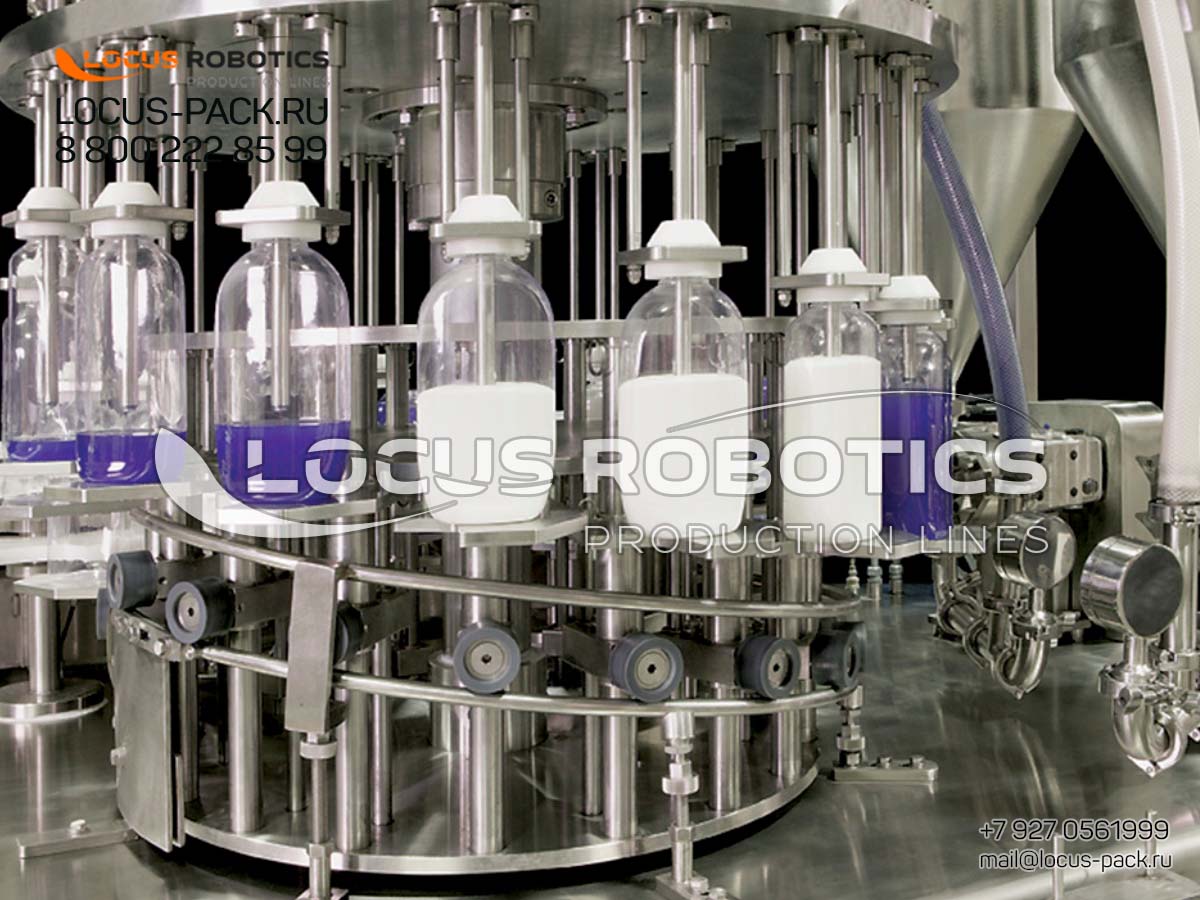
High-Speed Rotary Rinsing-Filling-Capping Monoblock for Hazardous and Hot Liquids.
Complete In-Line Solution for Shelf-Stable Hot-Fill Products.
Integrated Process: Blow Molding, Hot-Filling, and Capping in One System.
Ideal for High-Acid Foods, Sauces, and Syrups.
How Hot-Filling Technology Ensures Preservation and Shelf Life.
All-In-One Innovation: Integrates blow molding, hot-filling, and capping into a single, hygienic platform.
Shelf-Stable Preservation: Hot-fill process (85°C — 95°C) ensures microbial stability and extends shelf life naturally.
Perfect for Viscous Products: Handles sauces, jams, syrups, honey, and dairy products with suspended pieces.
Maximized Hygiene: Closed-loop system from preform to sealed bottle drastically reduces contamination points.
Complete In-Line Solution for Shelf-Stable Hot-Fill Products
The RC-100 represents the pinnacle of integrated packaging technology for the food industry. It is specifically designed for products that rely on the hot-fill process for preservation. This machine transforms standard PET preforms into custom-shaped bottles, immediately fills them with product at high temperatures, and hermetically seals them—all within a single, controlled environment. This end-to-end solution is ideal for manufacturers looking to enhance product safety, reduce their factory footprint, and streamline their production process for high-acid and viscous foods.
Integrated Process: Blow Molding, Hot-Filling, and Capping in One System
-
Station 1: Stretch-Blow Molding: PET preforms are loaded, heated, and then blow-molded into the desired bottle shape directly on the machine. This allows for custom container design and eliminates pre-bottle storage and handling.
-
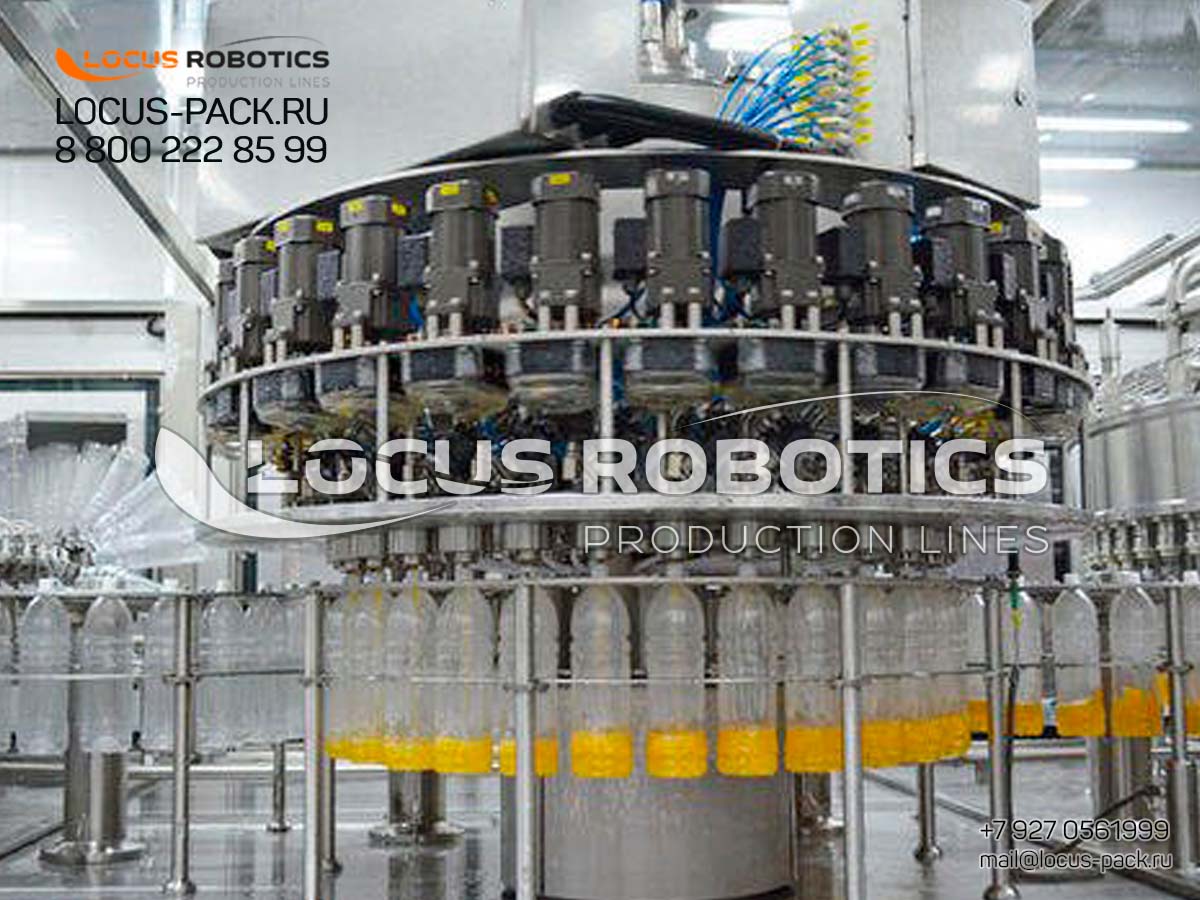
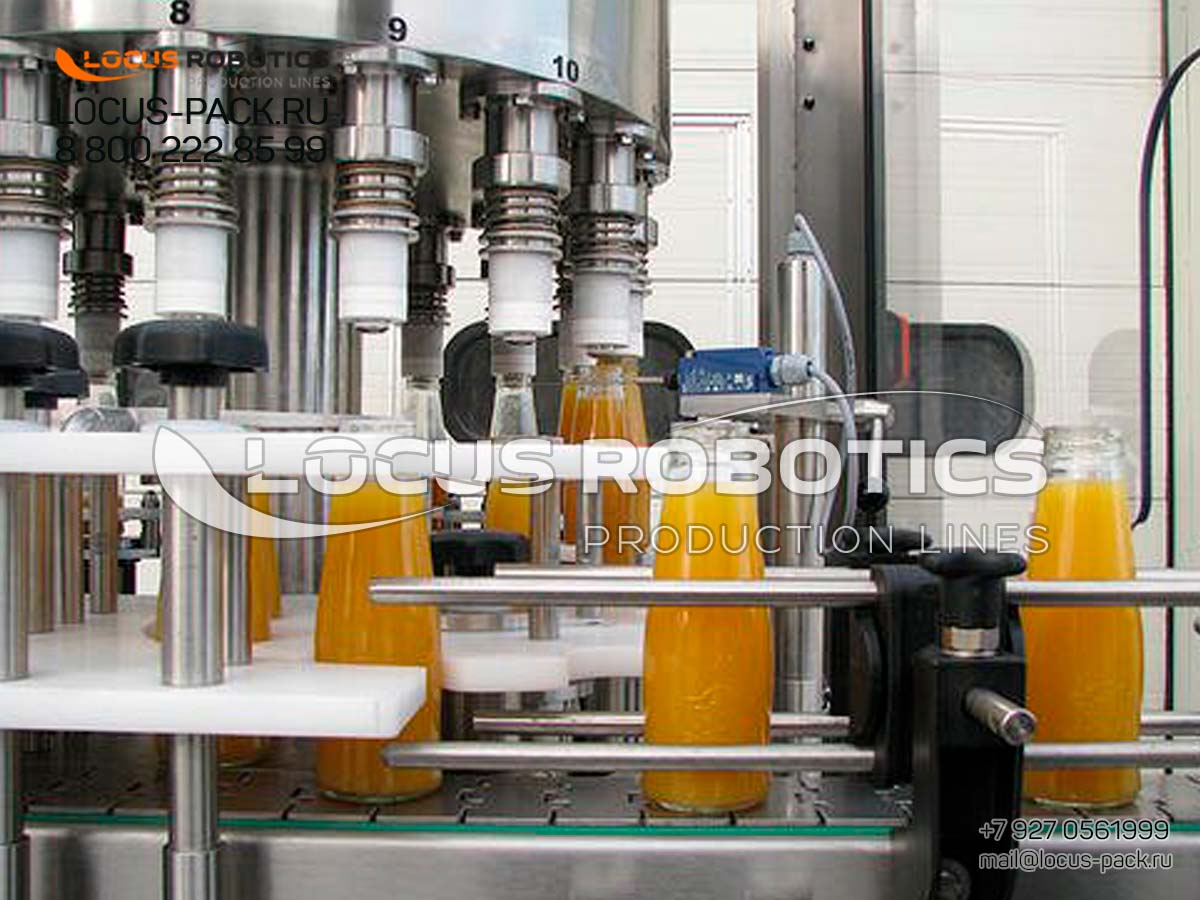
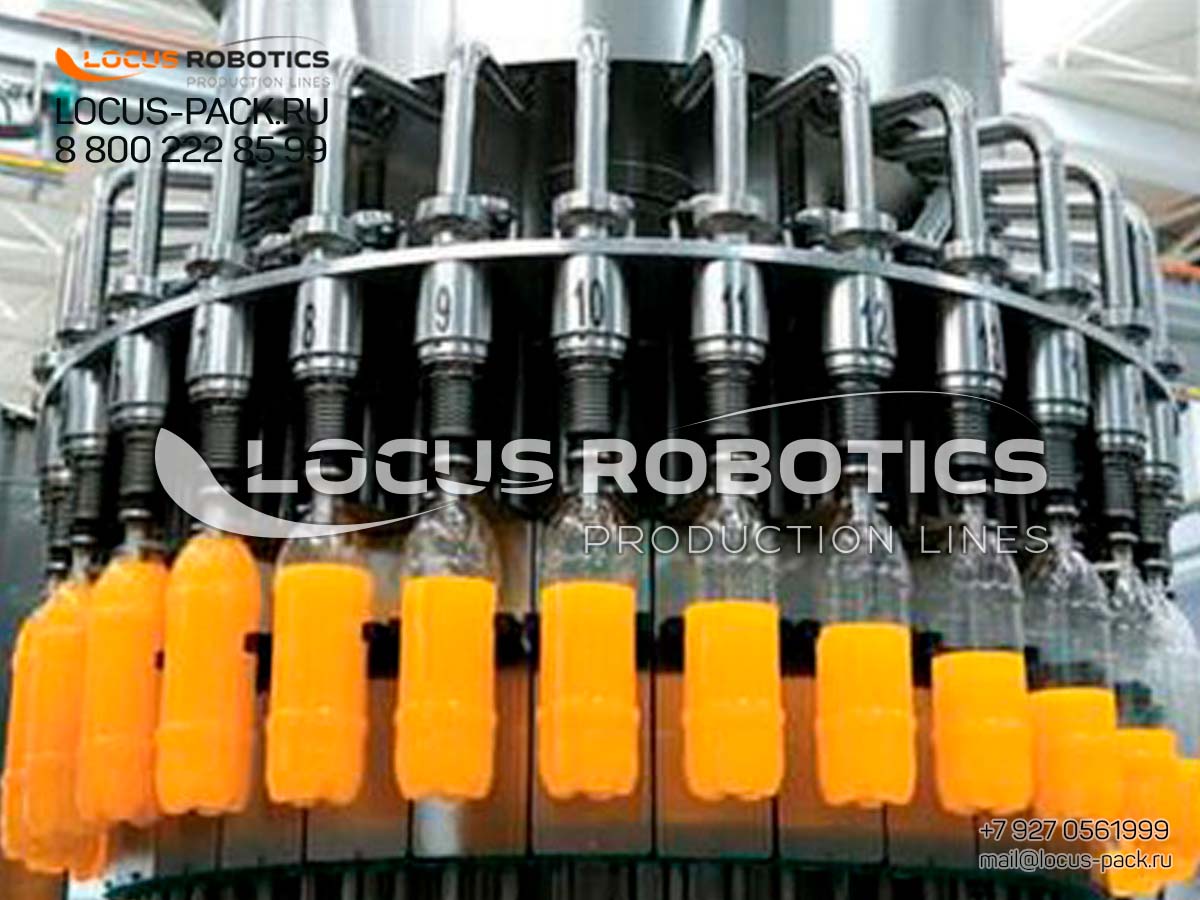
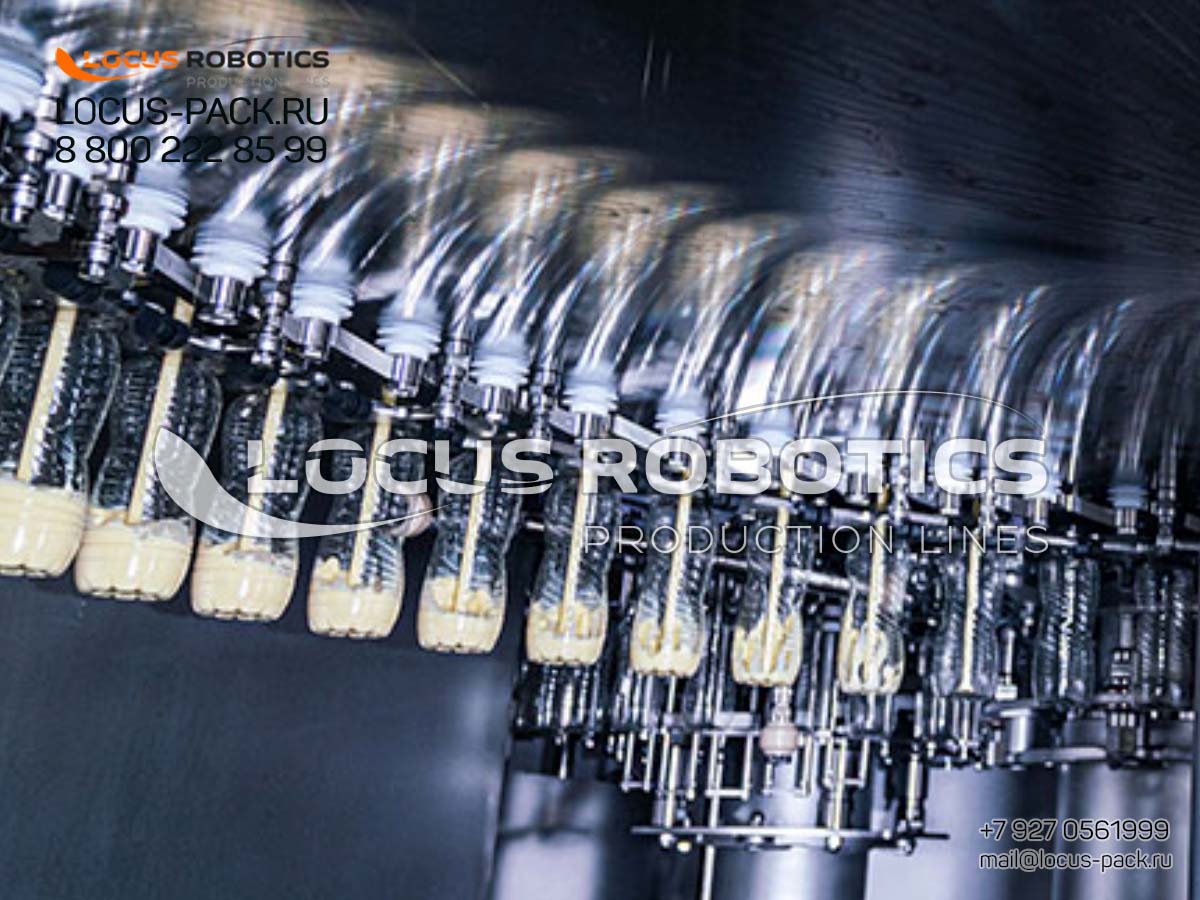
Station 2: Hot-Filling: The newly formed bottles are immediately filled with the product, typically at temperatures between 85°C and 95°C (185°F — 203°F). This temperature pasteurizes the product and the container interior.
-
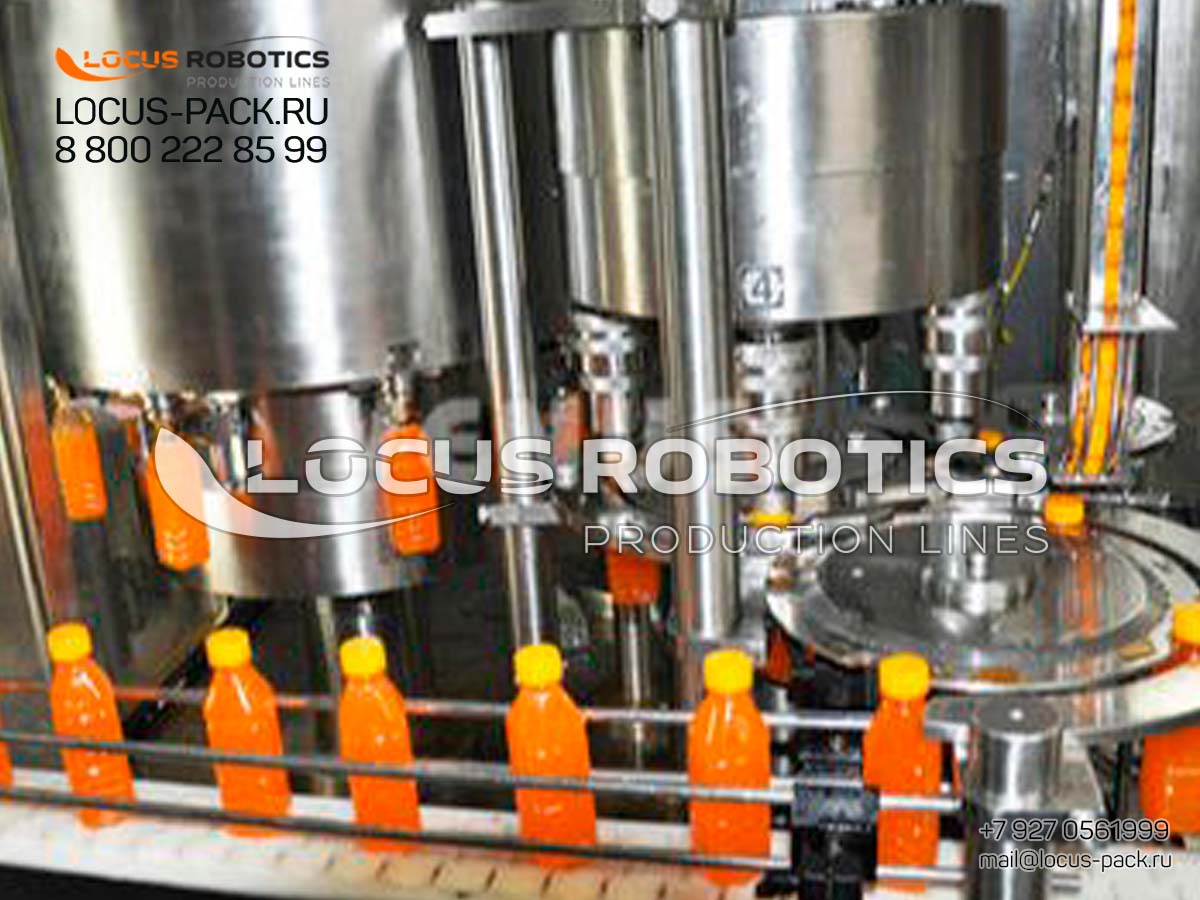
Station 3: Hermetic Capping: The filled bottles are sealed with a tamper-evident cap while the product is still hot. As the bottle and its contents cool, a vacuum forms inside, pulling the cap down securely and ensuring the seal is airtight. This vacuum is the key to the product’s shelf stability.
Technical Specifications & Performance Data
-
Model: RC-100
-
Type: Integrated Automated Monoblock
-
Functions: Stretch-Blow Molding, Hot-Filling, Capping
-
Filling Temperature: Up to 95°C (203°F)
-
Container Sizes: From 100ml to 1000ml (customizable based on mold)
-
Output: Up to 3,000 bottles per hour (dependent on bottle size)
-
Filling System: Piston filler for viscous products
-
Filling Accuracy: ≤ ±1.0%
-
-
Capping System: Rotary chuck capper with torque control
-
Blow Molding: Integrated single-stage stretch-blow molding unit
-
Power Supply: 380V/50Hz/3Ph (standard, configurable)
-
Construction Material: 304 & 316L Stainless Steel for all product contact parts
-
Control System: Advanced PLC with Touchscreen HMI for full process control and data logging
Ideal for High-Acid Foods, Sauces, and Syrups
-
Fruit Products: Jams, jellies, fruit pieces in syrup, pie fillings.
-
Sauces & Condiments: Ketchup, mayonnaise, mustard, pasta sauce, salsa.
-
Dairy & Desserts: Yogurt, pudding, dairy-based sauces.
-
Other: Honey, syrups, baby food, liquid eggs.
How Hot-Filling Technology Ensures Preservation and Shelf Life
The hot-fill process is a natural method of preservation. By filling the product at near-pasteurization temperatures, it destroys spoilage microorganisms and deactivates enzymes. The subsequent vacuum formation during cooling removes oxygen from the headspace, further inhibiting the growth of aerobic bacteria and yeasts. This allows products to achieve a long shelf life at ambient temperatures without refrigeration, which is crucial for distribution in regions with varying infrastructure.
Key Features Description:
This advanced rotary monoblock integrates comprehensive processing capabilities for handling challenging substances, including hot food products and aggressive hazardous materials. The system features a rotary bottle rinsing module, precision rotary dosing system, rotary capping mechanism, protective guarding, integrated fume extraction, disc-type (orbital) cap orienter with elevator feed system, and advanced filtration technology.
Specifically engineered for demanding industrial applications, this system safely handles pesticides, agrochemicals, and substances with toxic vapors, packaged in either glass or plastic containers. The complete enclosure and filtration system ensures operator safety and environmental compliance during production.
Technical Specifications:
-
Processing Capabilities:
-
Hot food products (85-95°C)
-
Aggressive chemicals and solvents
-
Toxic substances and pesticides
-
Products with hazardous vapors
-
-
Container Compatibility: Glass and plastic containers
-
Key Components:
-
Rotary bottle rinsing module
-
Precision rotary dosing system
-
Rotary capping mechanism
-
Full protective guarding
-
Integrated fume extraction system
-
Disc-type (orbital) cap orienter
-
Elevator feed system
-
Advanced filtration system
-
-
Safety Features:
-
Explosion-proof options available
-
Chemical-resistant materials
-
Vapor containment system
-
Emergency stop systems
-
-
Compliance: Meets international safety standards for hazardous material handling
Technical Advantages:
-
Safety First: Complete enclosure with fume extraction and filtration protects operators and environment
-
Chemical Resistance: 316L stainless steel and specialized sealing materials withstand aggressive substances
-
Precision Dosing: Rotary filling system maintains ±0.5% accuracy even with viscous products
-
Temperature Control: Handles hot products (up to 95°C) without performance degradation
-
Flexible Packaging: Accommodates various container types and sizes with quick changeover
-
Regulatory Compliance: Designed to meet international standards for hazardous material handling
Applications:
-
Agricultural Chemicals: Pesticides, herbicides, insecticides
-
Industrial Chemicals: Solvents, acids, alkaline solutions
-
Pharmaceuticals: Toxic active ingredients, potent compounds
-
Food Industry: Hot-fill products, sauces, concentrates
-
Specialty Chemicals: Cleaning agents, disinfectants, specialty formulations
Safety & Compliance Features:
-
ATEX-certified components available for explosive environments
-
CIP/SIP systems for effective cleaning and sterilization
-
Double mechanical seals on all rotating components
-
Emergency shower and eye wash system compatibility
-
Full documentation for validation and regulatory compliance
-
Leak detection and containment systems
📜 Schedule virtual airflow visualization test.
💡 Mention your: Target market (EU/US/Global South), Active ingredient, Required throughput.
🔬 Schedule virtual factory acceptance test with our engineers.
🏷️ Request Compliance Audit: Free gap analysis with throughput simulation.
Ready to Eliminate Production Bottlenecks?
Need Industrial Production Automation?
✅ GMP Compliance Guarantee
✅ 24/7 Multilingual Support
✅ 24-month performance guarantee
✅ Local technicians in 18 countries
Start small, get a free production layout designed for your growth trajectory. Scale smarter with engineering support!
📥Free line configuration for your products, throughput validation testing!
🎓Contact Specialists for Packaging Equipment:
📄 On-Demand Engineering: Product-specific configurations in 1-2 weeks.
🔧 Spare Parts Kits: Region-specific inventory for <24hr delivery.
🌡️ For a free product compatibility test using your materials.
Compliance Roadmap:
- CE, EAC, ISO 9001 certifications.
- GMP-ready: 316L SS contact parts, CIP/SIP capabilities.
- ATEX options for chemical solvents.